Custom Sheet Metal
Fabrication
Sheet metal fabrication and metal stamping, from one prototype to 100,000+ units
WERIX Metal is a custom sheet metal fabrication and metal stamping manufacturer in Dongguan, China. One 3,000+ sqm source factory runs laser cutting, CNC bending, welding, in-house dies and assembly — 5,000+ clients in 30+ countries since 2015 — orders start from a single prototype.
- 24h
- Quote reply
- 3–7d
- Sample delivery
- 5,000+
- Clients
- 98%
- On-Time
- 11+
- Years of experience
- ISO 9001
- Quality Assurance
Sheet Metal Fabrication and Metal Stamping Under One Roof
Two capabilities, one factory, one purchase order. Your parts ship from the same floor that cut and formed them, with in-house tooling for both fabrication and stamping.
Sheet Metal
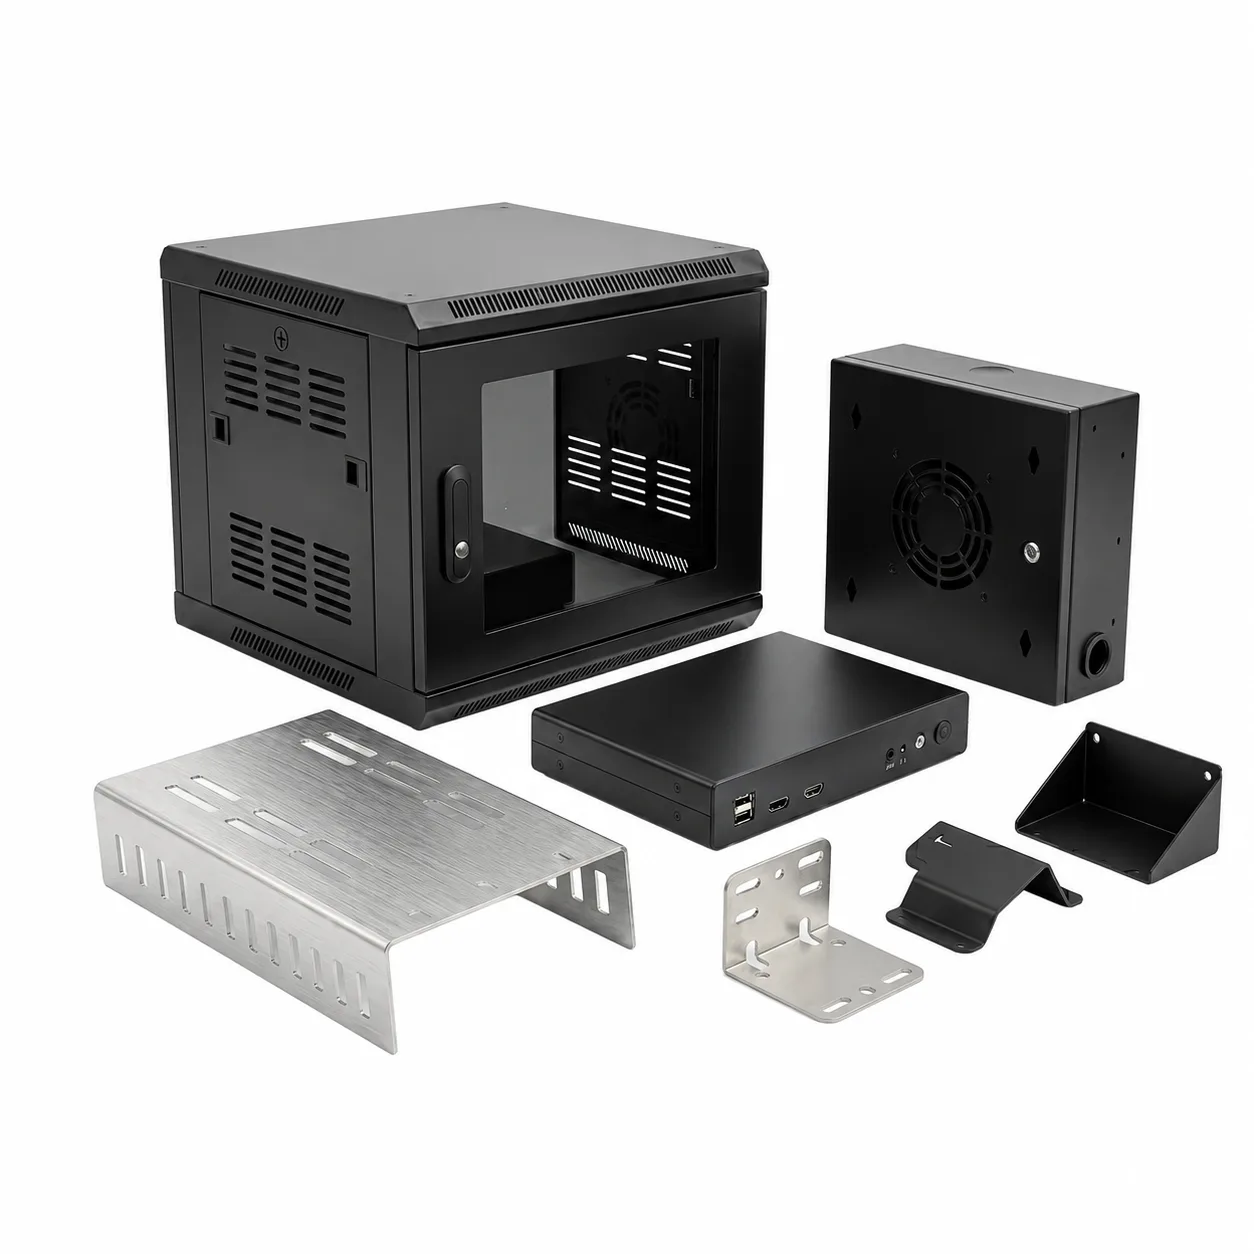
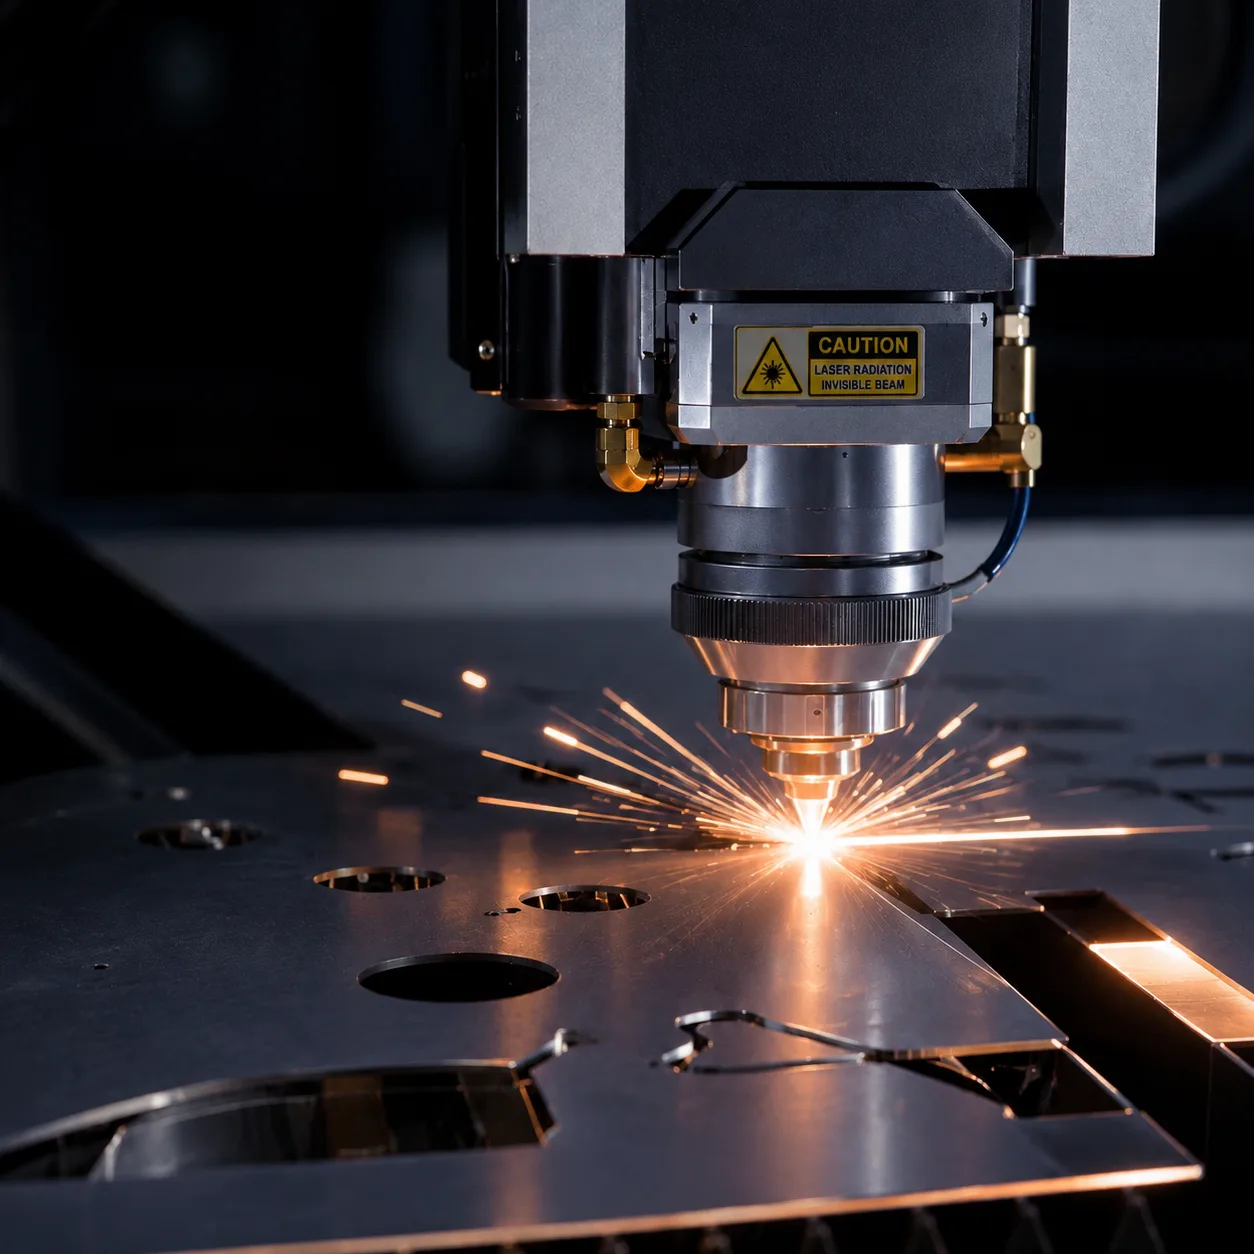
Custom sheet metal parts from 1 piece, prototypes in 3–7 days with no tooling cost. Fiber laser cutting, CNC press brake bending, TIG/MIG welding and assembly to ±0.1 mm, in sheet from 0.3 mm — laser cutting to 5.0 mm and press-brake forming to 6 mm.
Metal Stamping
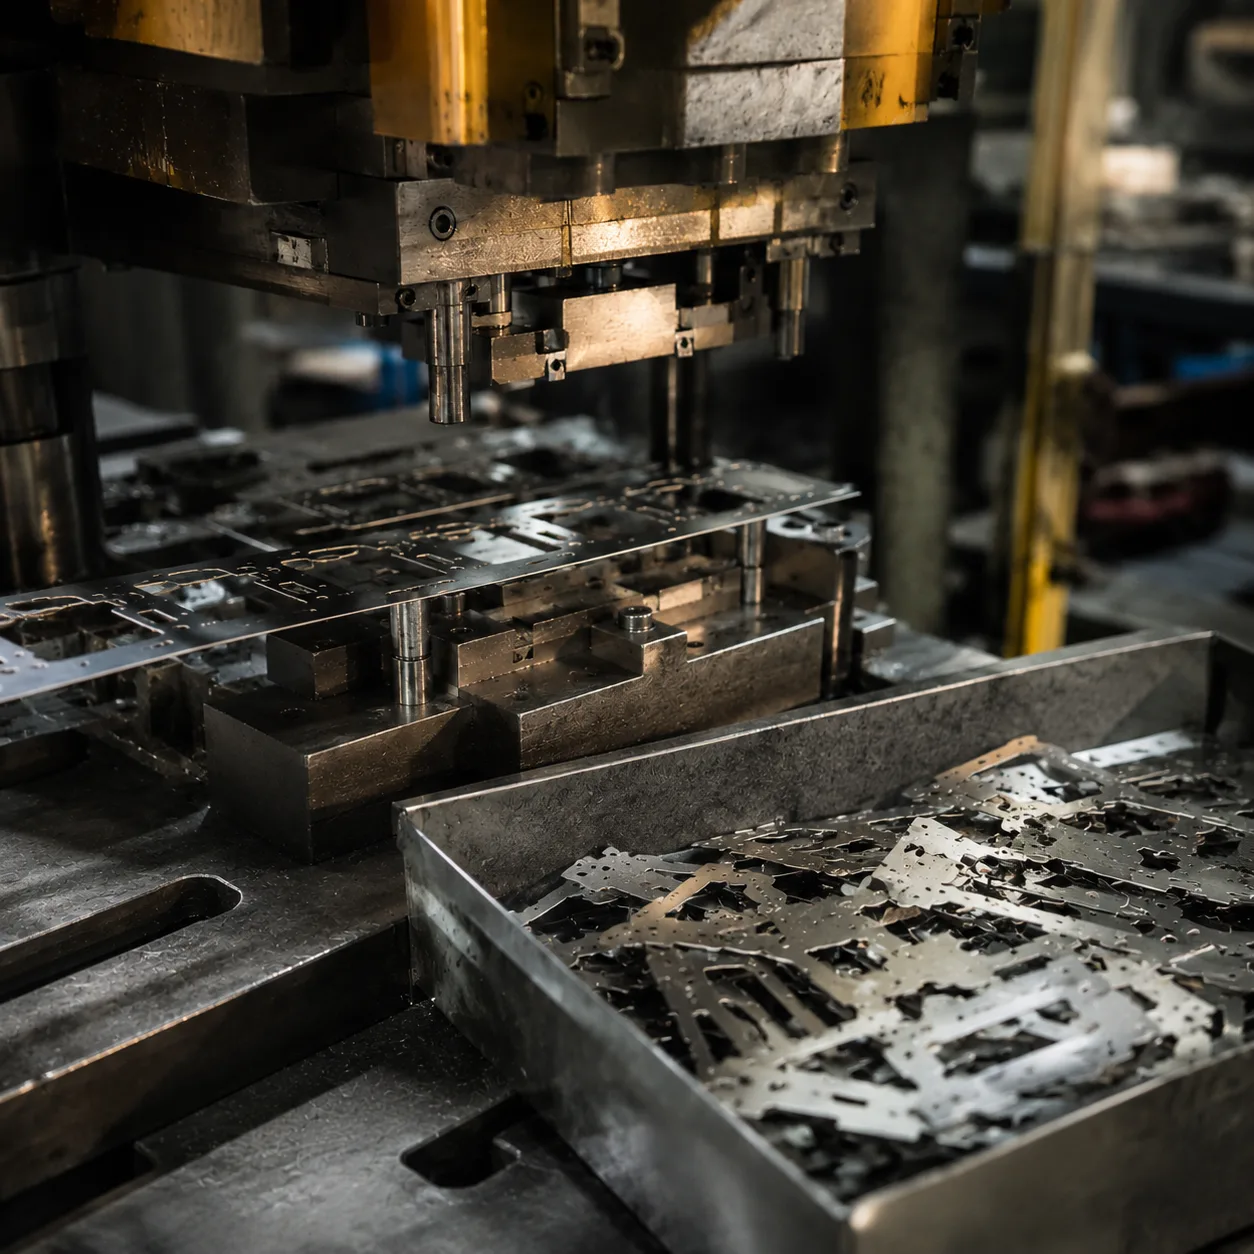
High-volume metal stamping on 25T to 300T press lines. Progressive, transfer and compound dies plus deep drawing, designed and built in our own die shop for a lower unit cost at scale.
Inside Our Factory
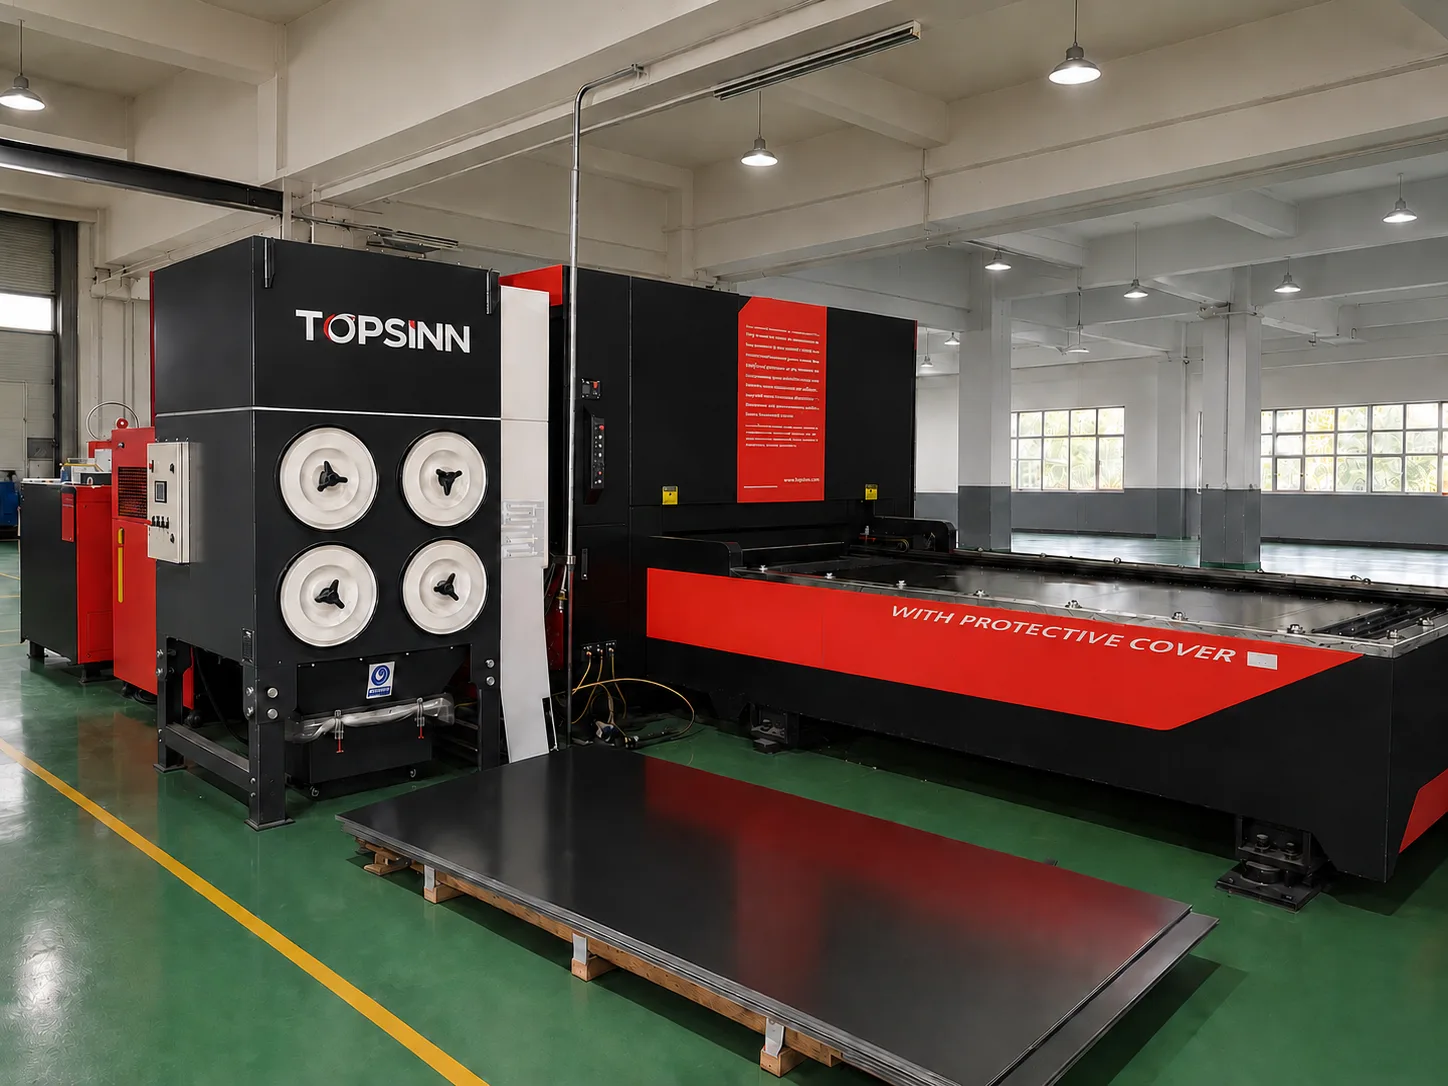
High Power Laser Machine
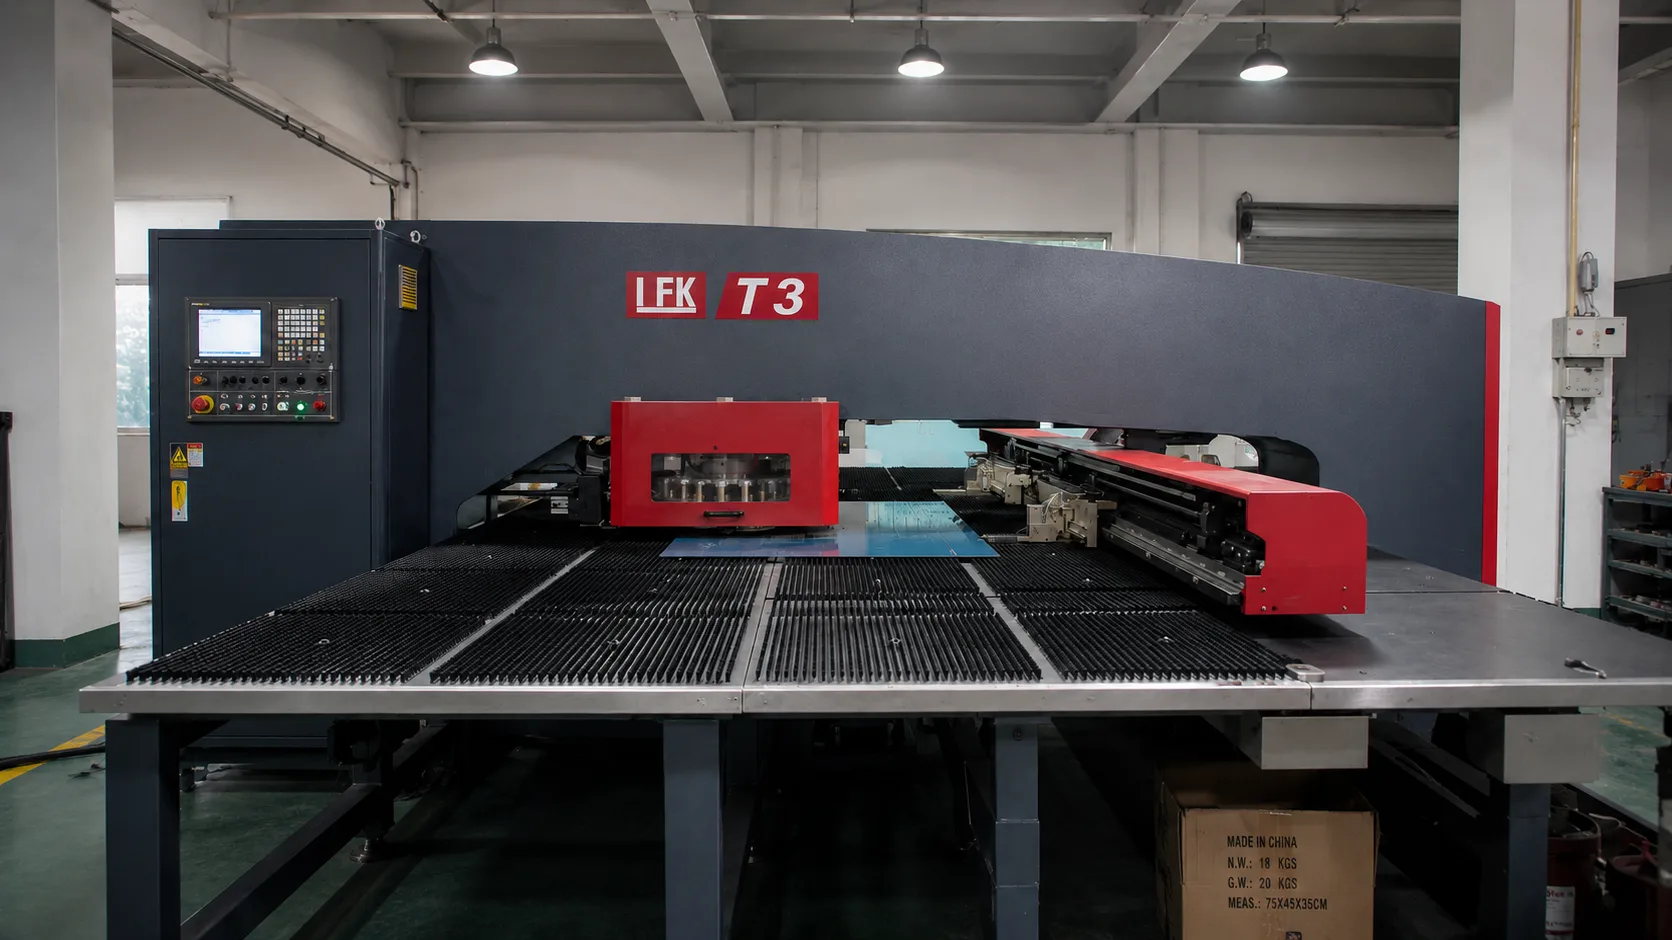
CNC Punching Center
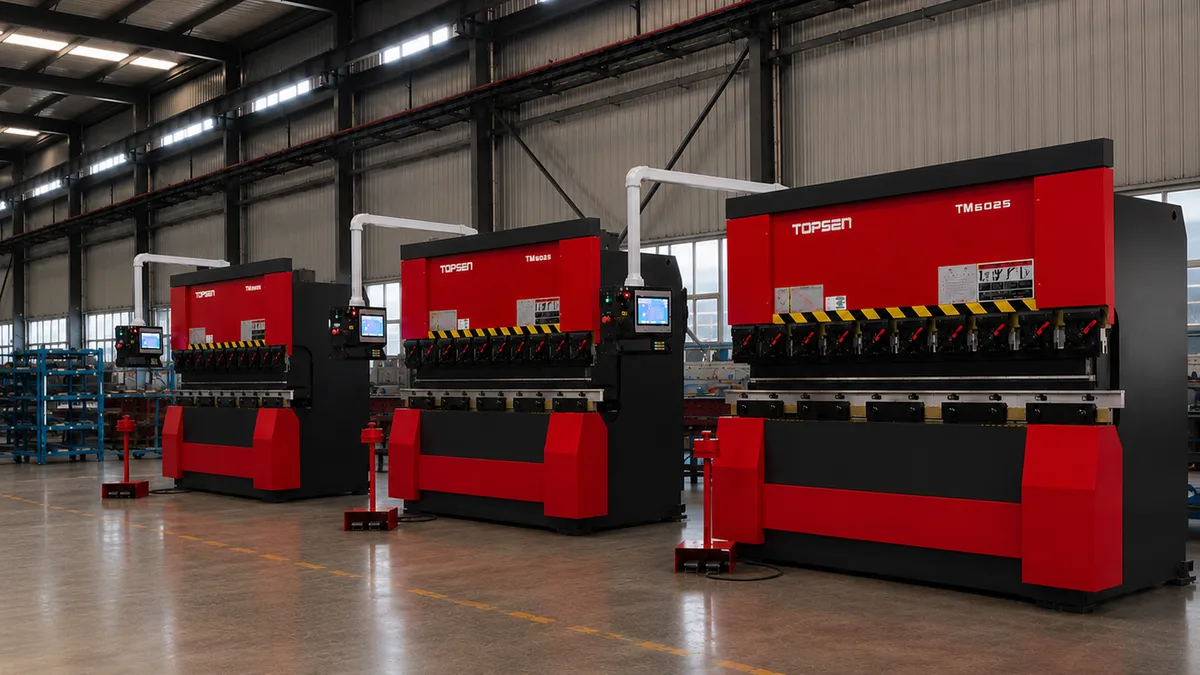
CNC Bending Center
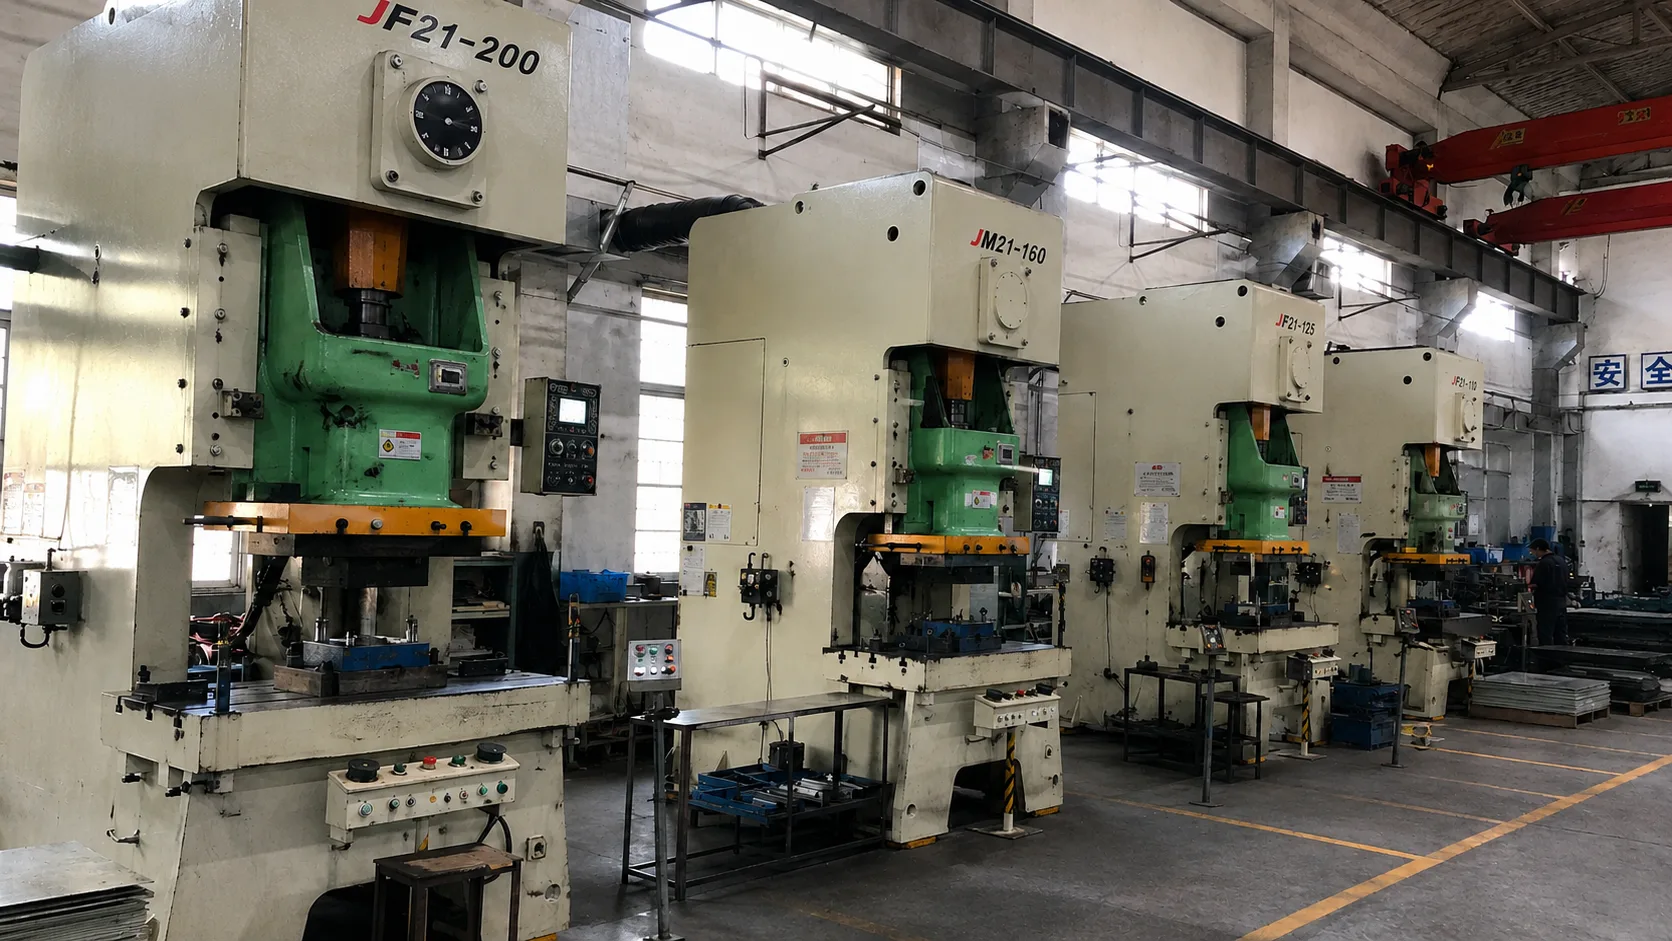
Stamping Center
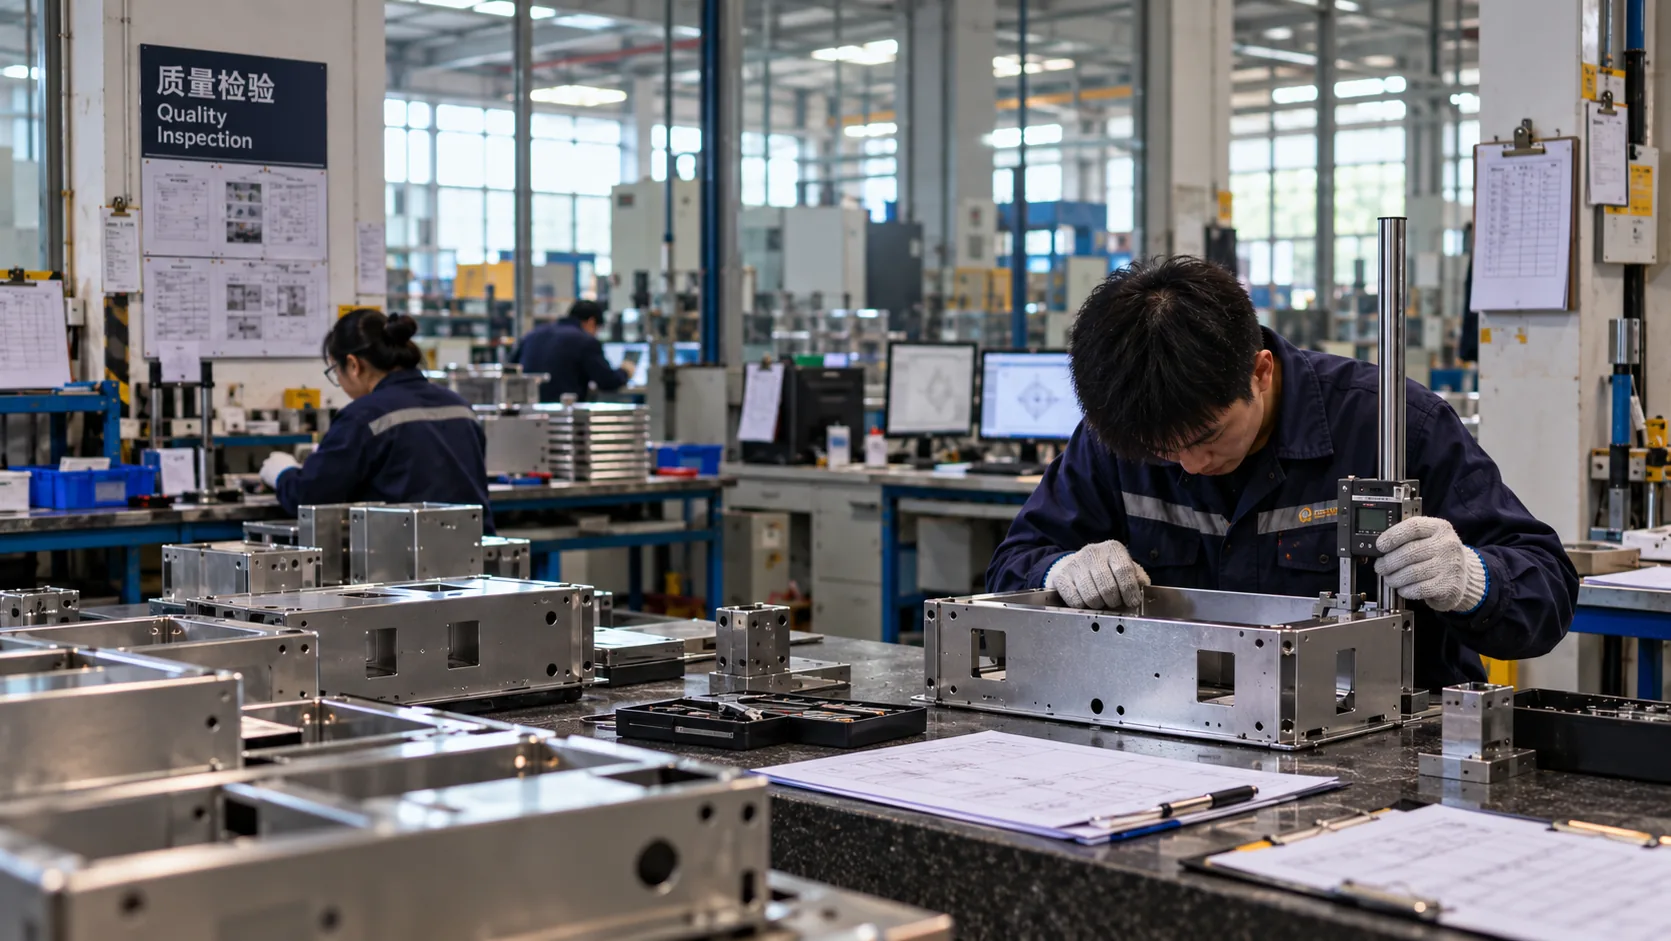
Quality Inspection Center
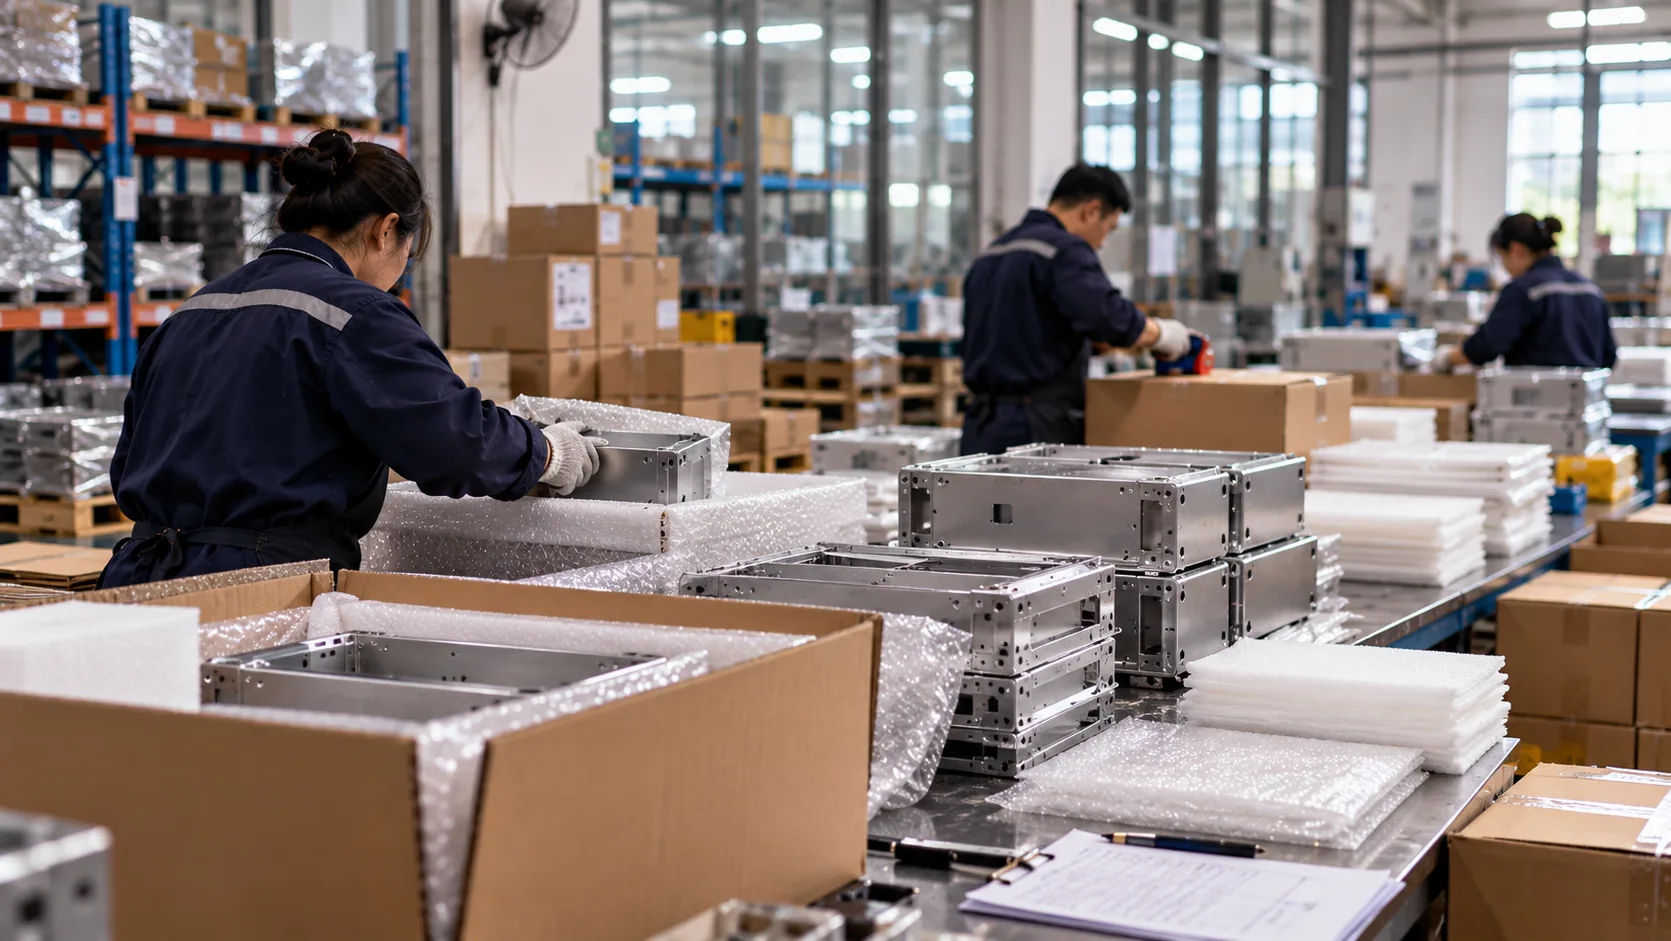
Packaging Center
Precision sheet metal parts for 14+ industries, fabricated and stamped to drawing
Custom sheet metal parts for 14+ industries — 5G cabinets to AI server racks.
- Power Grid & ElectricalJunction boxSGCC 1.5 mm · laser, bend, MIG · RAL 9005See parts for this industry
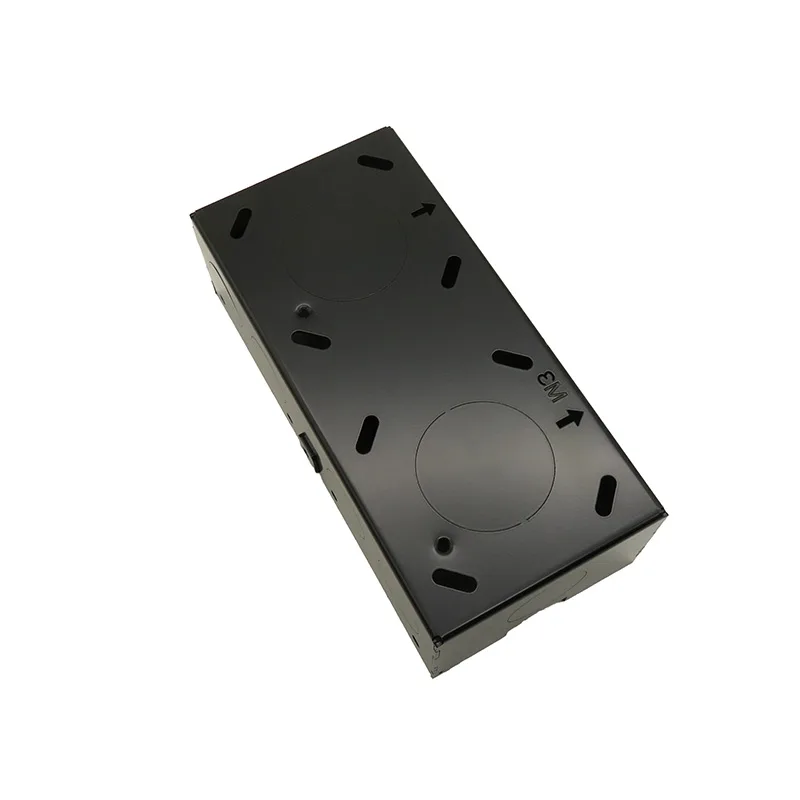
- Data Center & AIIndustrial PC chassisSPCC 1.2 mm · laser, bend, rivetSee parts for this industry
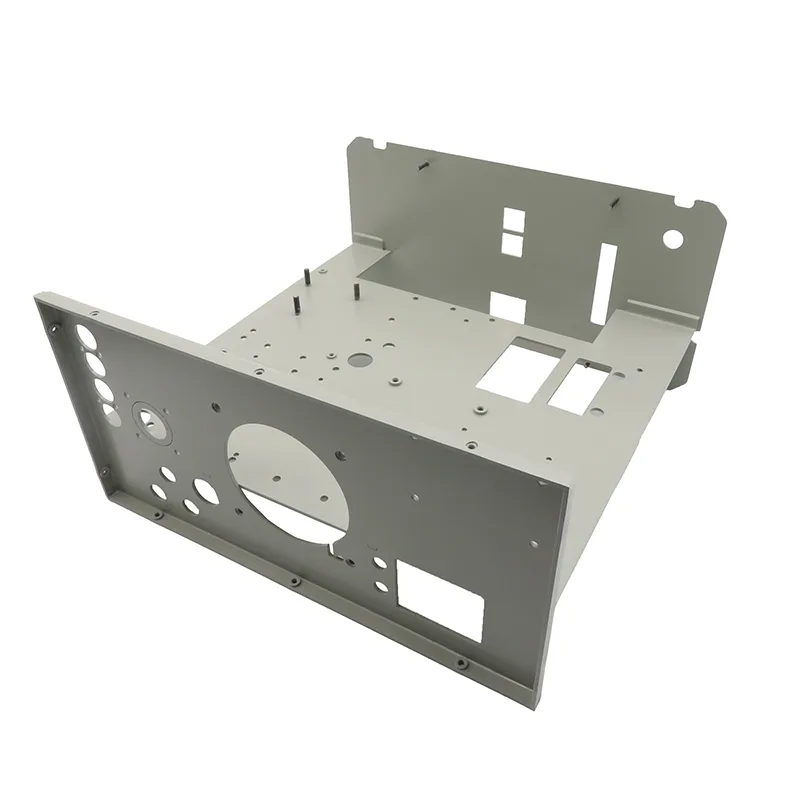
- Telecom & NetworkingTelecom equipment chassisSPCC 1.5 mm · laser, bend, MIG · powder coat silverSee parts for this industry
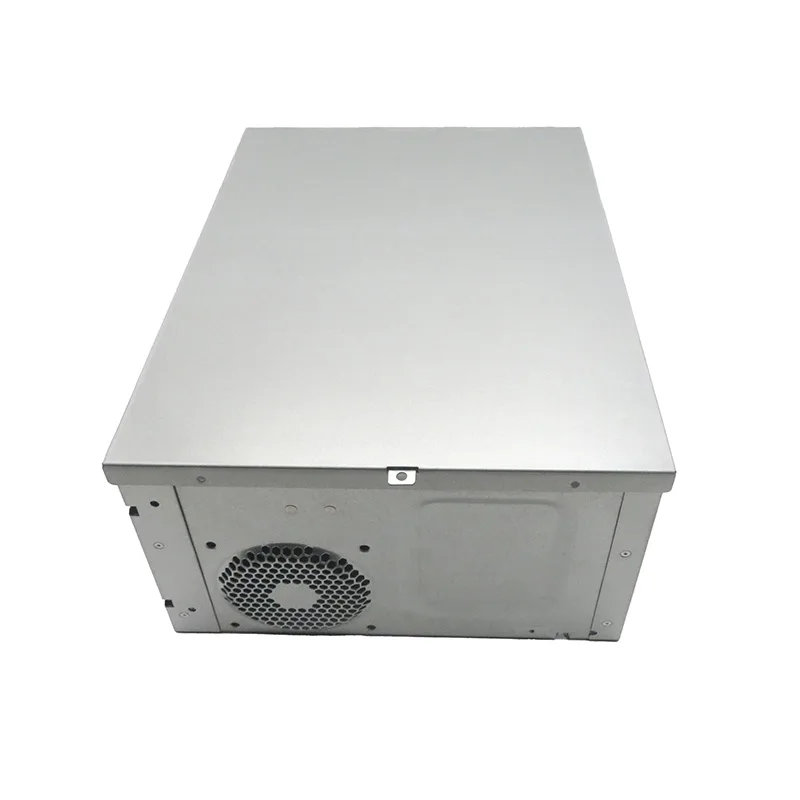
- New EnergyOutdoor energy storage enclosureSPCC 2.0 mm · laser, bend · RAL 9005See parts for this industry
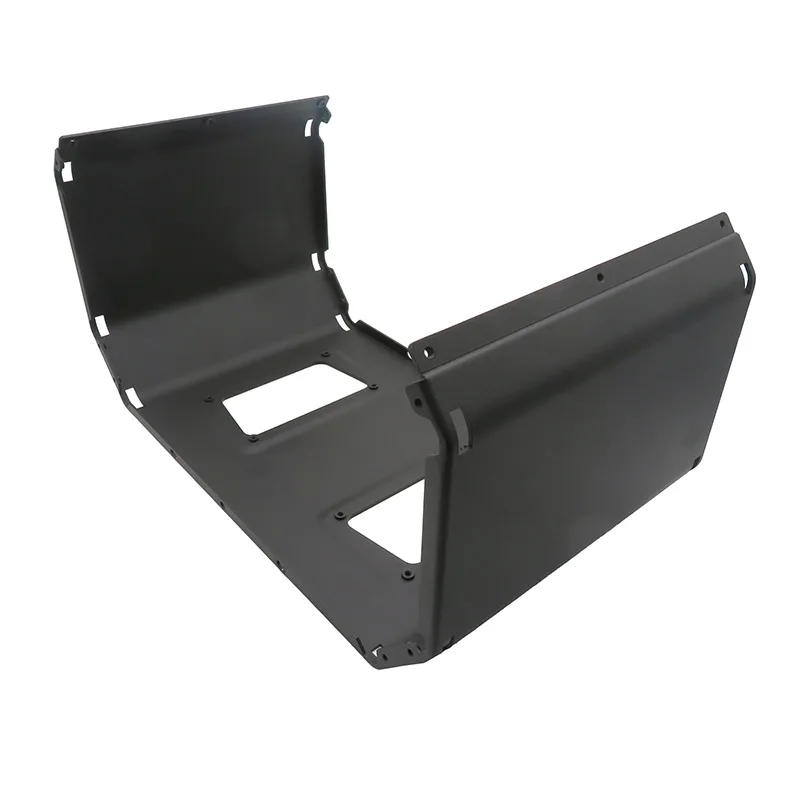
- Equipment & MachineryEquipment base plateAL5052-H32 2.0 mm · laser, bend · bead blastedSee parts for this industry
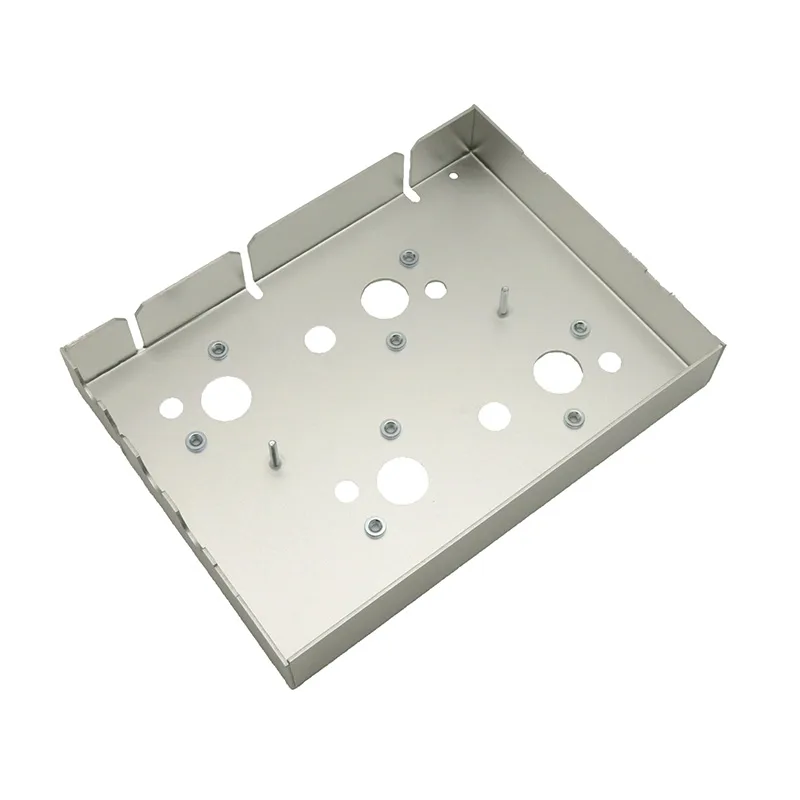
- Banking & FinancialBanking kiosk enclosure panelSECC 0.8 mm · laser, bend · zinc platedSee parts for this industry
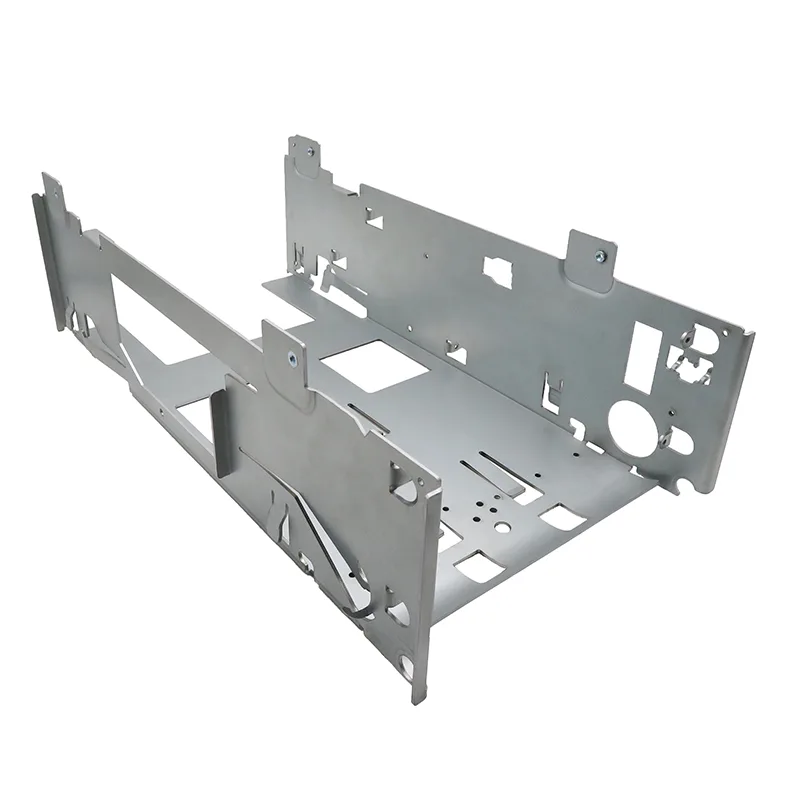
Industry index
Every industry we ship to, and the parts we make for it
- Telecom & networkingOutdoor 5G cabinets, ODF, small cell housings, antenna brackets
- Data center & AIGPU and 19-inch chassis, PDUs, liquid cooling, UPS cabinets
- New energy & EV chargingSolar inverter housings, BESS cabinets, charger enclosures
- Automotive & EVBattery trays, motor housings, seat frames, heat shields
- Industrial automationPLC cabinets, control panels, HMI housings, machine guards
- Consumer electronicsPC chassis, HiFi cases, smart-home housings, routers
- LED & displayDisplay cabinets, driver boxes, light housings, heat sinks
- RoboticsController cabinets, arm covers, teach pendant housings
- Power transmissionJunction boxes, distribution cabinets, meter enclosures
- Banking & kioskATM fascias, kiosk housings, cash drawer parts, security panels
- Home appliancesRange hoods, washer drums, refrigerator panels, AC outdoor units
- Industrial equipmentMachine bases, covers, guards, hydraulic tanks
- 3D printing hardwarePrinter frames, gantry plates, heated bed mounts, enclosures
- Anything else, to drawingOne-off and non-standard parts, made from your drawing alone
Where is your project today?
From a single prototype to 100,000+ units a year — pick the route that matches where you are.
Rapid Prototyping
Production-grade parts in 3–7 days. No die cost. Same materials and processes as your full run — so what you test is what you get at scale.
Low Volume Production
50+ parts, delivered in 7–15 days. No die cost. Continuous quality monitoring and full batch traceability on every order.
Mass Production / NPI
Full 8-phase NPI under one roof — from design review and tooling to first-article inspection and scaled production. One team, one purchase order, no transfer risk.
A sheet metal manufacturer and supplier in Dongguan, China, shipping to 30+ countries
One factory in Dongguan, China — the sheet metal supplier behind hardware programmes in 30+ countries. OEM and ODM contract manufacturing under one roof, with English-speaking engineers answering within 24 hours, whichever time zone you are in.

Customer Reviews
Verified feedback from buyers across 30+ countries.
"Jack aus dem Engineering-Team hat uns deshalb im Rahmen einer DFM-Prüfung empfohlen, die Teile stattdessen mit Laserschneiden und CNC-Abkanten zu fertigen. Er hat uns die Vor- und Nachteile verständlich erklärt, sodass wir die Entscheidung gut nachvollziehen konnten. Wir hatten das Gefühl, dass nicht einfach nur ein Auftrag abgewickelt werden sollte, sondern dass wirklich nach einer passenden Fertigungslösung gesucht wurde."
"We evaluated four Asian suppliers before committing to these guys. What set them apart was the DFM feedback — they flagged a sharp internal radius that would have cracked in SPCC at 1.5mm and recommended 2mm with a 3× bend radius. First article laser cuts were within ±0.1mm, bend angles matched our GD&T callouts perfectly across a 300-piece pilot."
"Passed our incoming inspection first time. Also requested electropolishing instead of standard brushed finish and they adapted without any fuss. Quote turnaround was under 24 hours which helped us hit our project deadline. Would definitely order again."
Sheet metal fabrication services, all in one factory
Custom sheet metal fabrication is the process of cutting, forming and joining flat metal into finished parts, enclosures and assemblies. WERIX runs fiber laser cutting, CNC press brake bending, TIG and MIG welding, progressive die stamping and six surface finishes in one Dongguan factory — from a single prototype to 100,000+ units per order.
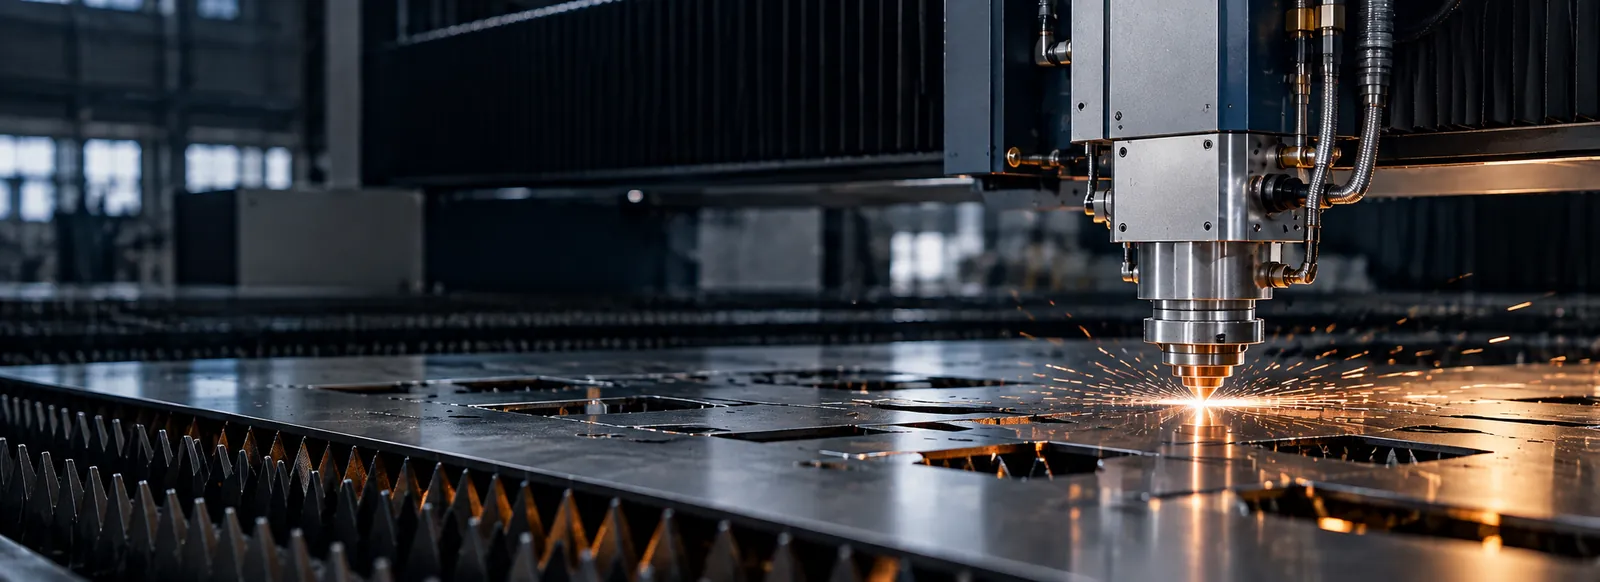
CNC sheet metal fabrication
Flat sheet cut and formed to order. No hard tooling, so a new revision costs nothing but the machine time.
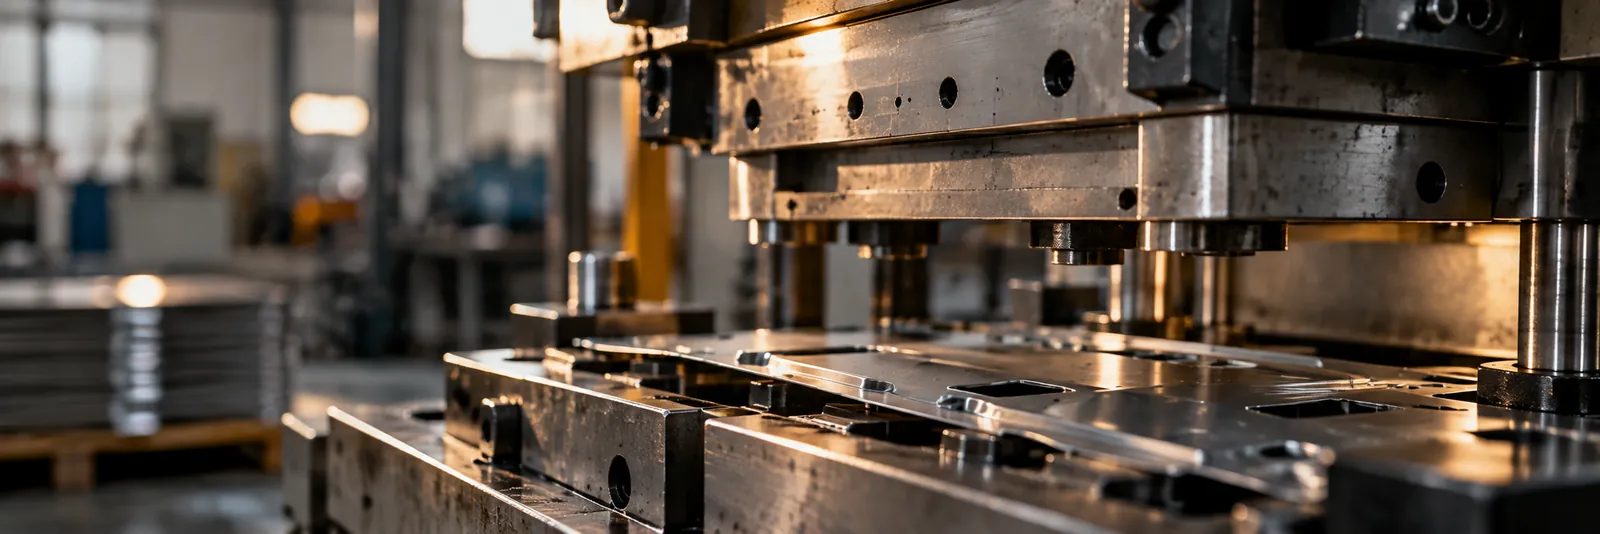
Metal stamping and tooling
Hard tooling built in our own die shop. Uneconomic for a prototype, unbeatable once a part repeats at volume.
Around those processes: the laser takes sheet to 3,000 × 1,500 mm, the press brakes bend parts to 3,100 mm with a CNC backgauge at ≤0.02 mm repeatability, and the stamping lines run from 25T to 300T at up to 200 strokes a minute — with sheet metal welding and sheet metal assembly in the same building. Unless the drawing says otherwise we work to ISO 2768-1 class m general tolerances and call out anything tighter on the drawing.
Material and tolerance specifications follow ISO 2768-1 general tolerances, ASTM A480/A480M stainless sheet, ISO 9001 quality management, IEC 60529 enclosure IP ratings and EU RoHS restricted substances. Every production run ships with an inspection report written against your drawing.
12+ sheet metal grades on the floor, and the parts we cut from them
From 0.1 mm phosphor bronze strip for stamped contacts to 8 mm hot-rolled plate for machine bases. Common grades and thicknesses are held in stock for same-week cutting; anything outside that is sourced to order and confirmed at quotation. Name the operating environment and we will point at the cheapest grade that survives it.
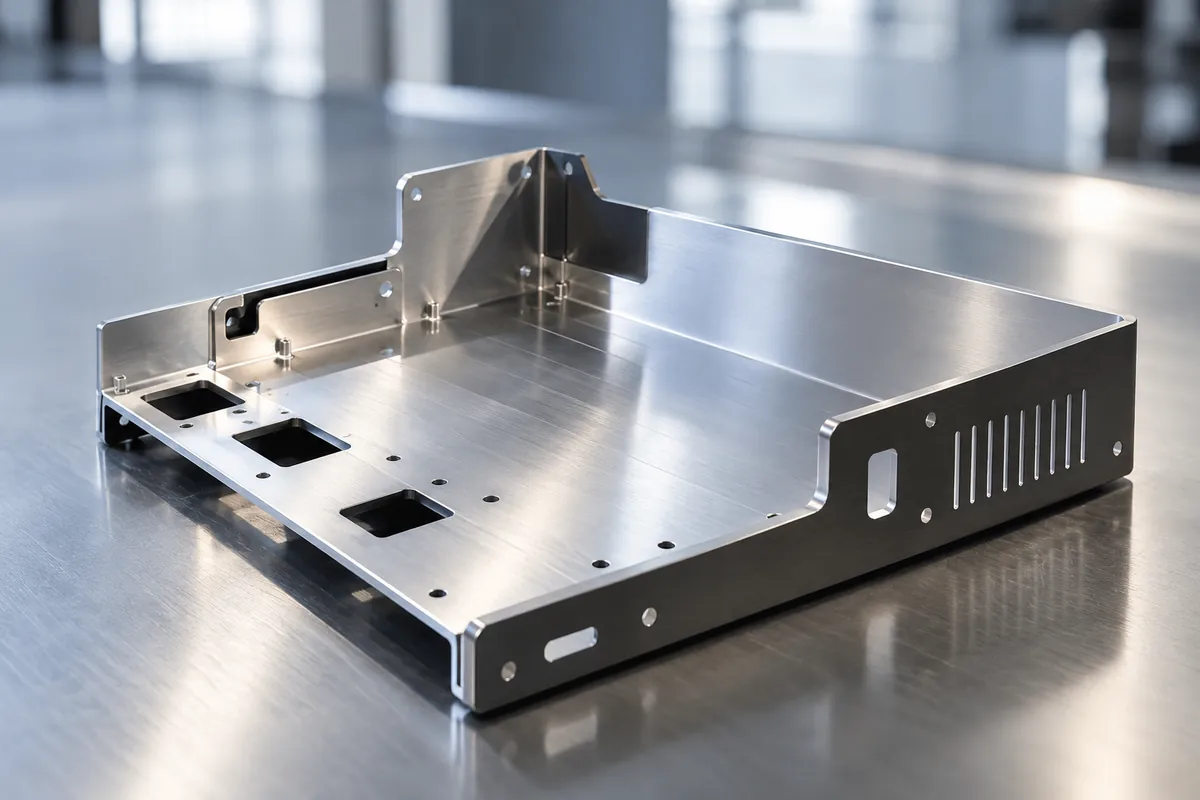
Aluminum
Chosen for weight and formability, never for price. 5052 takes a tight bend without cracking, 6061 machines after forming.
- 5052 aluminumASTM B2090.5–5.0 mm
- Best bendability of the common alloys — it rarely cracks at a tight radius. Chassis, enclosures.
- 6061-T6 aluminumASTM B2091.0–6.0 mm
- Stiffer and machinable. Use it where a formed part also needs milled pockets or tapped bosses.
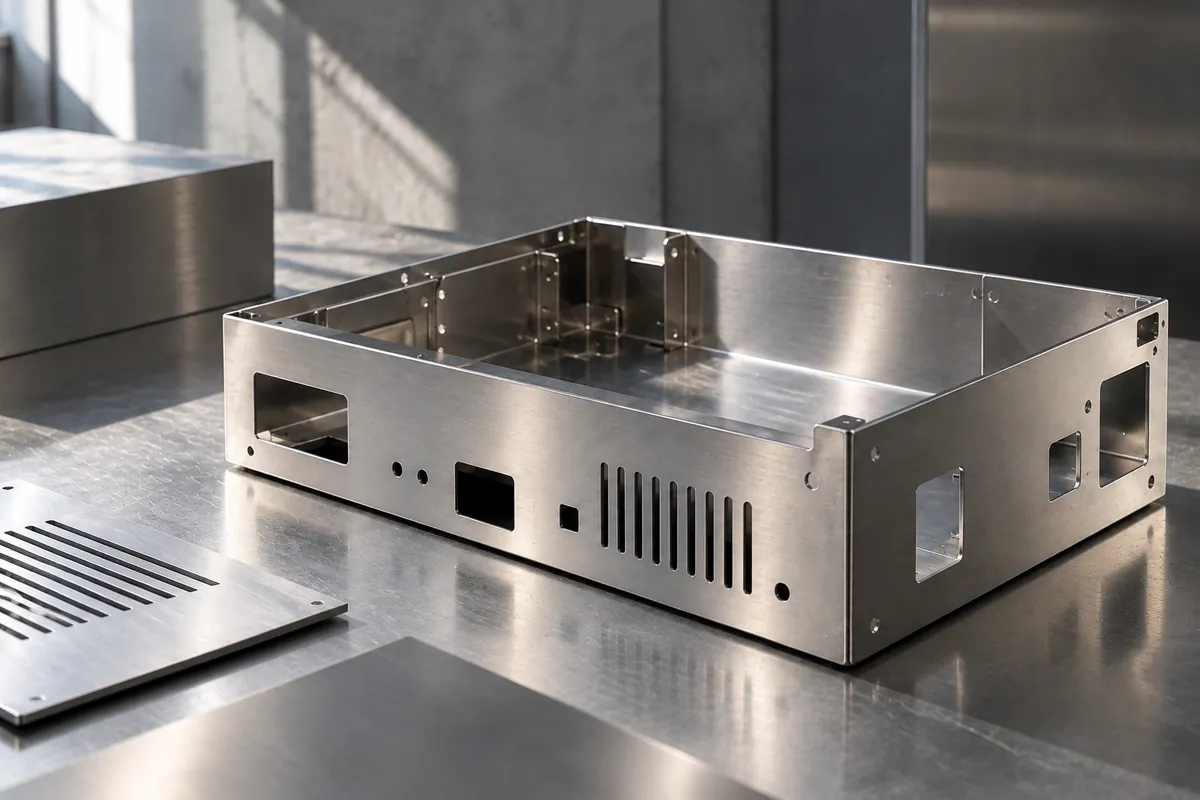
Two grades cover almost every corrosion problem. If you are unsure, 304 is the answer nine times out of ten.
- 304 stainless steelASTM A2400.5–4.0 mm
- The general-purpose stainless. Food equipment, medical housings, wash-down areas.
- 316L stainless steelASTM A2400.5–4.0 mm
- Molybdenum for chlorides. Coastal sites, chemical plant, marine electronics.
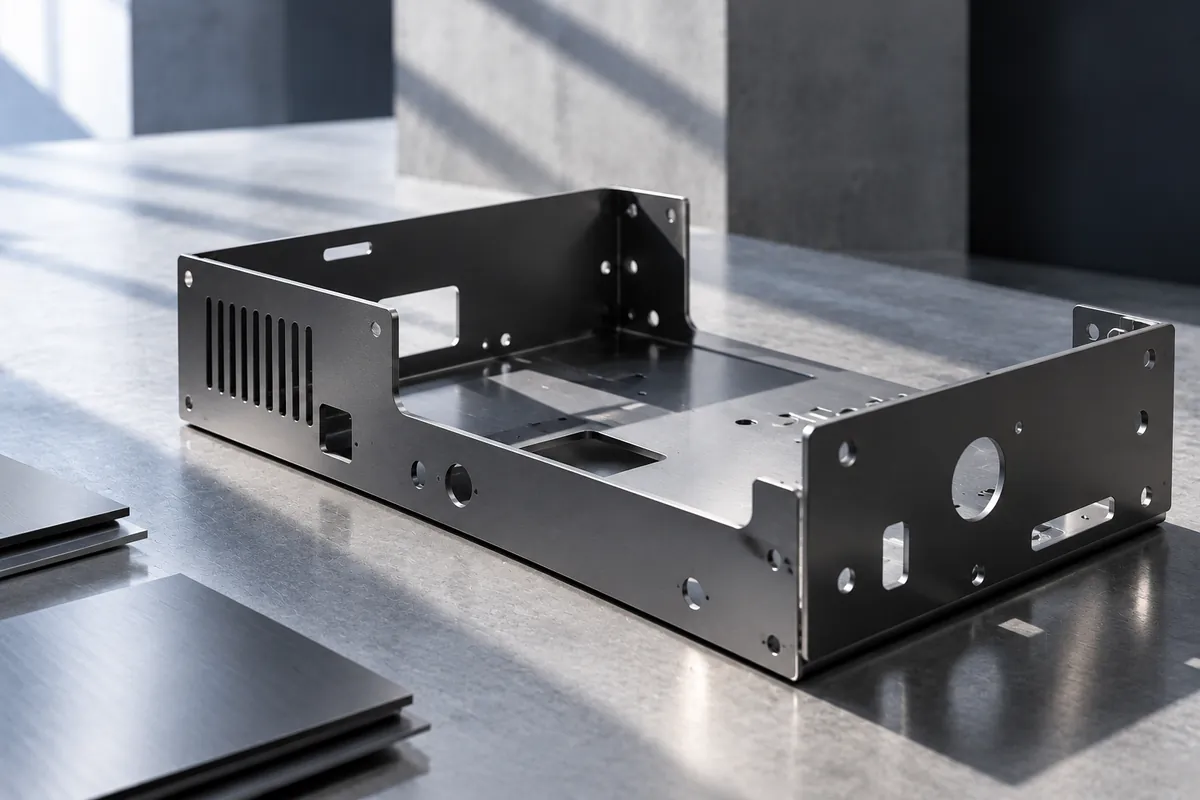
The volume metal — cheapest per kilo and the easiest to weld. SGCC arrives already zinc-coated, so the finish can be skipped on outdoor cabinets.
- SPCC cold-rolled steelJIS G31410.4–3.0 mm
- Default for brackets and chassis. Welds clean, takes paint, rusts the moment the finish is skipped.
- SGCC hot-dip galvanized steelJIS G33020.5–3.0 mm
- Zinc survives a sheared edge, so outdoor cabinets can go bare without a paint line.
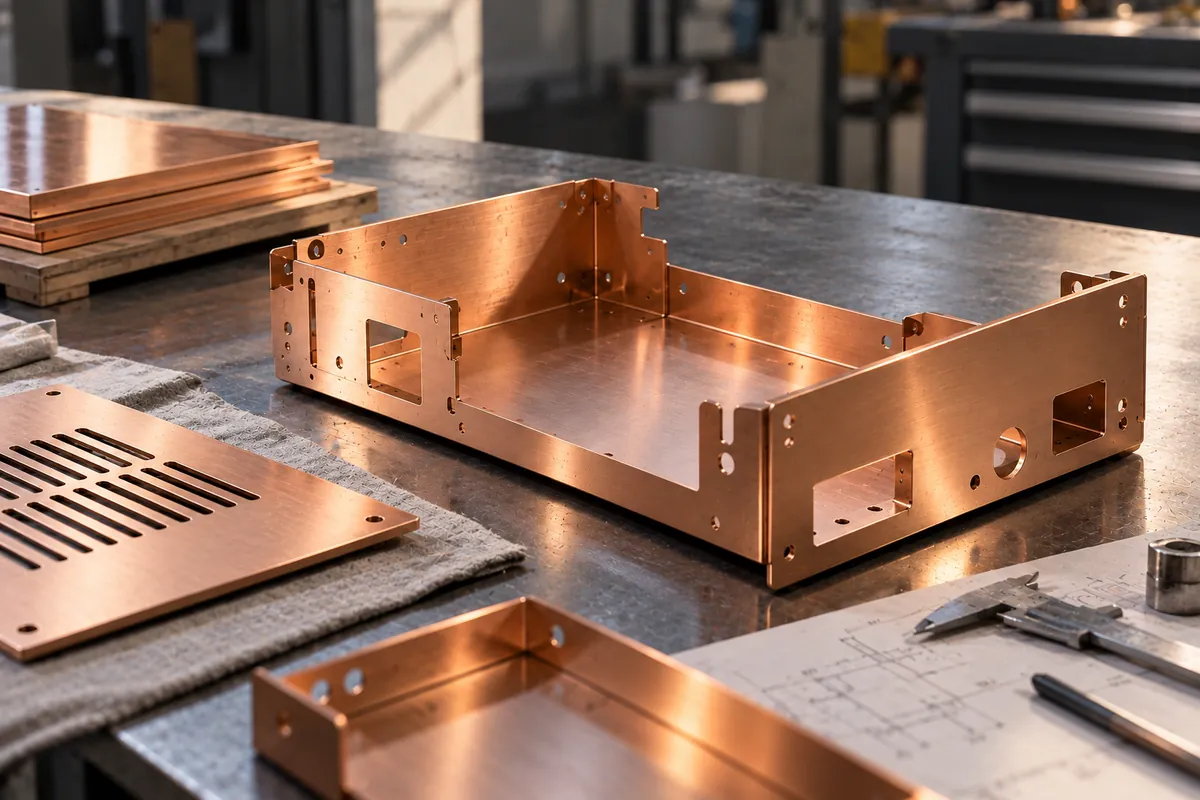
Specified for conductivity and plating, not for structural strength. C11000 carries current, C26000 forms and takes bright plating.
- C11000 copperASTM B1520.5–3.0 mm
- Busbars and current-carrying parts. Say so if it must be tinned or silver-plated.
- C26000 brassASTM B360.4–2.0 mm
- RF shielding, terminals, decorative trim — it takes bright plating better than steel.
Certificates of conformity travel with the shipment. Name a grade we do not list and we will quote the nearest equivalent we can hold in stock — or tell you plainly that we cannot.
Hold the material before you commit
Photographs flatten a finish and hide a grain direction. We post physical coupons instead: same alloys and tempers as production, labelled with grade and mill standard.
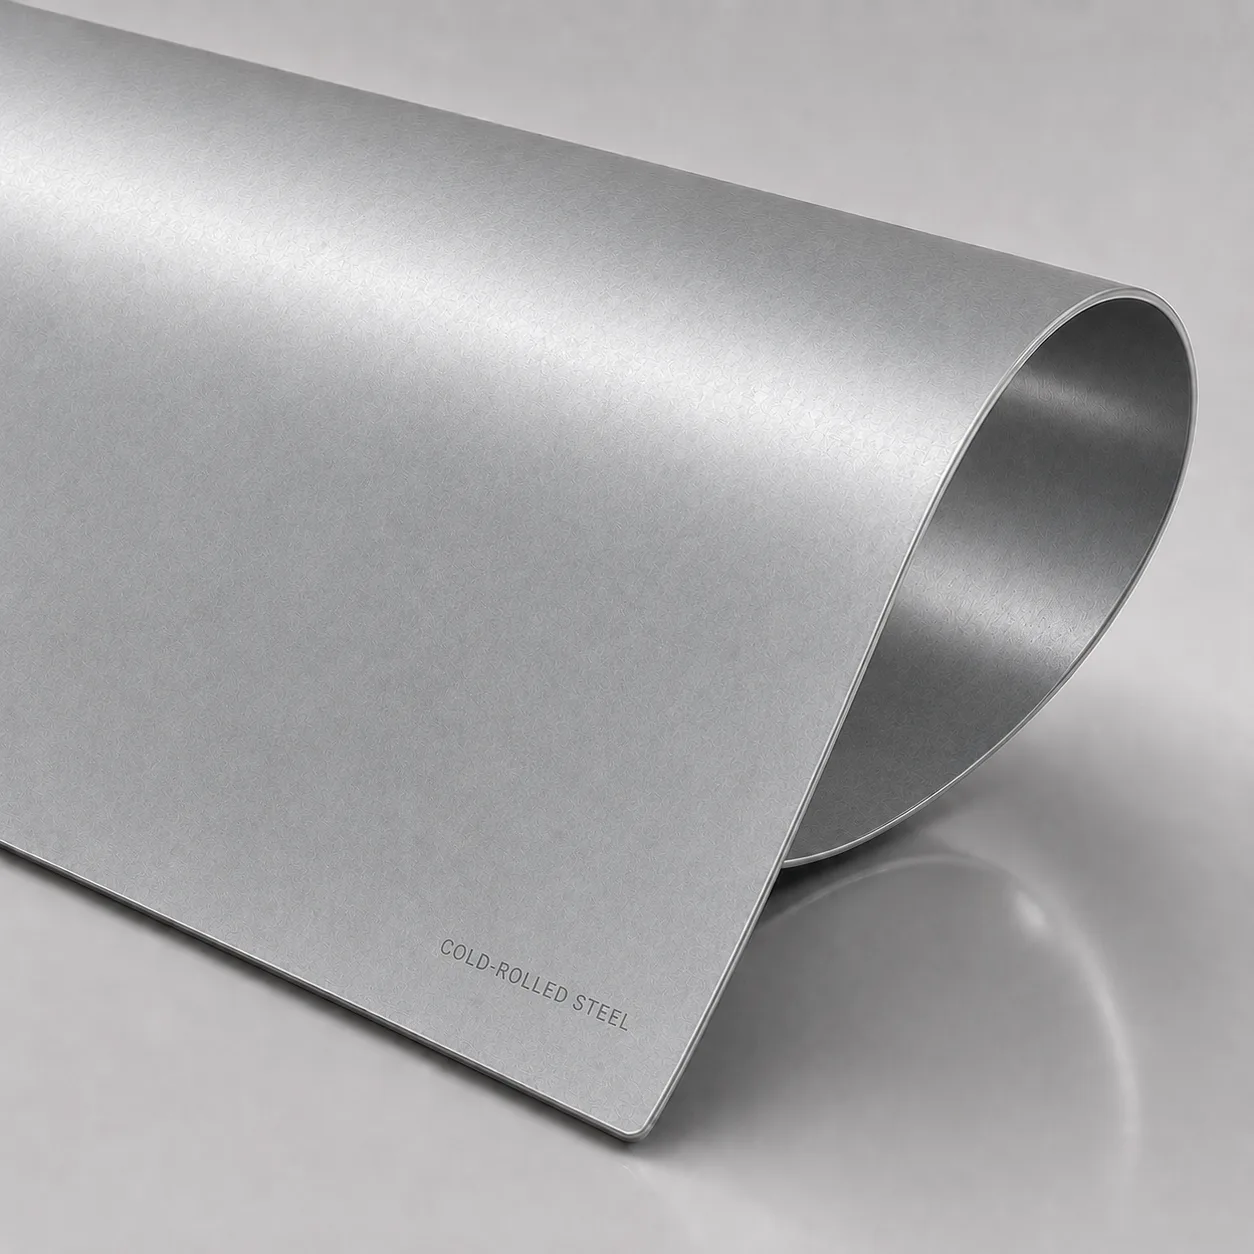
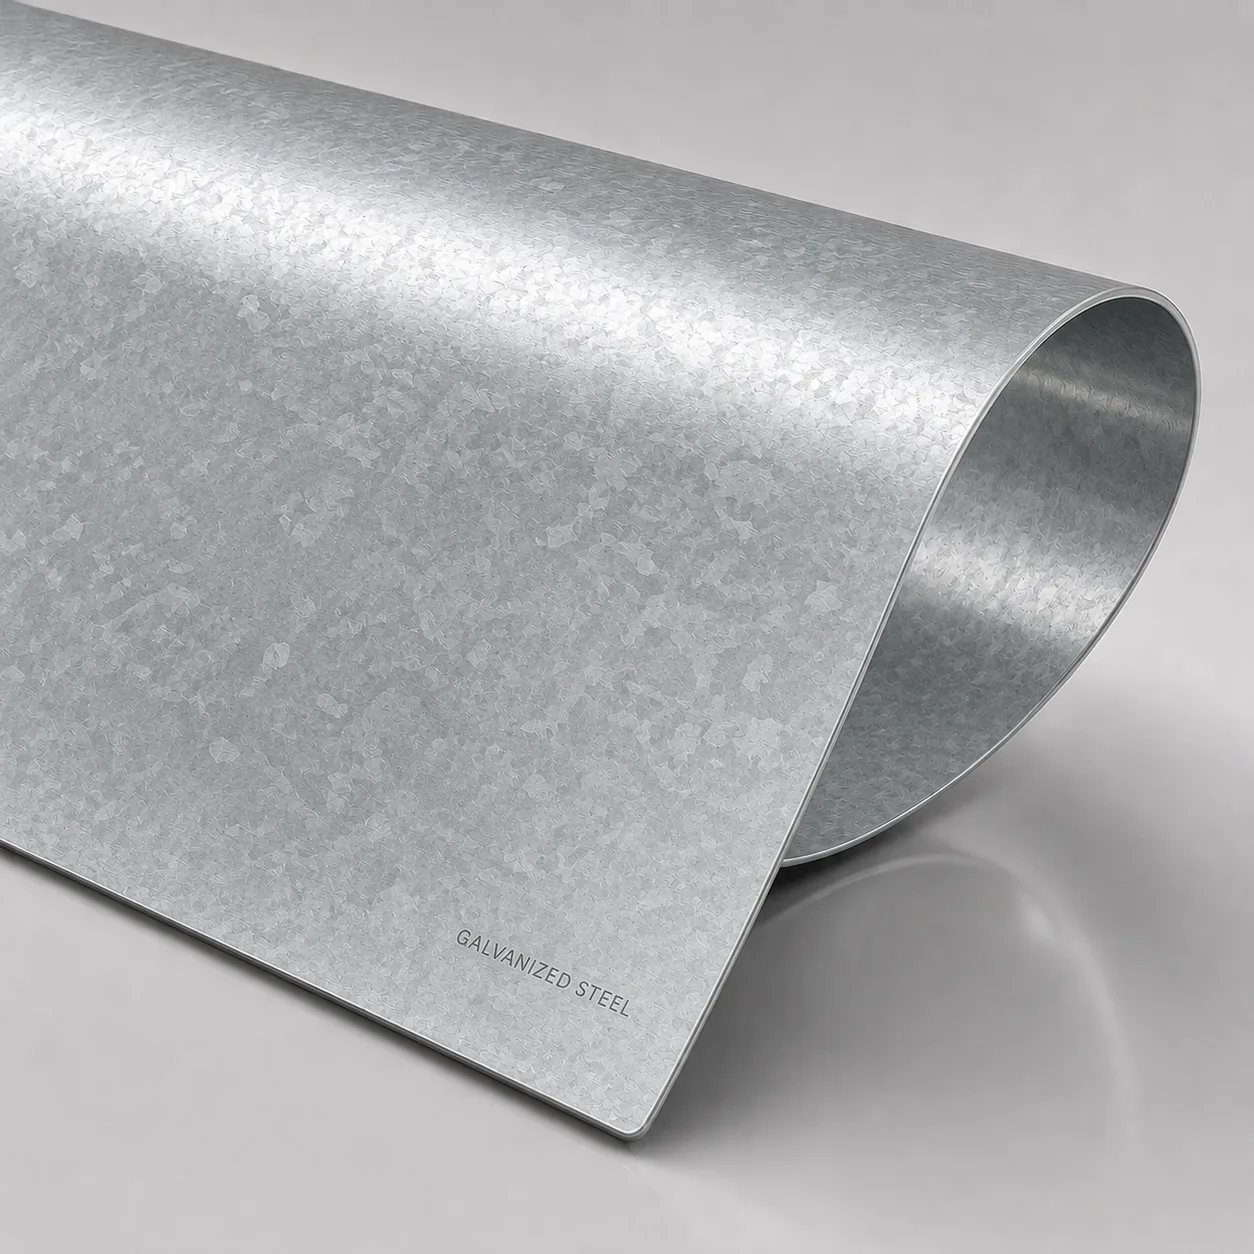
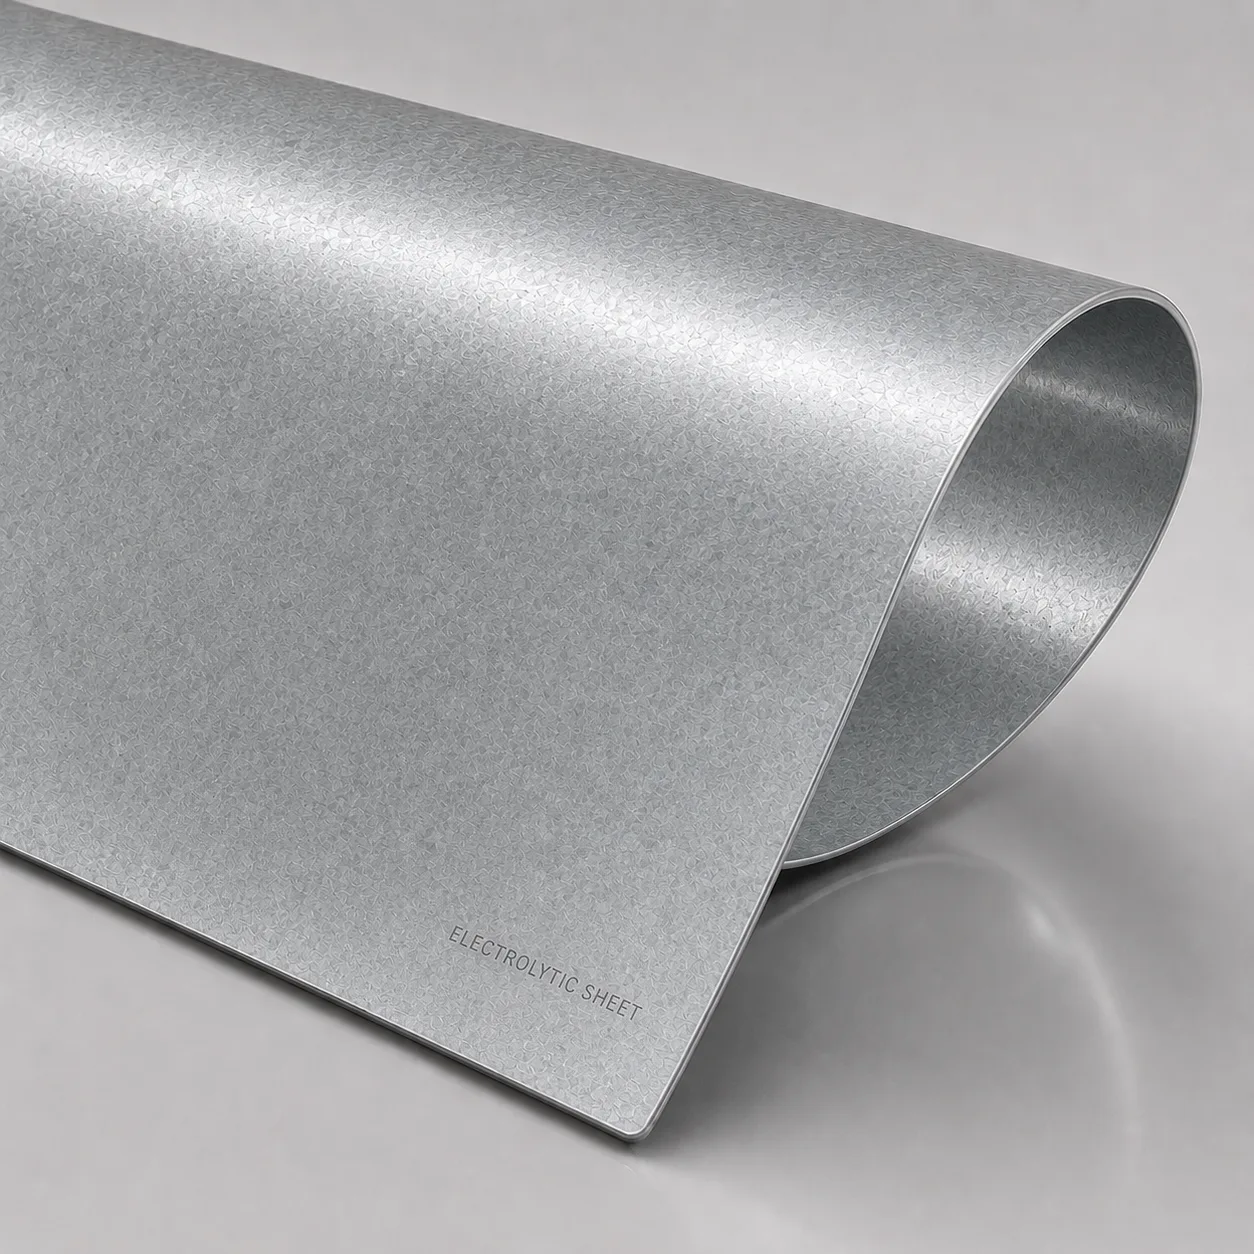
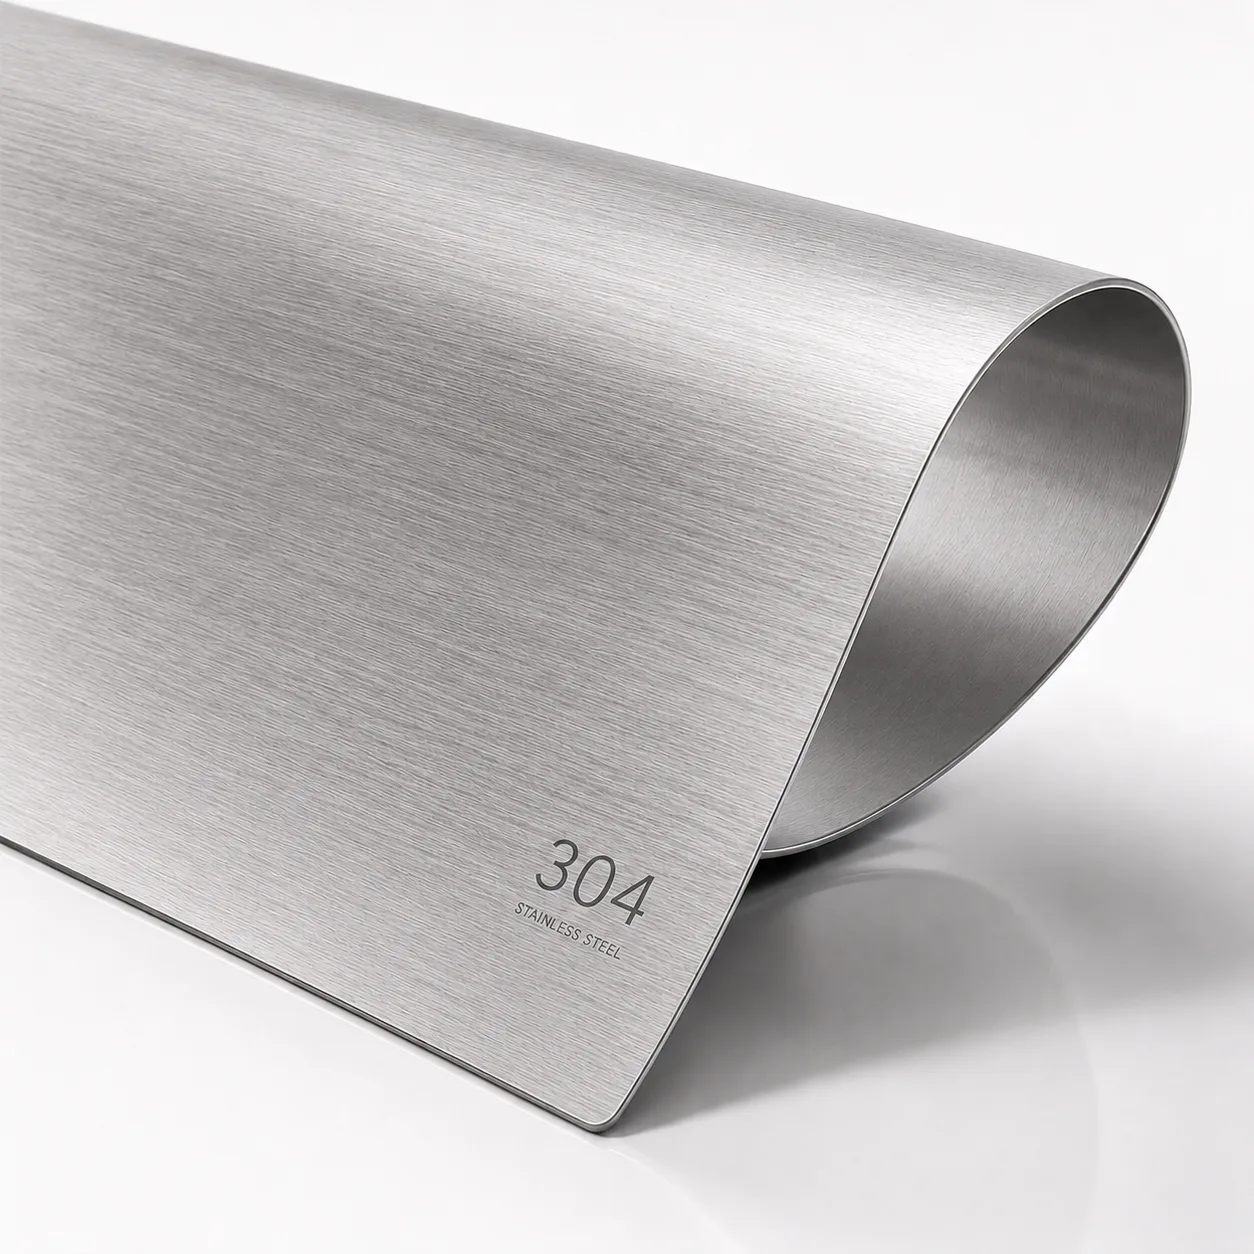

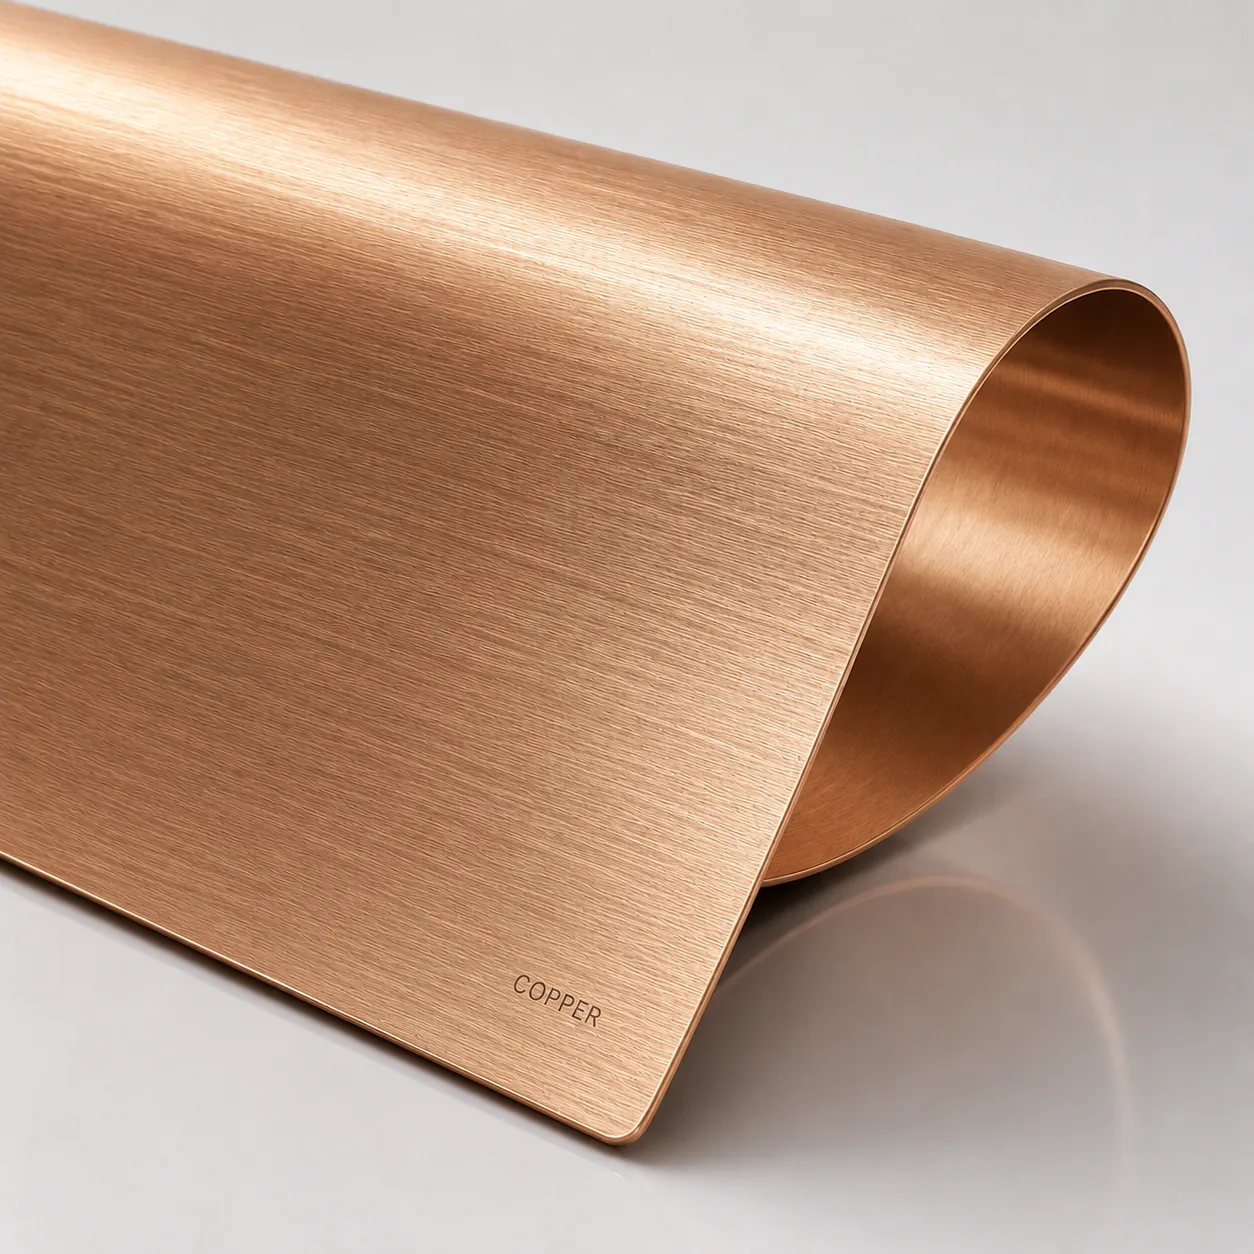
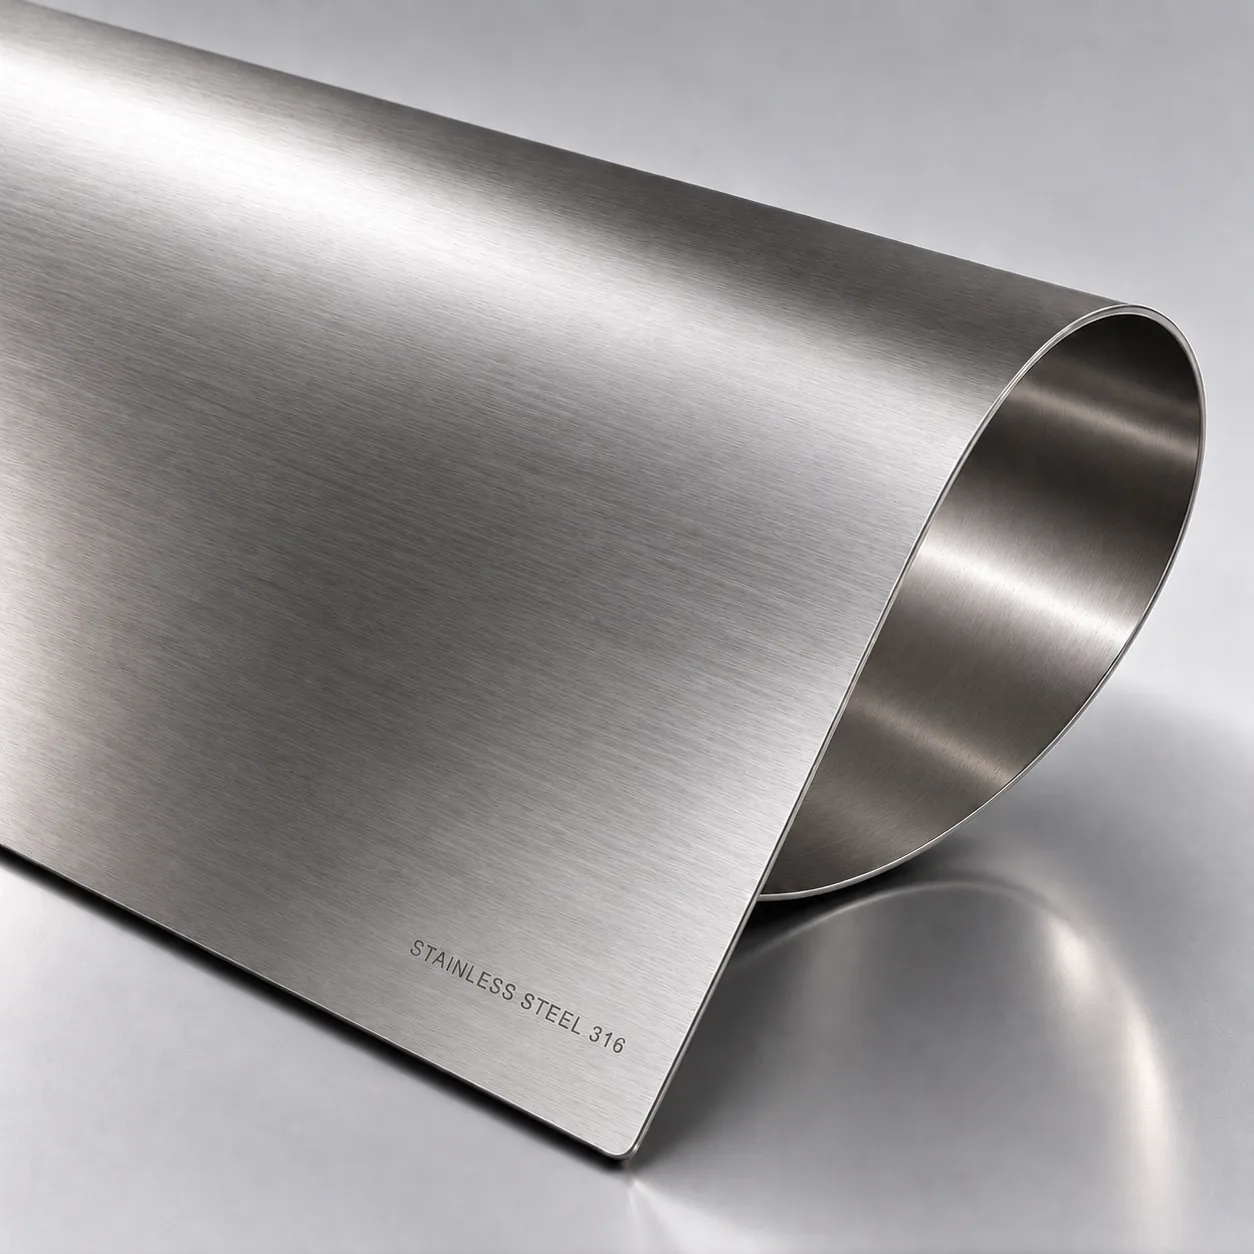
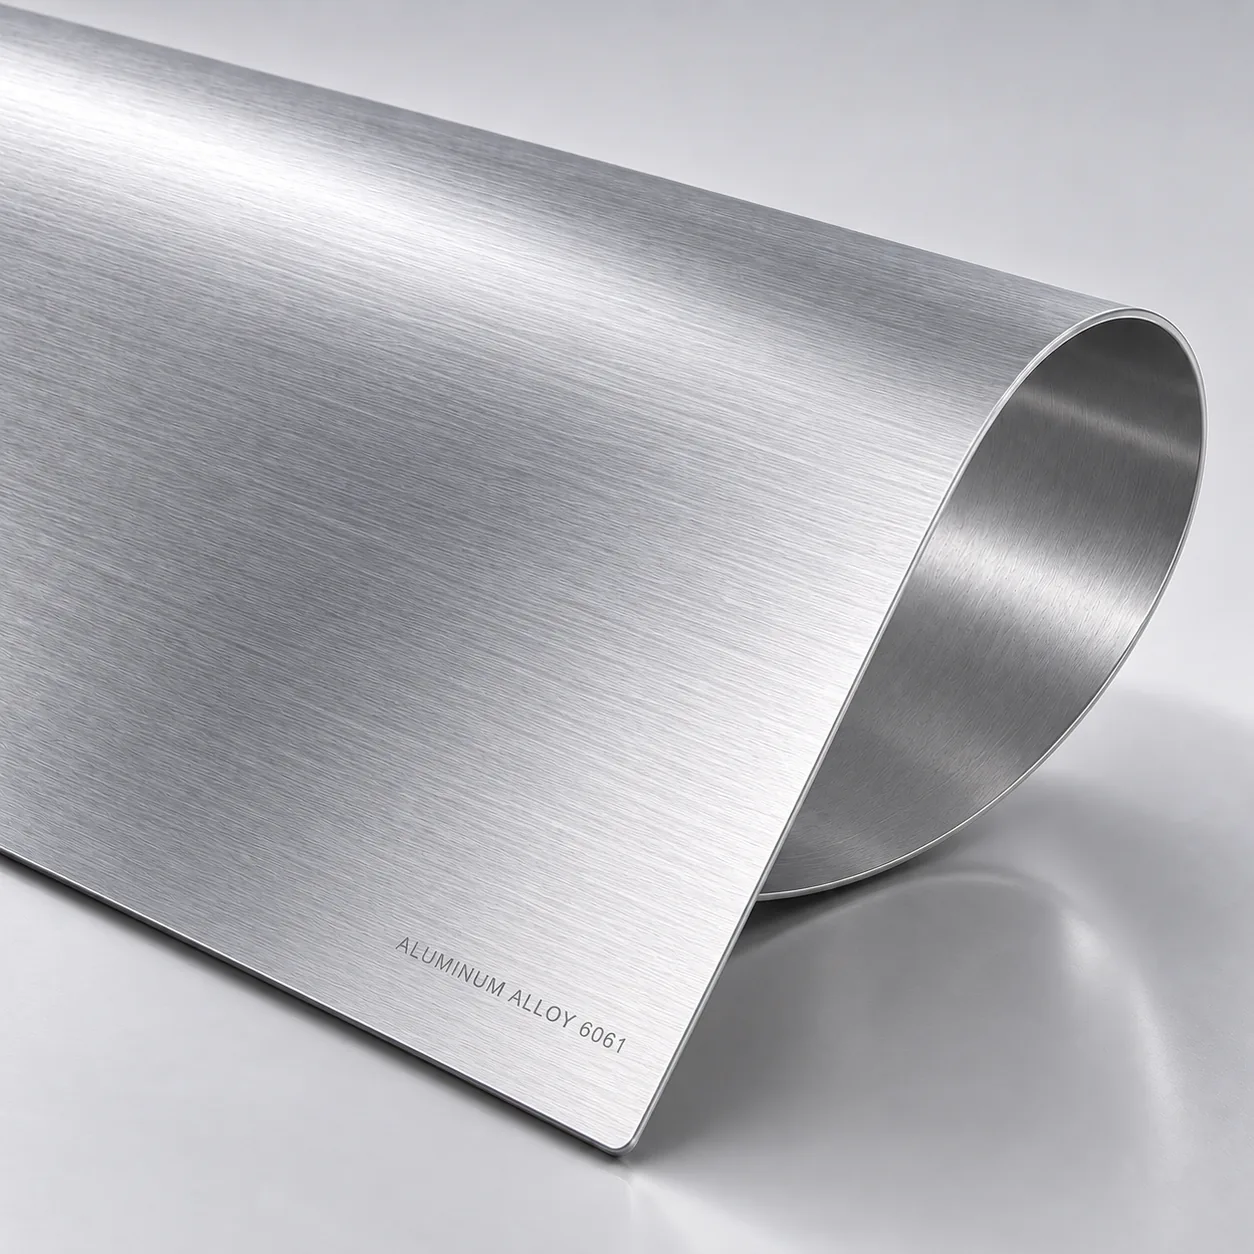
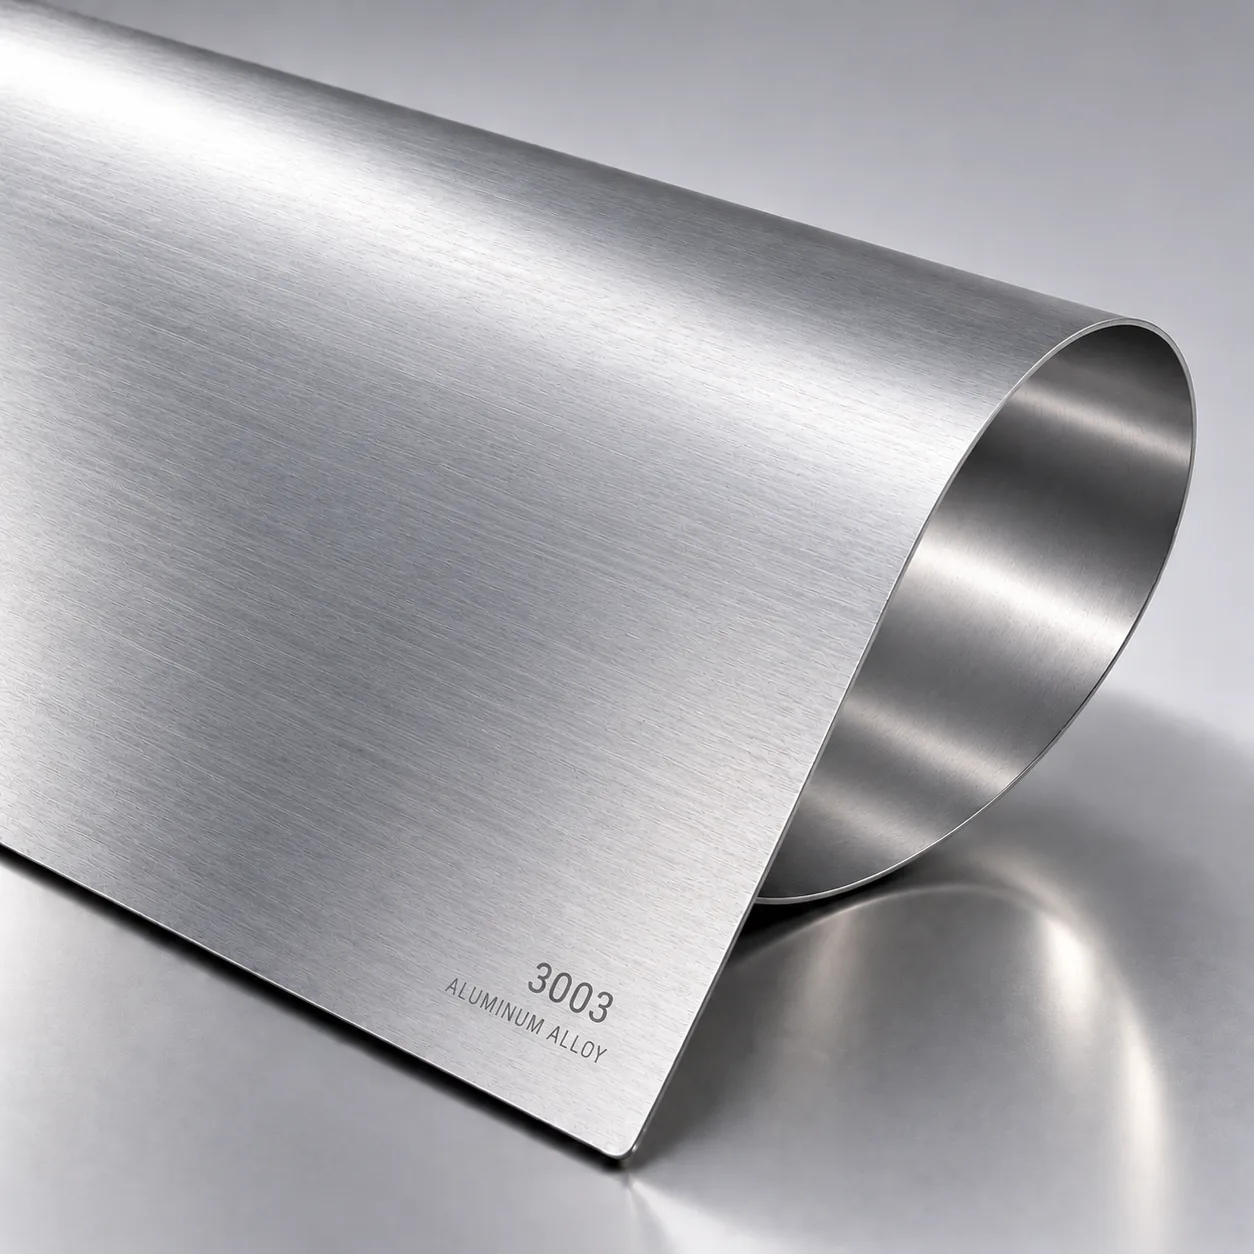
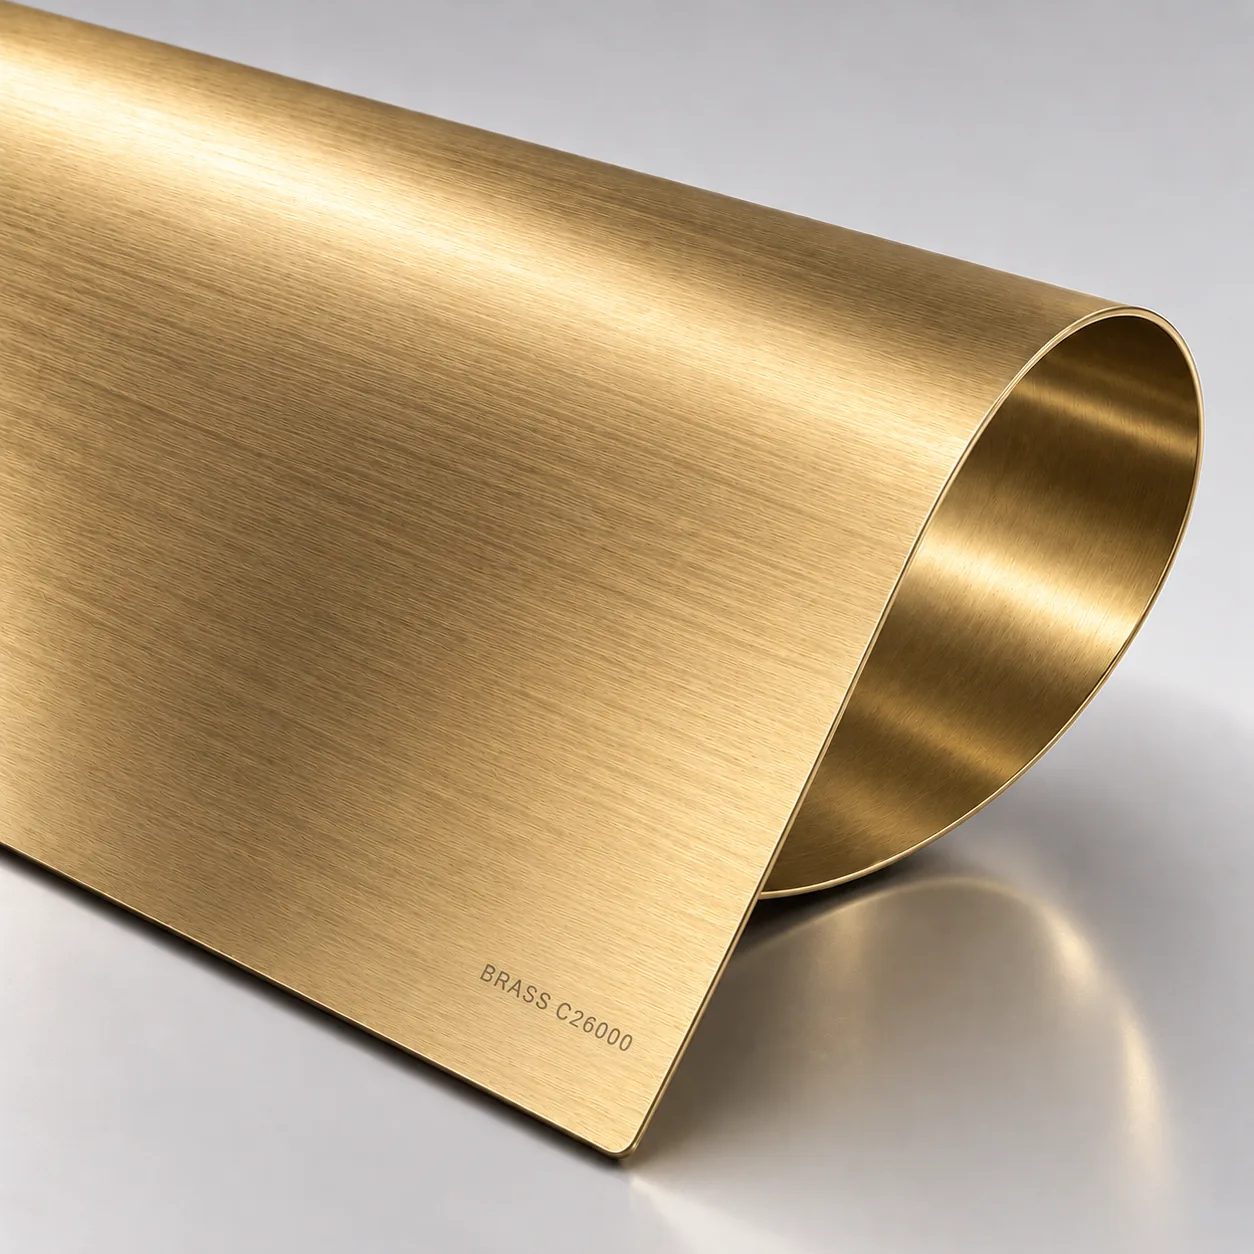
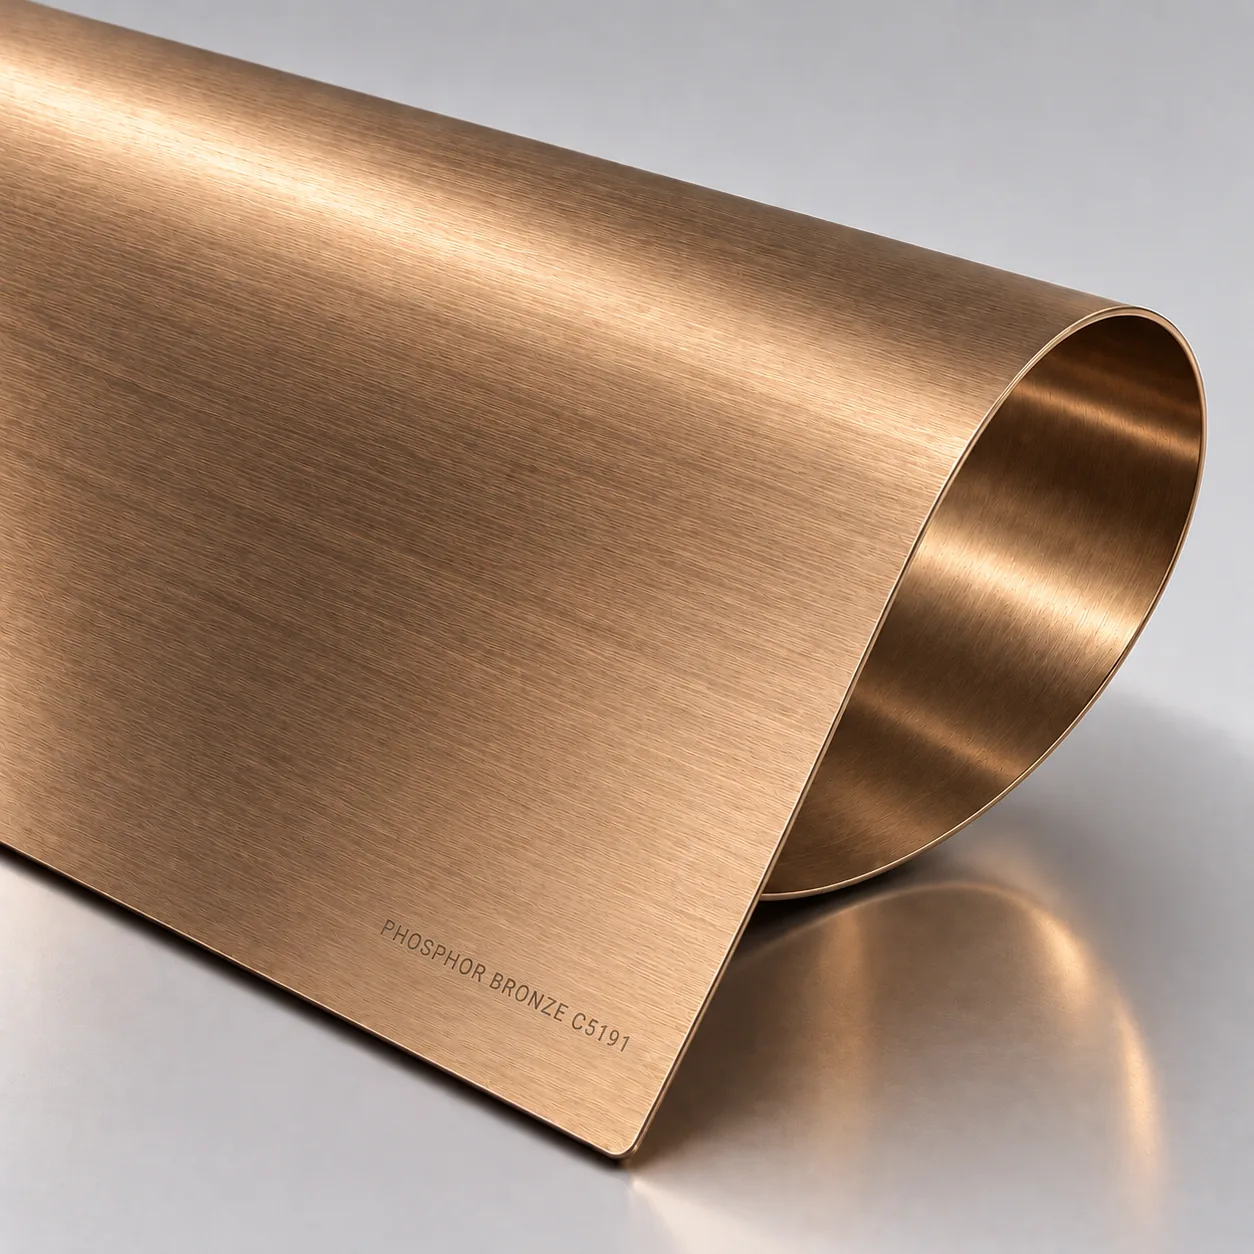
Posted worldwide, free, with the grade and mill standard written on each tag.
Surface finishes for sheet metal parts
Finish is the last decision a buyer makes and the first one that fails in the field. We quote six finishes against the environment the part lives in, not the look book.
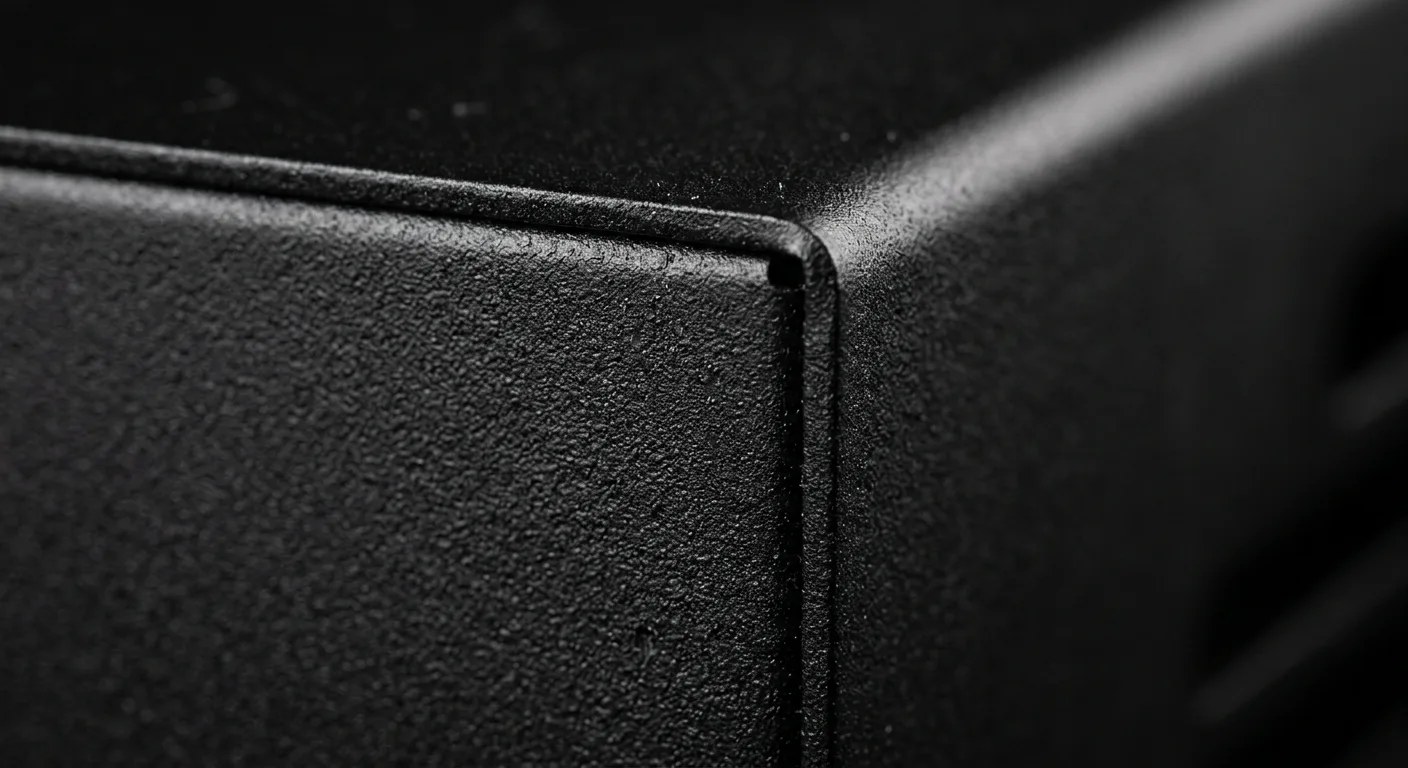 Powder coating60–120 μmRAL and Pantone matched, flat to fine texture. The default for outdoor steel.
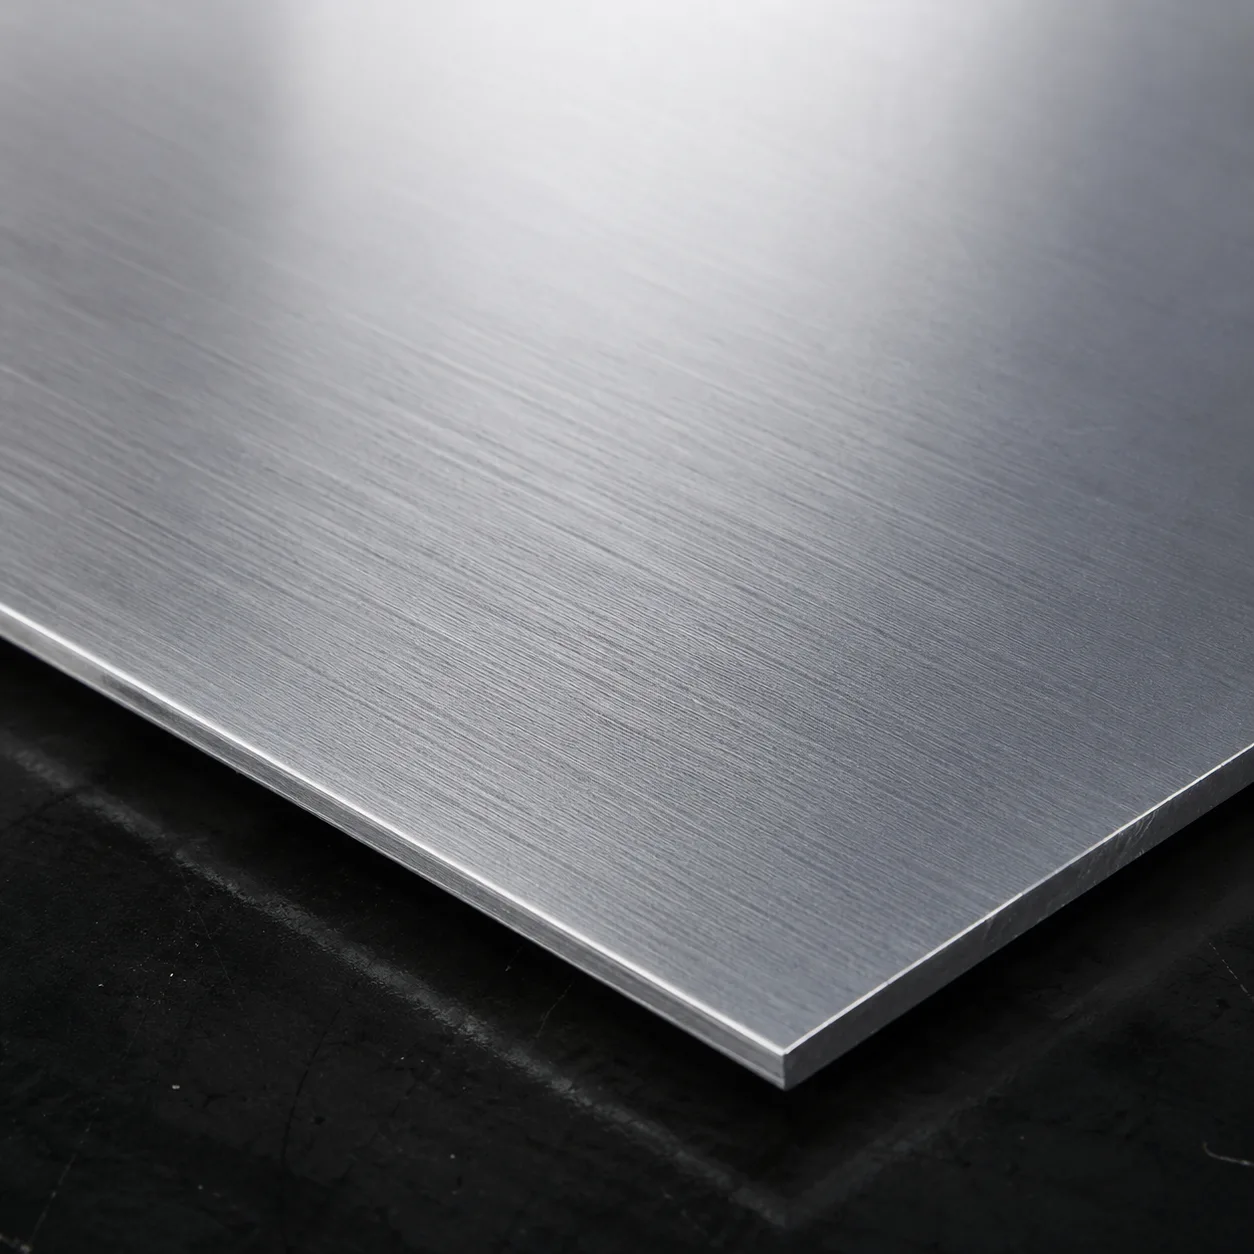 AnodizingType II / III5–50 μm on aluminium only. Mask the grounding points.
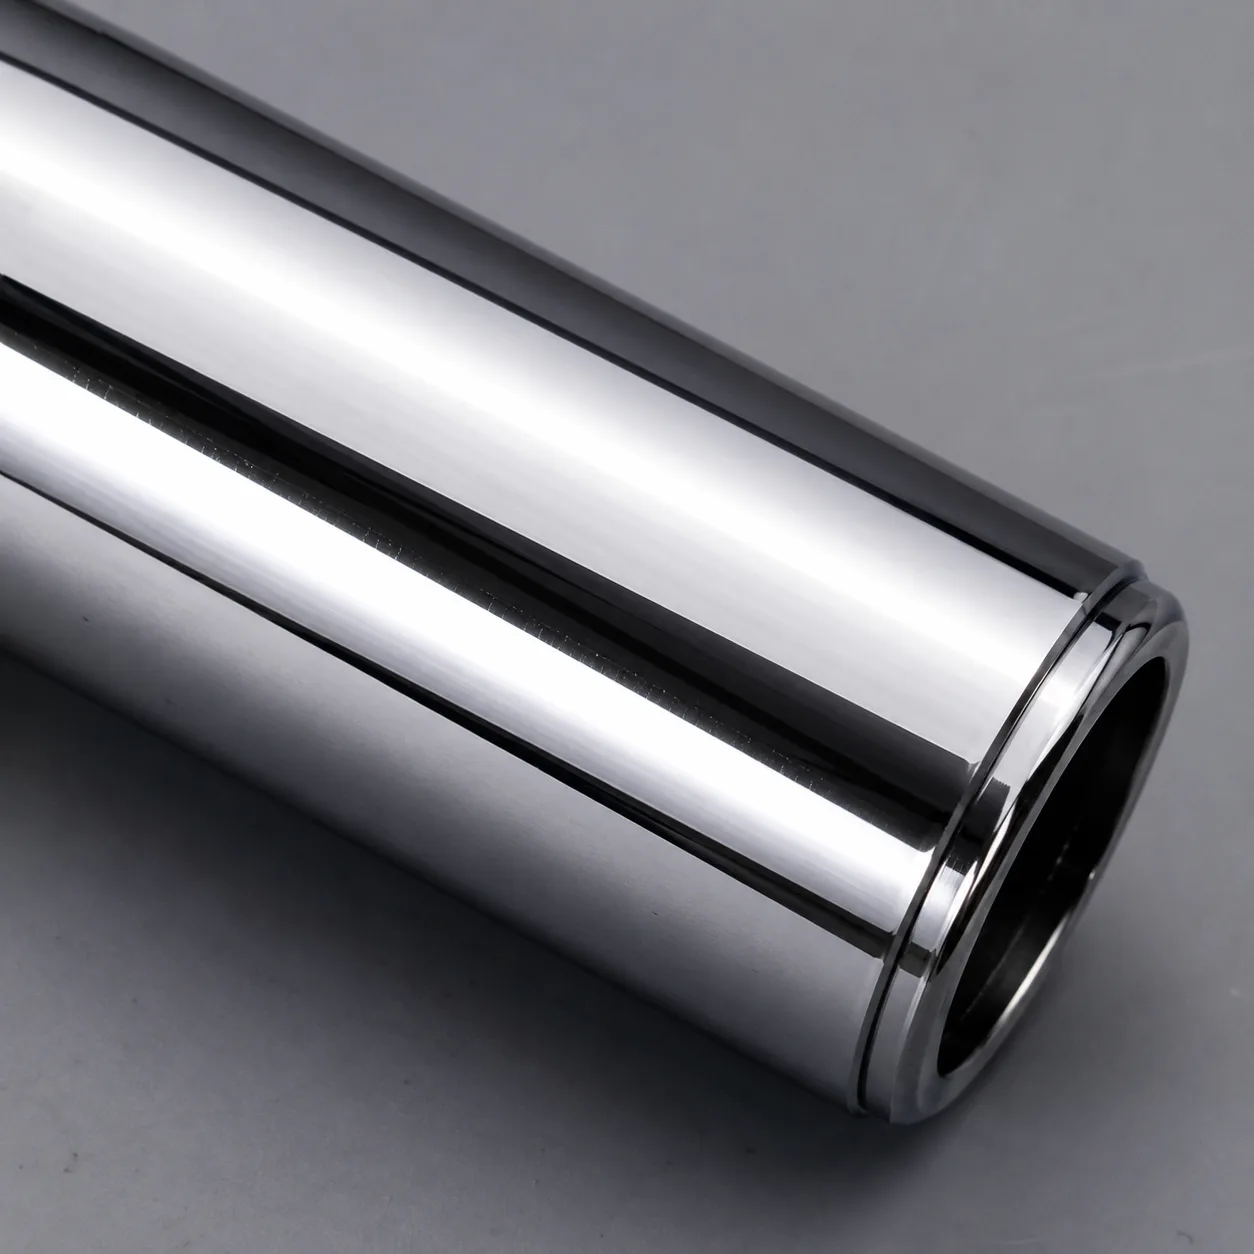 ElectroplatingZn · Ni · Cr · SnZinc first for corrosion, nickel for wear, tin for solderability.
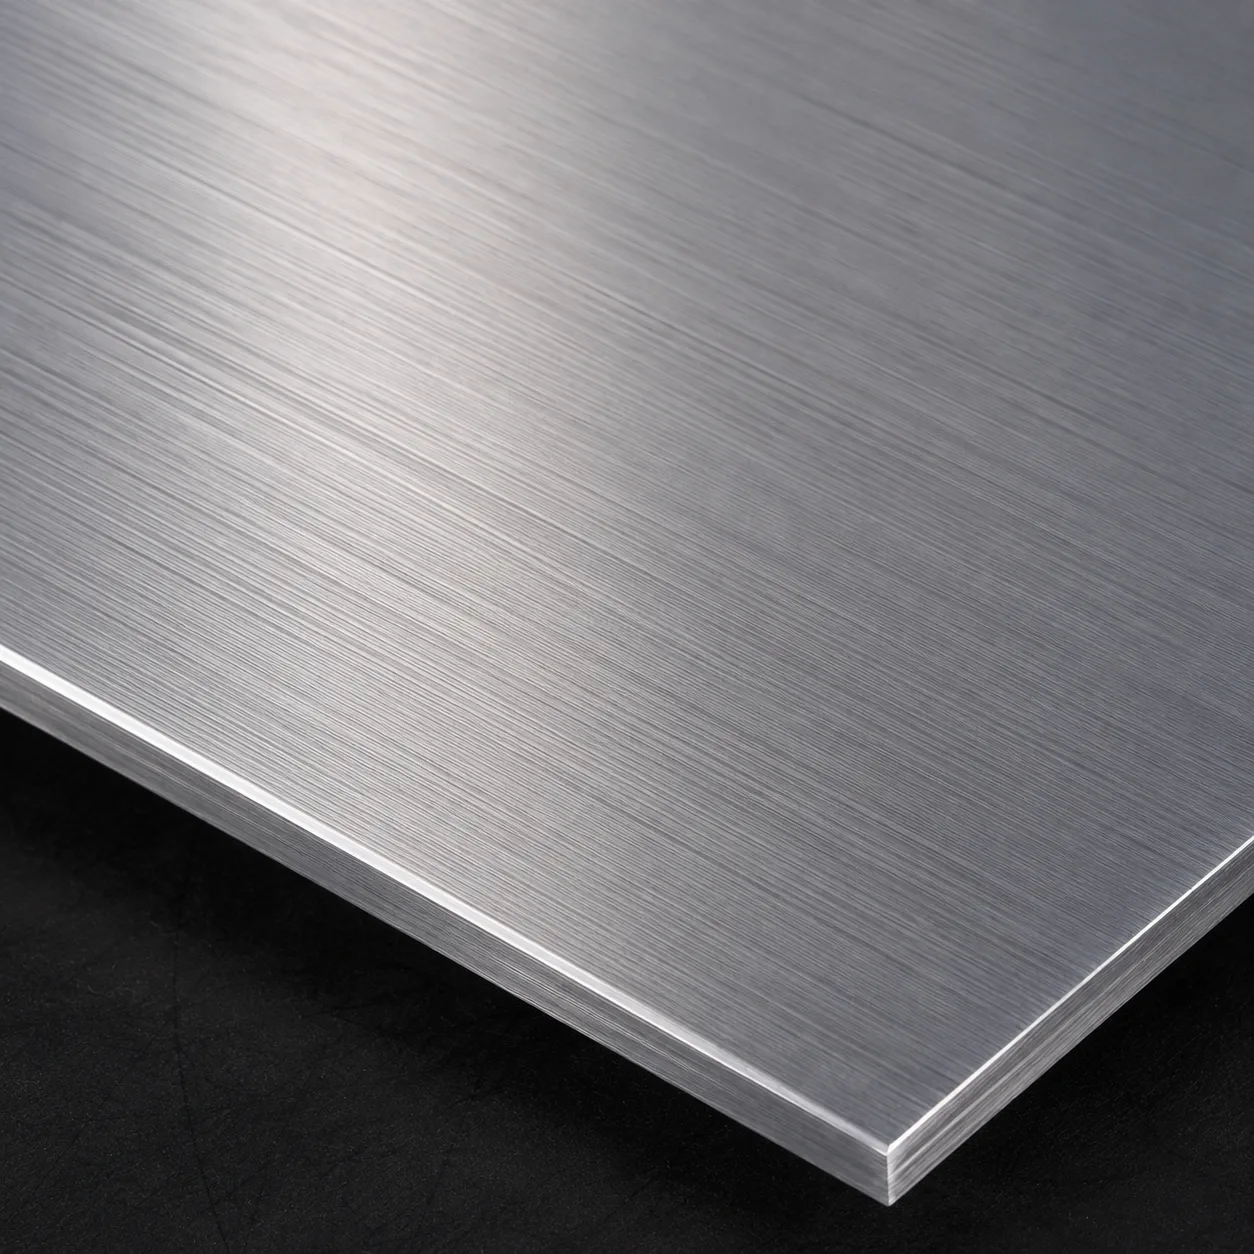 Brushed finish180–600 gritDirectional grain. Grain direction is a drawing callout, not a detail.
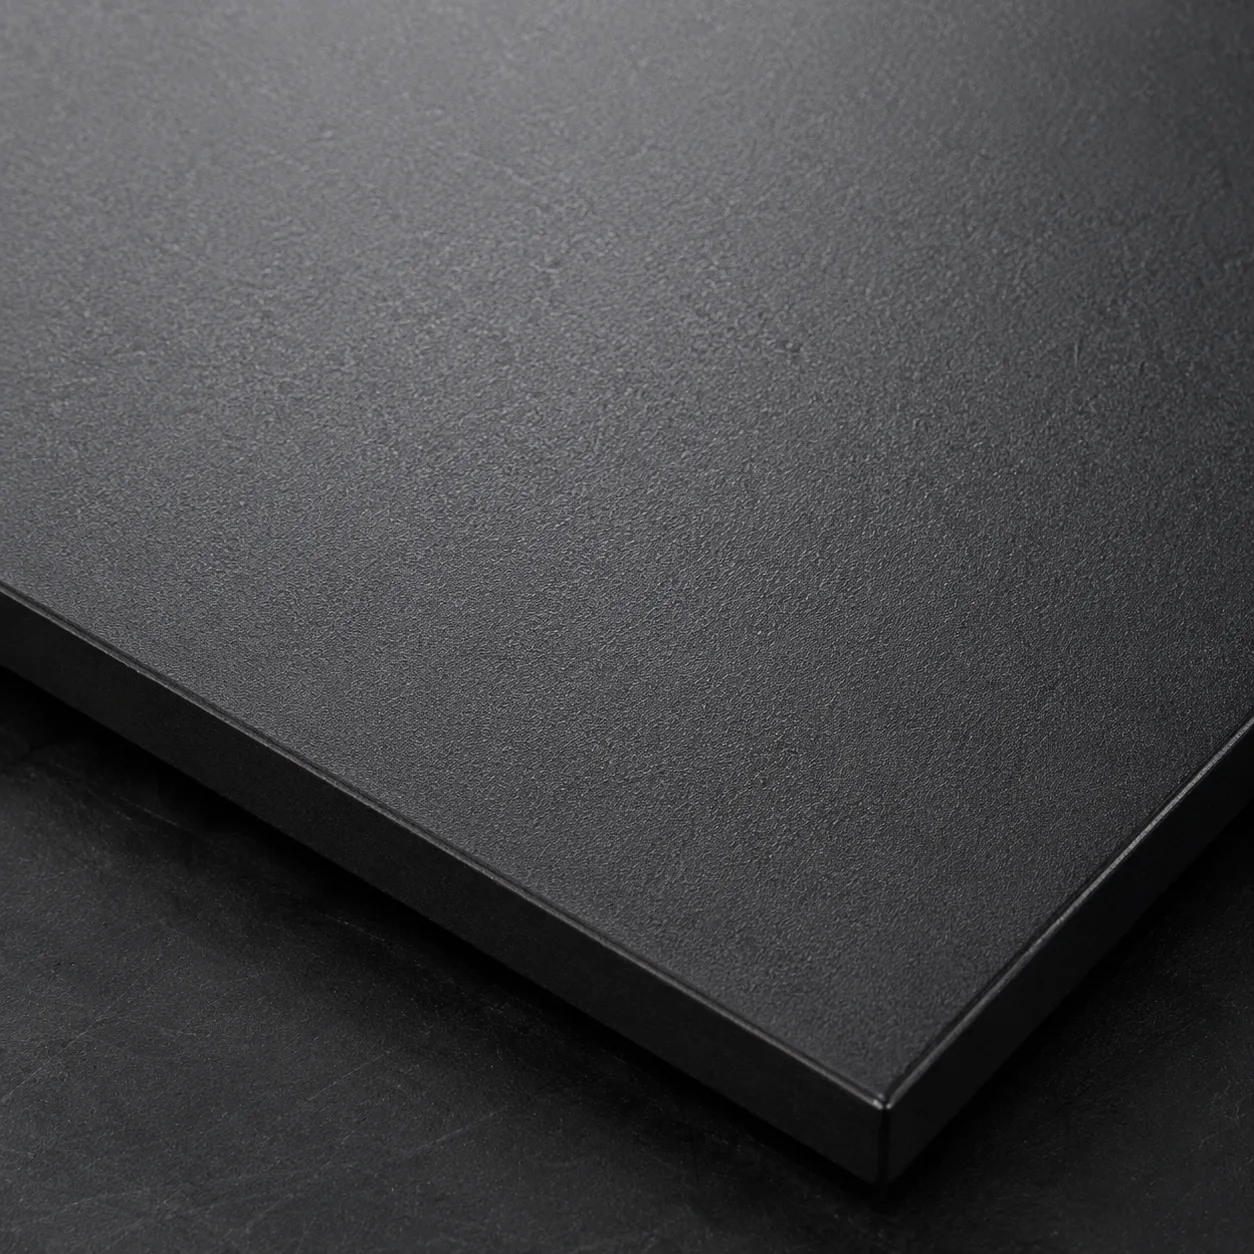 SandblastingGlass bead / oxideUniform matte key for paint, or the finished look itself.
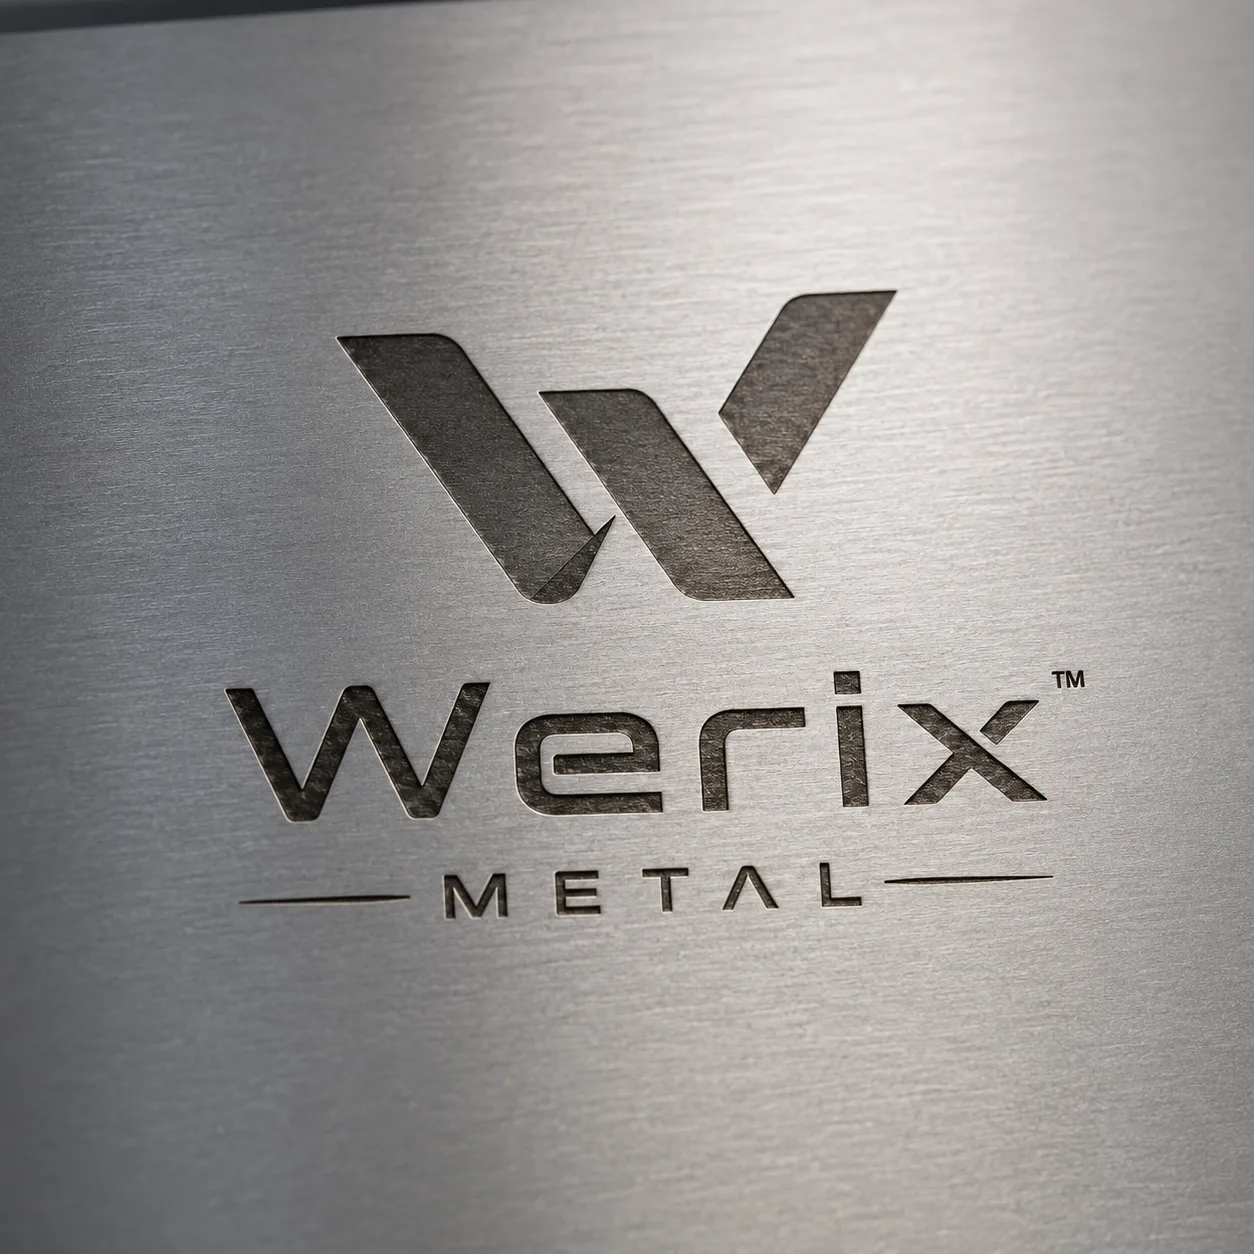 Laser engraving0.05 mm depthSerial numbers, wiring labels and QR codes, marked for the life of the part.
Also quoted on request: silk-screen and pad printing, electrophoretic coating, chemical passivation, chromate conversion and post-weld heat treatment.
Colour is the objection we hear most from overseas buyers. It gets the same answer every time: send a RAL or Pantone number plus a photograph of the part under your own lighting, and we spray a panel first and photograph it back before the batch runs.
Fabrication, stamping or CNC — pick by volume
Sheet metal fabrication wins below a few thousand pieces: there is no tooling to pay for. Progressive die stamping wins above it, because the die cost stops dominating and the unit price keeps falling. CNC machining is the third option when a part is thick, three-dimensional or threaded.
How many pieces are you ordering?
For your volume
Progressive die stamping
±0.01 mm/repeatable
- Economic volume
- 5,000 – 1,000,000+ pcs
- Tooling cost
- USD 3,000 – 40,000+ per die set
- Unit cost trend
- Falls sharply after break-even
- First part in hand
- 15 – 35 days including die build
- Design change after first part
- Modify or rebuild the die, days to weeks
- Material efficiency
- Best — strip nested edge to edge
- Wall thickness
- 0.2 – 6.0 mm strip
- Best suited shape
- Small to medium parts repeated
- Typical work
- Smaller parts repeated at volume, from a die built in our own die shop.
Metal stamping and die building→Low volume from 50 pieces→High volume stamping→
Not sure which side of the break-even you are on? Send the drawing and the annual volume — the recommendation comes back with the price.
What actually moves the price of a sheet metal part
Material and nesting yield
20%extra material cost
Sheet is bought by the sheet, not by the part. A design that nests badly across a 1,220 × 2,440 mm sheet can carry 20% more material cost than the same part nested well, before any machine time is added.
8 proven ways to cut sheet metal costs→Bend count and bend sequence
Every bend is a handling step, and direction matters as much as count. One setup and one gauge change is materially cheaper than three.
Over-specified tolerance
Calling ±0.05 mm on a profile that only needs ±0.2 mm buys inspection time, not machine time. It is the easiest cost to design out.
Surface finish and colour
Powder coating is priced per batch, per colour. Two RAL numbers on one order means two setup cycles — consolidating them is often a five-figure saving across a production year.
Volume and tooling amortisation
Fabrication prices are near-linear in quantity. Stamping prices are not: pass the break-even point and the unit price collapses and stays there.
How an order runs, from your file to your dock
Five steps, one engineer, and a written answer at each one. You always know which stage your order is in and who is holding it.
5 minutes, your side
Send the file
STEP, IGES, DXF, DWG, PDF or a photograph with dimensions — no account, no plugin, no sales call first. A physical sample works too if the original drawings are gone.
Upload a file for a free DFM review→Within 24 hours
Engineer review and quotation
A process engineer checks wall thickness, bend radii, hole-to-bend clearance and the process choice, then prices it against real machine rates. The DFM notes and the price arrive together, so both can be argued with.
What the DFM review covers→15 – 35 days
Tooling — stamping orders only
Die design, die build and trial run, all in our own die shop. You approve the first article off that die before it goes anywhere near production.
In-house die making→3 – 7 working days
Sample or first article
Fabricated parts ship in 3–7 working days with no tooling cost. Stamped parts go through first-article inspection with CMM data and a dimensional report against your drawing.
Rapid sheet metal prototyping→7 – 15 working days
Production, finish, assemble, ship
One purchase order covers cutting, forming, welding, finishing, hardware insertion, assembly and kitting. Parts leave as a finished unit, not a box of loose components waiting for your line.
Low volume and mass production→
How the parts get checked
Incoming material
Thickness, grade and surface condition checked against the mill certificate before the sheet is released to a machine.
In process
First-article check at each workstation — laser, bend, weld, press — then sampling through the run, not just at the end.
Dimensional
CMM and hand gauges against the drawing. Tight-tolerance and stamped parts get a written dimensional report.
Before dispatch
Finish, hardware, labelling and packaging checked, and the batch recorded so a query months later traces back to its run.
WERIX Metal is certified to the ISO 9001 quality management standard. First-article inspection reports, dimensional reports and transit-test results are available for any programme on request.
How would you like to start?
Chat instantly on WhatsApp, or send your files — we reply within 24 hours.
Chat on WhatsApp
Talk directly with an engineer — technical questions, pricing, NPI support. Fastest response.
Get a Quote Online
Describe your part, select material and quantity — our engineers will send a formal quote by email within 24 hours.
DFM & Quote by Email
Send 2D, 3D, PDF or image files — our engineers review your design and return a formal quote with DFM feedback within 24 hours.
Get a free quote via email, WhatsApp, or our online form — DFM review and engineering support included.
Two Paths, One Standard
Prototype or production. Same engineer, same factory, same quality standard, so nothing has to be re-qualified when volumes ramp.
Rapid Prototyping NPI
Upload your design, get a quote within 24 hours. Sample parts in 3–7 days.
Production NPI
The same engineer, the same factory — from first sample to mass production.
Why buyers choose the factory
Speed, transparency and one-stop execution, from first sample to mass production.
Fast Response, Real Engineers
Get instant pricing online. Our in-house engineers review every project and respond within 24 hours — no sales scripts, just real technical feedback.
Talk to an EngineerDirect Factory Sourcing
No middlemen, no broker markups. We are the actual manufacturer — get transparent, competitive pricing straight from our production floor.
Get a QuoteQuote & DFM Review
Upload DXF, DWG, STEP or PDF — our engineers review your design and return a quote with DFM feedback within 24 hours.
Get a QuoteOne-Stop Assembly
Hardware inserts, rivets, seals, silk-screening and full kitting — ship assembled, not in a box of parts.
Assembly ServicesPrototype with Us, Scale with Us
Same factory, same team, same quality standard from first sample to full production. No supplier switching, no quality surprises when volumes ramp.
NPI Solutions
Sheet metal engineering guides
Practical DFM, material selection, cost and sourcing guides from the process engineers on our shop floor.
Jun 26, 2026
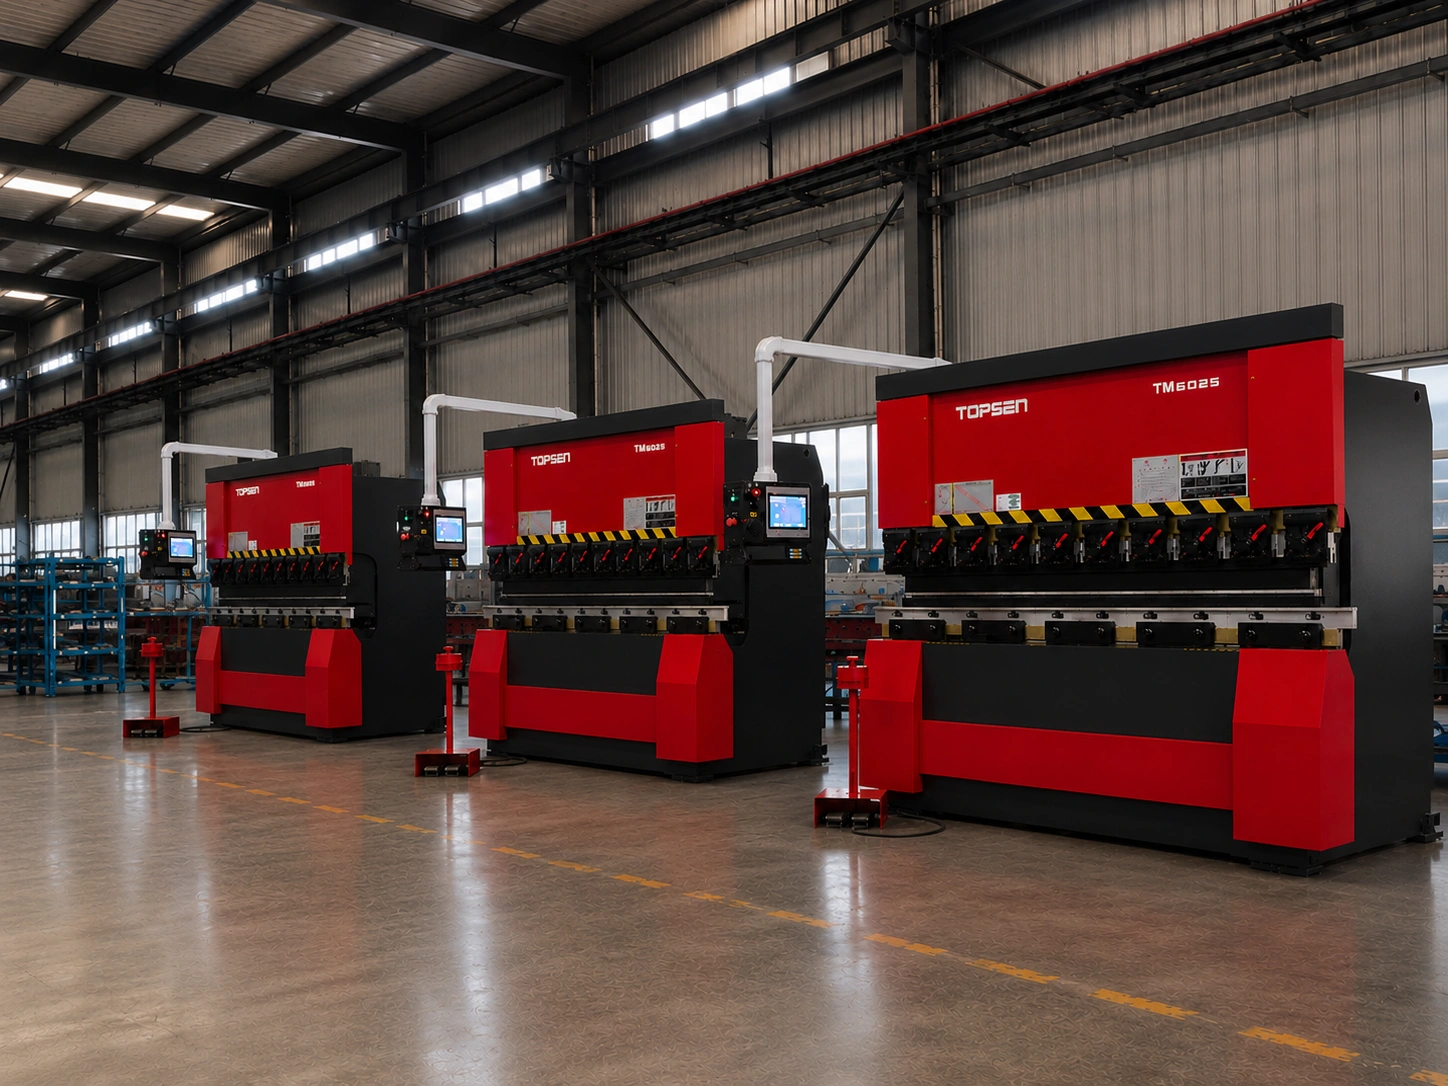
New CNC Press Brakes: Tighter Tolerances
New CNC press brakes with ±0.5° accuracy — what this means for your bending projects.
Mar 20, 2026
8 Proven Ways to Cut Sheet Metal Costs Without Sacrificing Quality
From bend radius optimization to material nesting — eight actionable design and sourcing strategies that reduce cost while maintaining part performance.
Sep 27, 2026
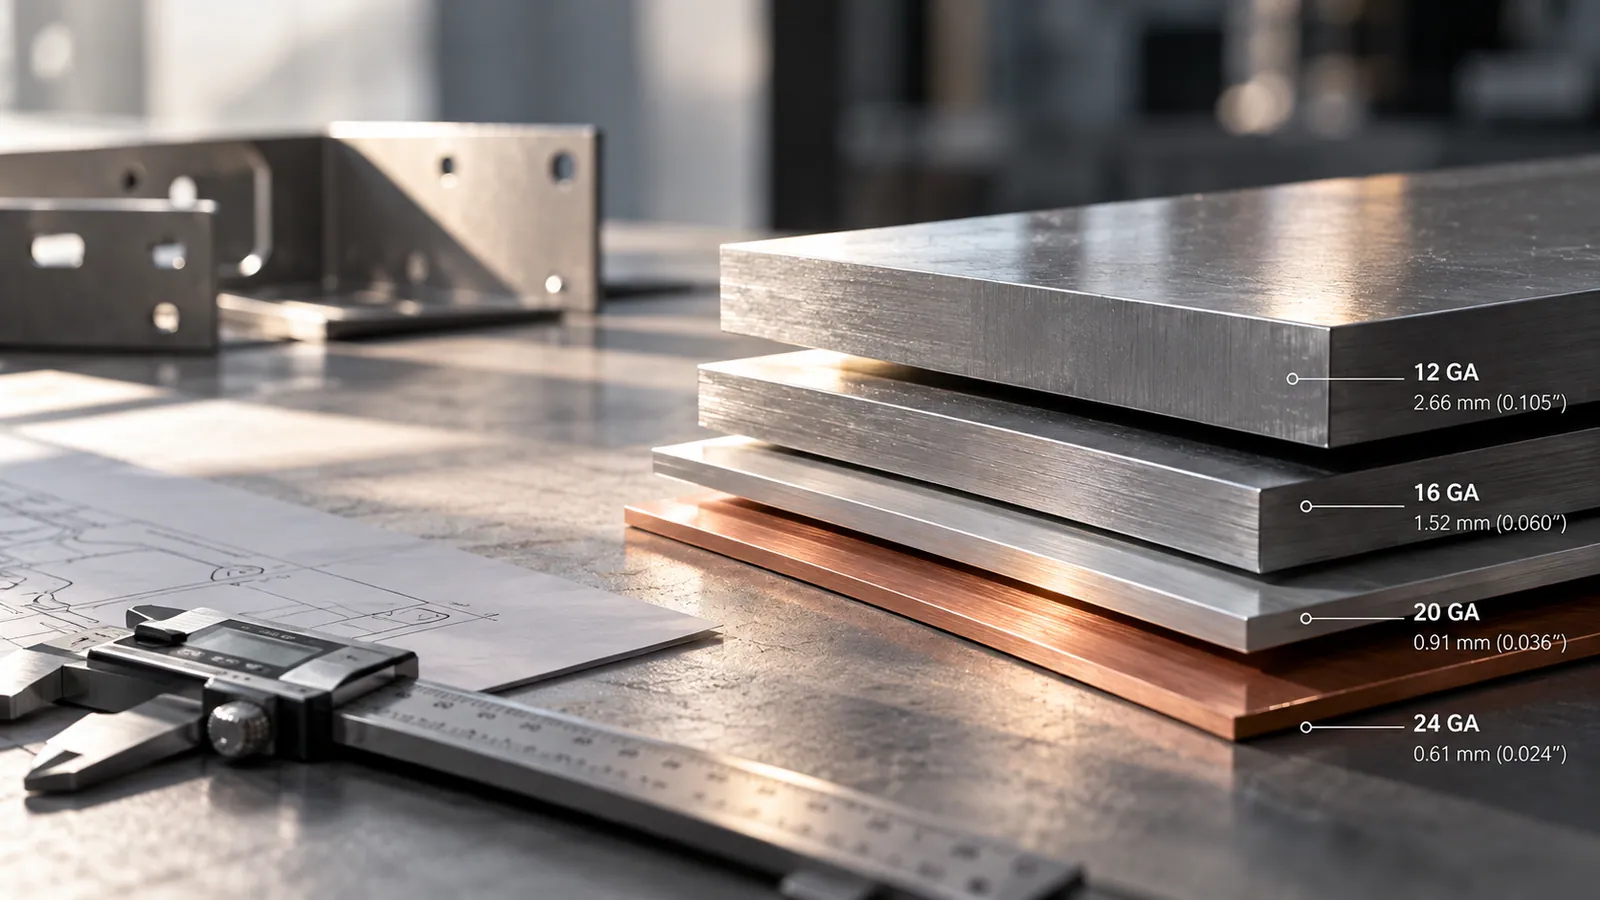
Sheet Metal Gauge Chart
A higher gauge number means a thinner sheet. The steel gauge-to-mm chart, why aluminum differs, and how to choose the right gauge.
Jul 3, 2026
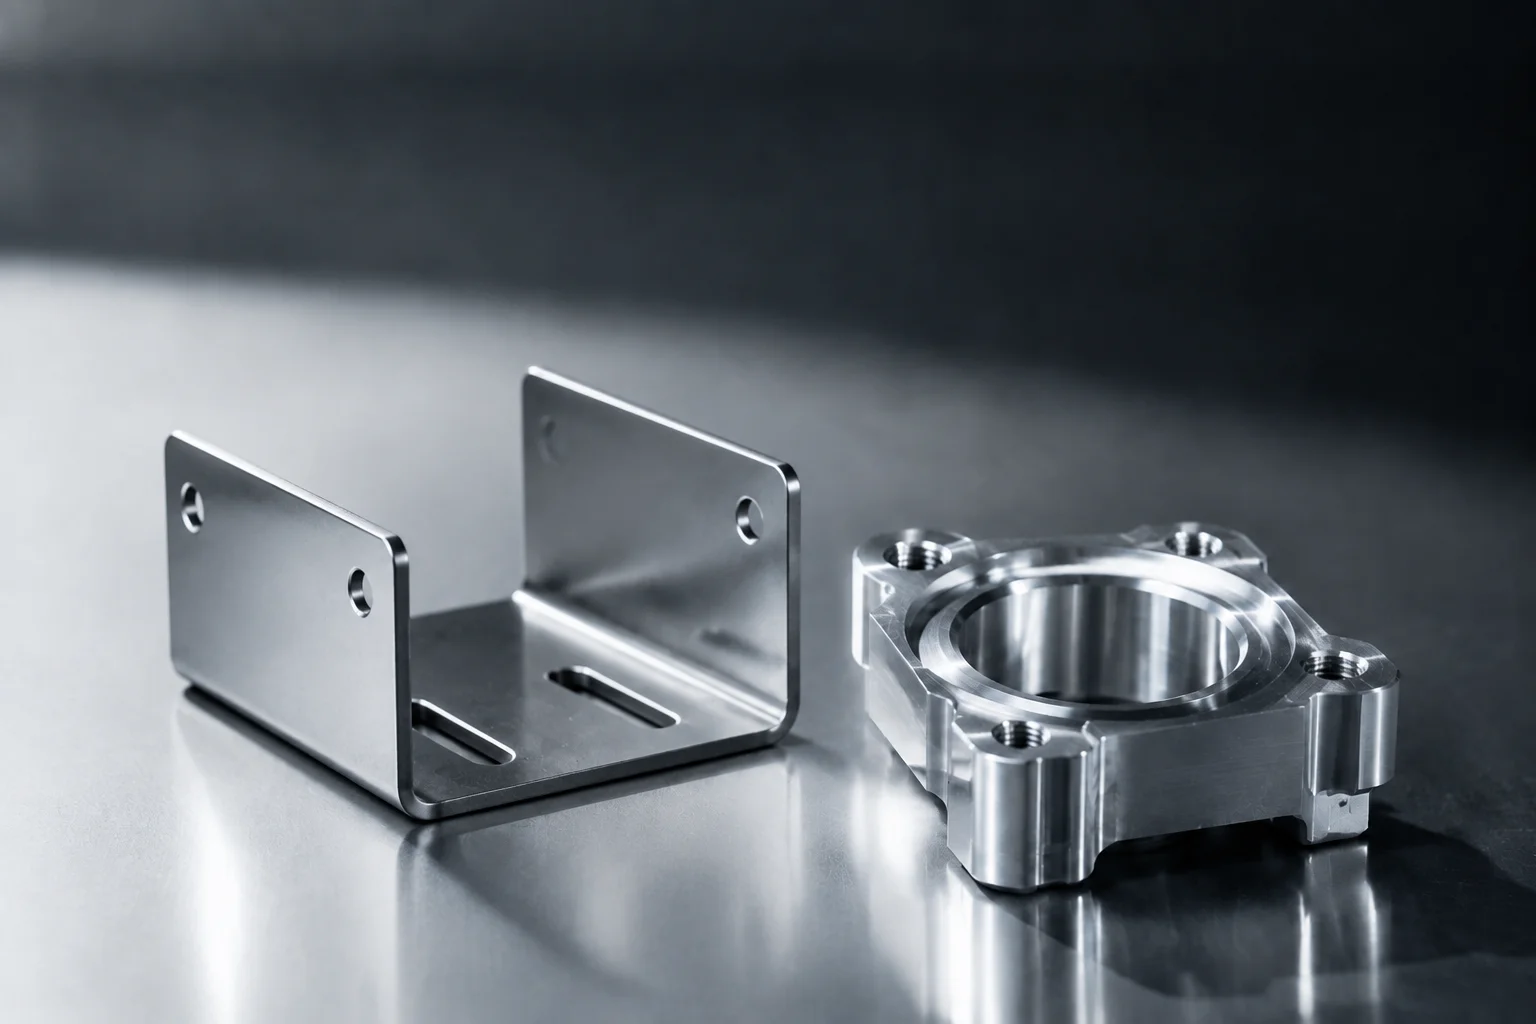
Sheet Metal Fabrication vs CNC Machining: How to Choose the Right Process
Sheet metal fabrication and CNC machining serve different geometries, volumes, and budgets. This data-backed comparison covers cost, tolerance, materials, and lead time.
All 21 engineering guides
Design and process
- DFM for sheet metal: essential design rulesBend radii, hole-to-bend clearance and the details that stop a design before production.
- Laser cutting vs CNC punchingContour complexity, edge quality and where each process stops being economic.
- Sheet metal fabrication vs CNC machiningHow to choose when the part could be made either way, and the geometry that decides it.
- Sheet metal material selectionSteel, aluminium, stainless, copper and brass compared on strength, corrosion and cost.
- 304 stainless vs 5052 aluminiumThe comparison most enclosure projects come down to, with bend and weight figures.
- 304 vs 316 stainless steelWhere the molybdenum premium actually pays — chlorides and coastal sites — and where 304 does the same job for less.
- 5052 vs 6061 aluminiumWhy bendability, not datasheet strength, decides the alloy for folded parts — and when 6061-T6 is worth the cracking risk.
Cost and sourcing
- 8 proven ways to cut sheet metal costsMaterial waste, over-tolerancing and process selection — what each one is worth in money.
- How sheet metal quoting worksA line-by-line breakdown of a price, so you can read a quotation properly.
- How to source sheet metal parts from ChinaQualifying a factory, verifying capability, and the questions that expose a broker.
- WERIX vs online manufacturing platformsHow platform markup, routing and quality ownership compare with a single source factory.
Inside this factory
- From upload to deliveryWhat happens to your files and your parts between the enquiry and the container.
- What "source factory" actually meansEquipment ownership, outsourcing, and why the distinction changes your price and your risk.
- Source factory vs broker platformThe business model behind a quotation determines your real cost and lead time.
- How WERIX uses AI in quotingWhat the quote engine does with eleven years of production data, and what still needs an engineer.
- New CNC press brakes installed3,100 mm bed, ±0.02 mm ram positioning — and what the tighter tolerance unlocks for your parts.
Reference and finishes
- Sheet metal gauge chartGauge to mm for steel, stainless and aluminium — and why one gauge number means three thicknesses.
- Minimum bend radius chartThe tightest radius each material and thickness will take before the flange cracks.
- Sheet metal weight calculatorThe formula, a density table, and what your blank weighs before freight enters the price.
- Powder coating vs anodizingA coating built on top of the metal versus a converted surface — cost, durability and failure modes.
- Zinc plating vs nickel platingSacrificial protection for a few cents versus a harder, brighter finish — how to choose.
The 2026 company brochure
No form, no email address, no gate.
Ready to Start Your Project?
Get a Quote — or Talk to an Engineer.
Send drawings, get a DFM review and a price within 24 hours — no account required, and orders start from a single prototype.