Table of Contents
Overview
Quick answer: 5052-H32 is the default sheet-metal aluminium — it bends tight, welds well and resists salt water, so enclosures, brackets and marine parts use it. 6061-T6 is the structural and machined-part alloy: about twice the yield strength and great for CNC features, but it cracks during sharp bending. Formed parts default to 5052; machined parts default to 6061.
What do the alloy numbers mean?
The four digits describe the alloy family; the temper suffix describes its final condition. Both 5052 and 6061 are alloyed with magnesium, but 6061 adds silicon, copper and chromium — a recipe that heat-treats to much higher strength. 5052 is a work-hardening alloy: it gets its strength from cold rolling, and the common sheet temper H32 means strain-hardened then stabilised. 6061 is a heat-treatable alloy: the T6 temper means solution-treated and artificially aged, which is where its strength comes from.
That single difference drives almost everything downstream. A work-hardening alloy bends without losing its properties; a heat-treated alloy is at its strongest exactly when you try to form it, which is where the trouble starts.
Forming: The Bending Difference
This is where the two alloys separate for good. 5052-H32 bends cleanly across the full thickness range we run — parts fold with inside radii at or near one material thickness without cracking, and the formed flange keeps its strength. 6061-T6 is a different story: bend it across the grain at a tight radius and it tears along the bend line, sometimes hours later. The classic shop rule is to bend 6061 only at generous radii, perpendicular to the grain — or buy it in the T4 condition, form it, then age it to T6, which is rarely practical for outsourced sheet work.
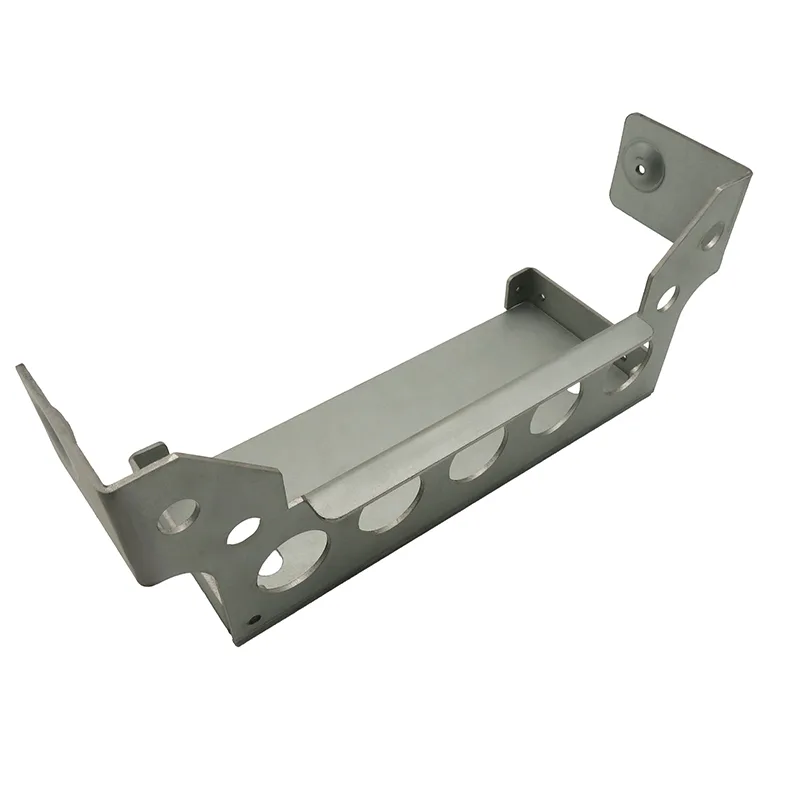
For a fabricated enclosure, bracket or panel — anything with bends — 5052 is the alloy. 6061 sheet exists in fabrication mostly as flat blanks waiting for CNC features, not as formed parts. If your supplier quotes 6061 for a multi-bend sheet metal part without comment, ask about the bend radii in writing.
How do strength, corrosion and cost compare?
6061-T6 wins the numbers game decisively: its yield strength is roughly double that of 5052-H32, and its tensile strength is about 40% higher. If the part is a structural member carrying real load, that margin matters. But numbers are not the whole story — corrosion behaviour and formability often decide the part long before strength does.
| Property (typical reference) | 5052-H32 | 6061-T6 |
|---|---|---|
| Yield strength | ~193 MPa | ~276 MPa |
| Tensile strength | ~228 MPa | ~310 MPa |
| Tight bending (1T radius) | Excellent — the default choice | Poor — cracks at sharp radii |
| Salt-water corrosion | Excellent — marine grade | Good, less suited to marine duty |
| Welding | Good, retains most strength | Weldable, loses ~40% strength at weld |
| CNC machining | Gummy, adequate | Excellent — the machinist's alloy |
| Typical sheet use | Enclosures, brackets, panels, marine | Flat machined plates, structural fittings |
Values are typical reference figures for common tempers; exact properties depend on thickness and certifiable mill data. On price, the two usually land within a modest band of each other at sheet gauges — the process consequences (bending, welding, finishing) move the total cost far more than the raw material does.
Welding, Machining and Finishing
Welding splits the pair in an under-appreciated way. 5052 welds readily and keeps most of its strength across the joint. 6061 also welds, but the heat-affected zone drops to roughly T4-level strength — a real design consideration on load-bearing weldments, and the reason post-weld heat treatment exists for critical 6061 structures. On fabricated assemblies that mix both, we plan the welds around the 6061's softened zones rather than pretending they are not there.
Machining is 6061's home turf: it cuts clean, holds tolerance and finishes beautifully, which is why CNC-machined mounting plates and fittings use it. 5052 machines gummier but entirely adequately for the drilled and tapped features typical on enclosures. Both anodize well with slightly different film tone — the practical notes are on each alloy's material page, and colour-critical multi-part builds should agree a sample panel at quotation.
How do you choose?
The decision tree is short. Enclosure, bracket, panel or any part with bends → 5052-H32, every time. Marine or salt-exposed hardware → 5052. Machined plate, structural fitting or heavily loaded bracket → 6061-T6. Part that bends and carries serious load → usually 5052 with a thicker gauge, because the formed 6061 alternative risks the bend line; when the load truly demands 6061, the part becomes a machined fitting, not a bent sheet part.
When customers send both options for quote, the price difference is rarely the deciding factor — the bend behaviour is. A cracked first article costs more than any alloy premium. Describe the load and the environment, and the quotation names the alloy we would run, with the reasoning on paper.
FAQ
Written by
Industrial & Product Design Engineer
Julia takes a product from the first sketch to a sheet metal design that can actually be made. She sits between the customer’s concept and our press brakes — modelling enclosures and brackets in CAD, running early DFM passes, and choosing the material and finish that will still look right two years down the line.
View profileParts we make for this topic
Ready to Start Your Project?
Get DFM feedback and a quote within 24 hours. No minimum order quantity.