
Laser Cutting vs Stamping: Finding the Break-Even
A calculation you can run on your own part, with the inputs stated. It also covers the three cases where the arithmetic says yes and the answer should still be no.
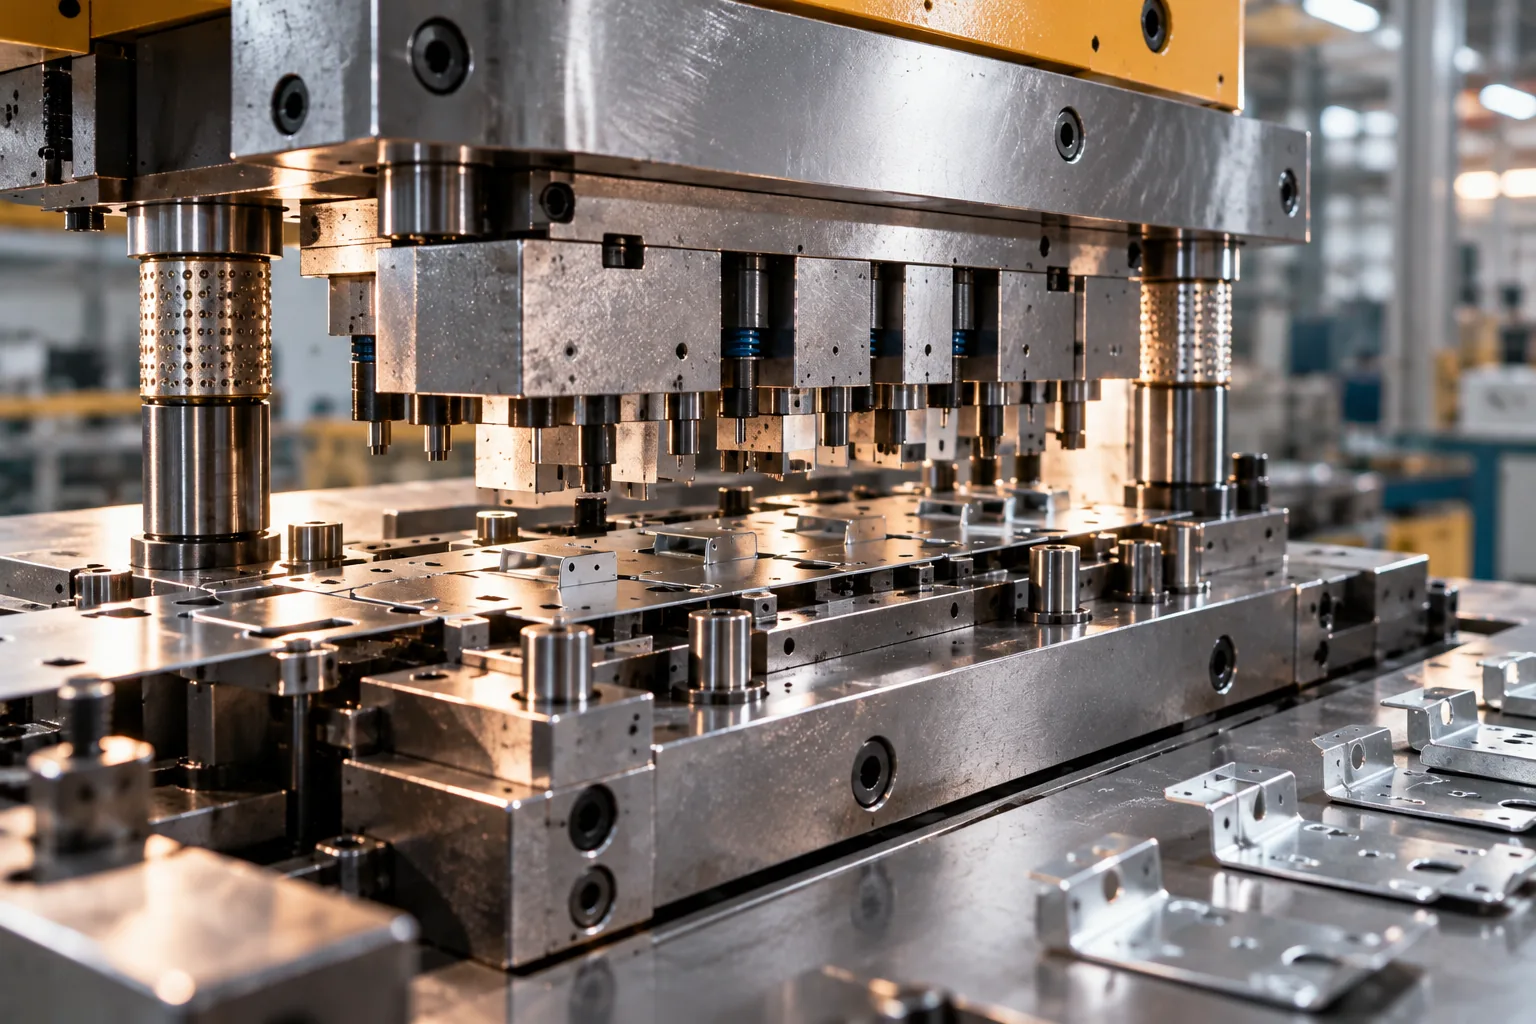
Break-even volume is tooling cost divided by the per-part saving of stamping over laser cutting and bending. It is not a fixed number of parts: a bracket with many holes and formed features saves far more per piece than a plain plate, so it pays back far sooner. Below break-even, stamping is the expensive route.
The calculation
Let D be the one-off tooling cost and S the saving per part of the stamping route over laser cutting and bending. Break-even occurs at D ÷ S parts. Below that volume the tooling has not paid for itself; above it, every additional part is cheaper than the laser route would have been.
The difficulty is not the division, it is estimating S. On the laser route, each part carries a share of programming, cutting time, handling between operations and often a manual deburr. On the stamped route, one stroke delivers a finished part with the deburr moved to a batch tumble. The saving per part is the difference between those two, and it grows with feature count, not part size.
Read the table below as a ratio rather than as money. A part with many pierced holes and several formed features pays back at a fraction of the volume a plain plate needs: break-even is decided by feature density, not by part size or annual spend.
- Small (plain plate, few features)
- 50,000 · 100,000 · 200,000
- Moderate (several holes, one or two forms)
- 25,000 · 50,000 · 100,000
- Large (many holes, multiple formed features)
- 12,500 · 25,000 · 50,000
What the calculation leaves out
Cycle time sets a second constraint. A progressive die runs at a press rate, so above break-even the die capacity becomes the limit rather than the cost. Where demand spikes beyond die capacity, the extra volume still goes somewhere else — which is a schedule question, and worth planning for rather than discovering.
Material utilisation differs between the routes too. A strip layout and a nest consume different fractions of a sheet for the same part, and on a part with an awkward outline the die can be the less efficient user of material even while it is cheaper in labour.
Three cases where the answer is no
- The design is not frozen. Every revision after the die is cut is a die modification, and the strip layout cannot be revised economically at all.
- Volume is real but short-lived. A programme that ends in two years may never reach break-even, however good the arithmetic looks on an annual figure.
- The part changes per customer configuration. Unless the common features can live in a common die and the differences be handled by a secondary operation, tooling the variant is tooling a moving target.
Running it on your part
We need the drawing, an annual volume, the expected programme life, and a view on whether the design is final. From that we produce both routes costed the same way, and the payback volume. Where the answer is marginal, that is worth saying plainly rather than tuning the numbers to reach a decision — a die that never pays back is worse than a laser part that costs slightly more per piece.
Frequently asked questions
How many parts justify a stamping die?
It is tooling cost divided by the saving per part, so there is no universal number. A bracket with many features can pay back in the low tens of thousands; a plain plate may never pay back. The lever is feature density, not part size.
Does a die always reduce the part price?
No. It reduces the per-part price at volume, because one stroke replaces cutting, handling and often a manual deburr. Below break-even the tooling makes the part more expensive, and that is the common case for low-volume or short-life programmes.
What happens if the design changes after tooling?
Some changes are affordable — adding a station, adjusting a form, revising a trim. Changes that move the strip layout generally are not, because they are built into the die blocks and the feed. Freezing the design before tooling is the single most effective protection for the investment.
Can both routes be used for the same part?
Yes, and it is often the right answer. Prototype and early production on the laser route, then a die once the design is frozen and volume is established. What matters is that the flat pattern is consistent between the two so the parts are interchangeable.
Does the die capacity limit volume?
It can above break-even, particularly on a single press. Where demand exceeds the die rate, the excess has to be produced another way, or a second die is needed. That is worth modelling alongside the cost, especially on a part with a seasonal or campaign-driven demand pattern.
Send the drawing, get a real answer
An engineer reviews your model for manufacturability and returns a costed quotation — with the DFM observations that would change the price.