
ATM Enclosure & Cash Machine Housing — Tamper Resistant
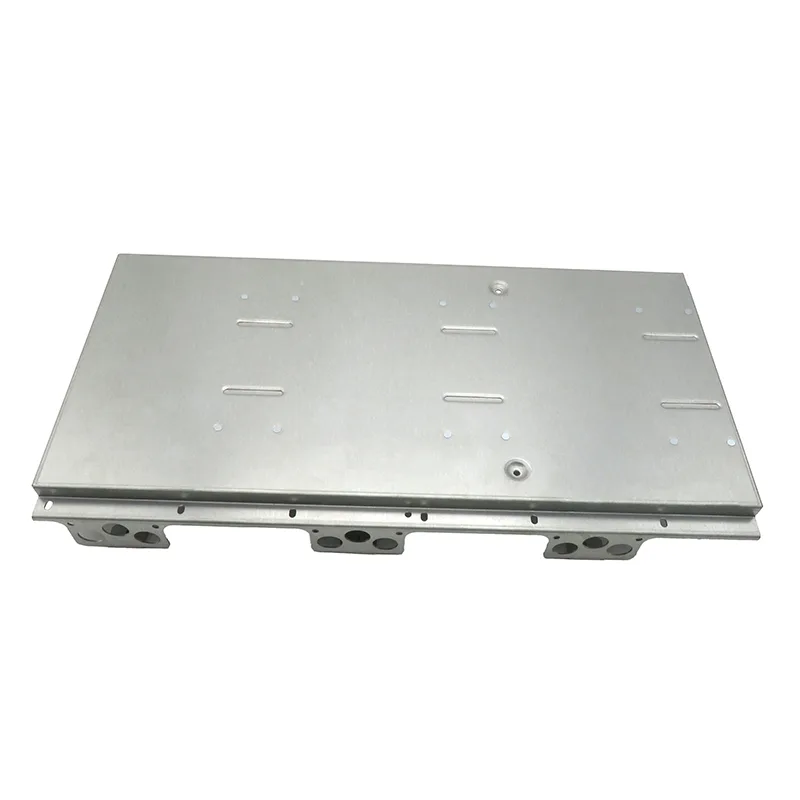
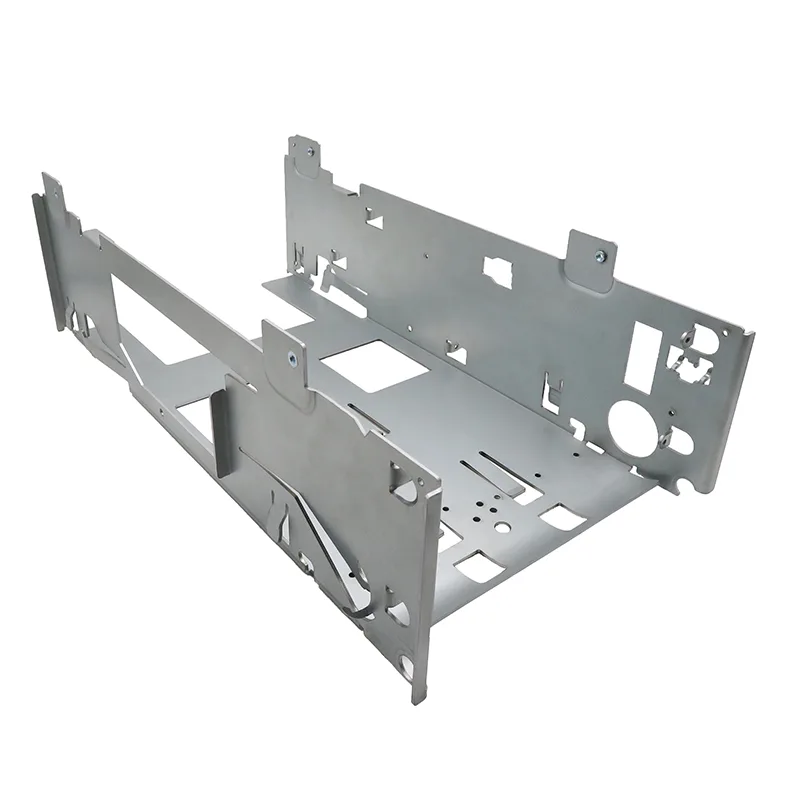
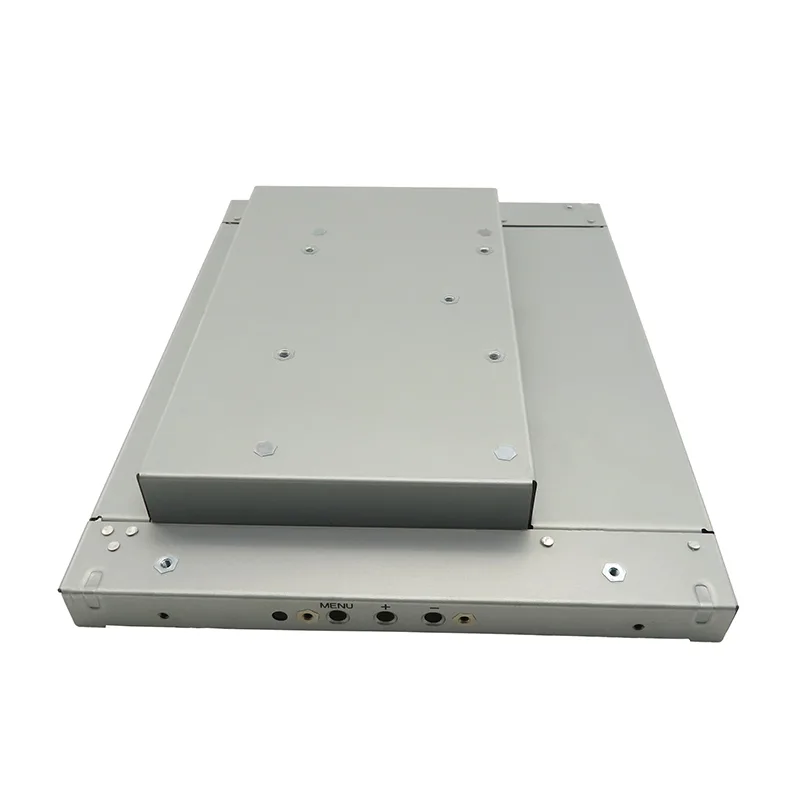
ATM surround and cash machine housing built for public 24/7 use: 2–3 mm steel, reinforced door frames, anti-pry flanges around the note dispenser, concealed hinge pins and a bolted floor frame so the machine cannot be walked out of the lobby. Made by WERIX Metal from SPCC 2.0-3.0mm / SUS304 1.5mm to a tolerance of ±0.1mm, finished with powder coat + anti-tamper features. Typical order volume is from 1 to 1000+. Free DFM quote within 24 hours.
Engineering drawing available on request
Send your target specifications — we reply with a drawing and a DFM quote within 24 hours.
ATM Enclosure & Cash Machine Housing — Tamper Resistant
ATM surround and cash machine housing built for public 24/7 use: 2–3 mm steel, reinforced door frames, anti-pry flanges around the note dispenser, concealed hinge pins and a bolted floor frame so the machine cannot be walked out of the lobby.
| Part number | P-089 |
|---|---|
| Product type | ATM Enclosure |
| Industry | Banking & Financial |
| Material | SPCC 2.0-3.0mm / SUS304 1.5mm |
| Tolerance | ±0.1mm |
| Surface Finish | powder coat + anti-tamper features |
| Manufacturing processes | laser cutting · CNC bending · MIG welding |
| MOQ / Volume | from 1 to 1000+ |
ATM Enclosure & Cash Machine Housing — Tamper Resistant: manufacturing notes
This part — atm enclosure & cash machine housing — tamper resistant — is manufactured in our Dongguan plant. The notes below explain the manufacturing decisions behind the specification: why this material, why this forming sequence, and what the tolerance actually requires in production.
Why this part is made in stainless steel
ATM Enclosure & Cash Machine Housing — Tamper Resistant is specified in SPCC 2.0-3.0mm / SUS304 1.5mm. Stainless is specified for corrosion resistance and for appearance in one move: the surface is the corrosion protection, so a scratch is a maintenance question rather than a rust path. It work-hardens as it is formed, which raises the bend force and pushes springback up, so bend radii on stainless are kept larger than on mild steel and the tooling is set for the higher force.
How the part is formed
The production route for this part is laser cutting, CNC bending, MIG welding. Fiber laser cutting separates the blank without hard tooling, which is what makes a first article economical: the profile can change between the prototype and the production run without a die sunk. The trade-off is a small heat-affected edge, so on parts that will be painted we deburr and, where the edge is a sealing face, dress it flat before coating. Bending is where most tolerance stack enters a sheet metal part. We set the bend allowance from the part’s own material and radius using the K-factor the press is running, then verify the first article on the machine rather than from the drawing, because springback moves with material batch and grain direction.
What ±0.1mm actually requires on the shop floor
The drawing calls for ±0.1mm. On a part like this that is a process decision, not an inspection decision: it fixes which machine holds the critical features, how the part is fixtured for each operation, and whether a formed feature can be checked after coating or has to be measured before it. We confirm the first article against the drawing and record the values, so the tolerance is demonstrated rather than assumed. If a dimension in your drawing is tighter than this part needs, it is usually worth relaxing it — over-toleranced features are one of the quietest cost drivers in a sheet metal quote.
Finishing: powder coating
powder coat + anti-tamper features. Powder coating builds a film of roughly 60–120 µm per face and cures at 180–200 °C. Two consequences get designed for: the film adds to every mating dimension, and the cure temperature is high enough to move an unsupported panel, so stiffening or return flanges go in before the part reaches the oven. Colour is matched to the RAL range given on the drawing.
Frequently asked questions
- What is the minimum order quantity for atm enclosure & cash machine housing — tamper resistant?
- The order range for this part is from 1 to 1000+. Below the low end of that range the tooling and setup are spread over too few pieces to be economic, so if you are prototyping we would normally build the first units from the same process route and quote the production quantity separately.
- Can the material be changed to reduce cost or weight?
- Yes, and it is worth asking before the design is frozen. The current specification for this part is SPCC 2.0-3.0mm / SUS304 1.5mm; depending on the service environment, a different grade or a lighter gauge with formed stiffening can meet the same requirement. What we would not do is change the material without re-checking the bend radii, the welding process and the coating system, because all three move with the substrate.
- What finishing options are available for this part?
- The current finish specification is powder coat + anti-tamper features. Powder coating, anodising, zinc or nickel plating, brushing and blasting are all available in-house, so the finish can be changed without changing supplier — and where the part will be seen, we match colour to the RAL or Pantone reference on your drawing.
- How long does production take, and what do you need from us to quote?
- Prototypes are typically 3–7 business days and production runs 7–15 days once the drawing is released and the finish is confirmed. To quote we need the drawing or CAD file (STEP, DXF, DWG, IGES or PDF), the material and finish, the quantity and the destination — and any tolerance or inspection requirement that is not already on the drawing. You get a DFM review with the quotation, not after it.
Sheet metal engineering guides
 Zinc Plating vs Nickel PlatingZinc protects steel even when scratched, for cents. Nickel is harder and brighter but 3-5x the cost. The finish decision, in one table.Read More
 8 Proven Ways to Cut Sheet Metal Costs Without Sacrificing QualityFrom bend radius optimization to material nesting — eight actionable design and sourcing strategies that reduce cost while maintaining part performance.Read More