
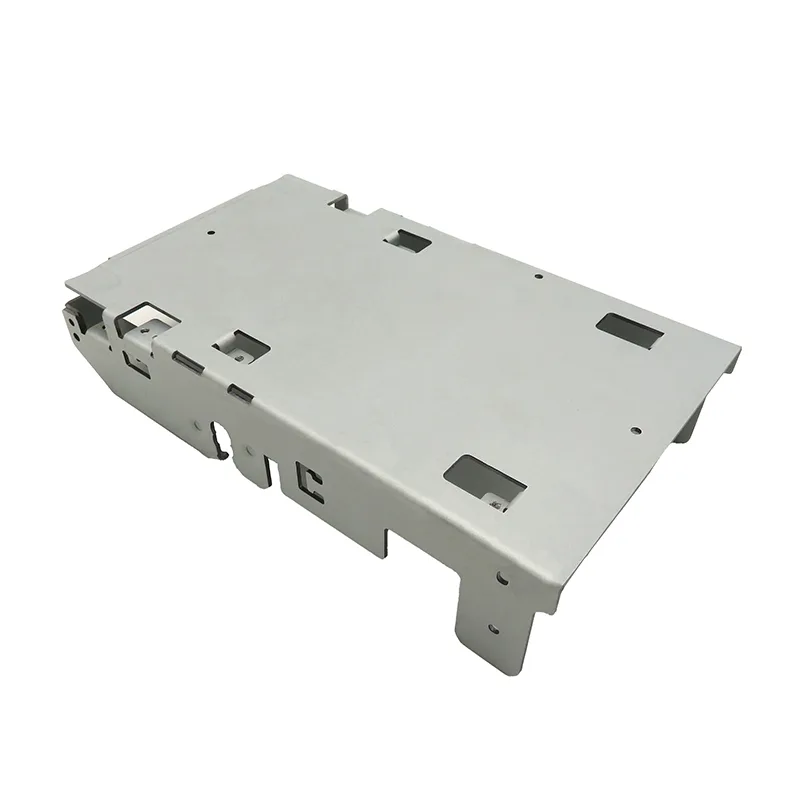
Internal Component Bracket
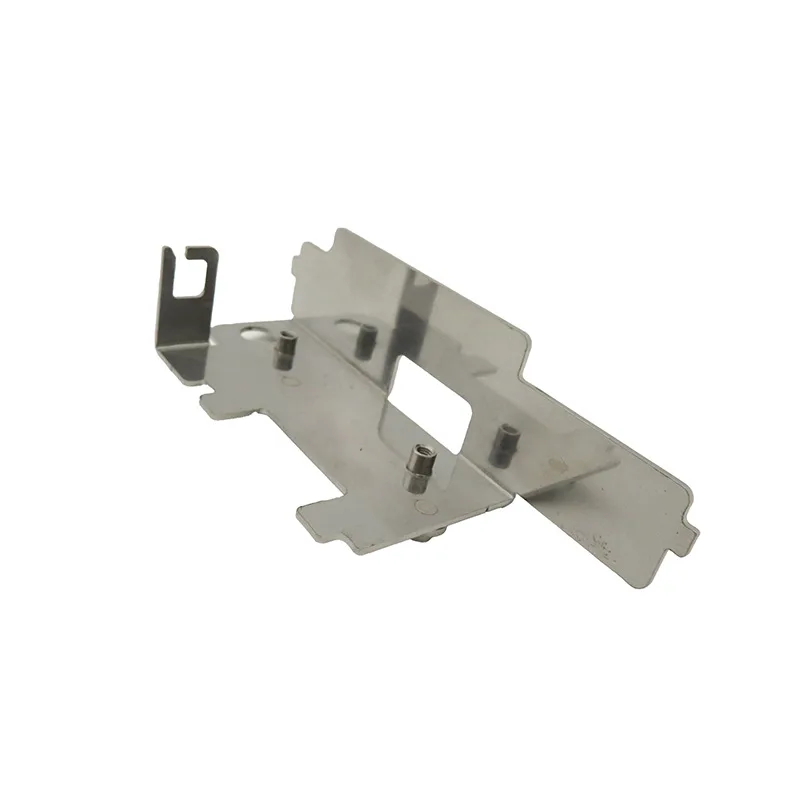
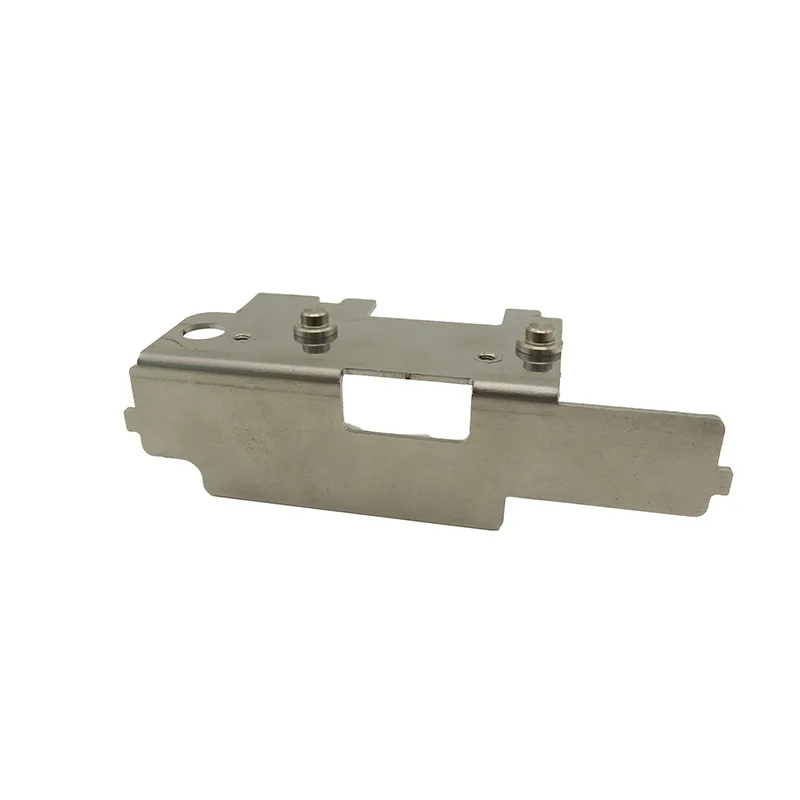
Small precision-stamped stainless steel bracket with PEM insert standoffs. Complex multi-bend geometry for internal component mounting. Made by WERIX Metal from SUS304 stainless steel 0.5mm to a tolerance of ±0.1mm, finished with Passivation. Typical order volume is From 5,000 to 500,000+. Free DFM quote within 24 hours.
Internal Component Bracket
Small precision-stamped stainless steel bracket with PEM insert standoffs. Complex multi-bend geometry for internal component mounting.
| Part number | G-022 |
|---|---|
| Product type | Bracket |
| Industry | Consumer Electronics |
| Material | SUS304 stainless steel 0.5mm |
| Tolerance | ±0.1mm |
| Surface Finish | Passivation |
| Manufacturing processes | Precision Progressive Die Stamping |
| MOQ / Volume | From 5,000 to 500,000+ |
Internal Component Bracket: manufacturing notes
Internal Component Bracket has to survive its application, not just its inspection report. This page sets out how the part is actually made — the material decision, the forming sequence and the tolerance strategy — so a buyer or engineer can judge whether the specification matches the application before a drawing is even sent.
Why this part is made in stainless steel
Internal Component Bracket is specified in SUS304 stainless steel 0.5mm. Stainless is specified for corrosion resistance and for appearance in one move: the surface is the corrosion protection, so a scratch is a maintenance question rather than a rust path. It work-hardens as it is formed, which raises the bend force and pushes springback up, so bend radii on stainless are kept larger than on mild steel and the tooling is set for the higher force.
How the part is formed
The production route for this part is Precision Progressive Die Stamping. Stamping moves the cost from the labour line to a hardened die, which pays off from a few thousand pieces upward: cycle time stops being a labour cost and becomes machine time, and every subsequent part inherits the die’s tolerances instead of the operator’s. Below that volume the same geometry is normally lasered and formed.
What ±0.1mm actually requires on the shop floor
The drawing calls for ±0.1mm. On a part like this that is a process decision, not an inspection decision: it fixes which machine holds the critical features, how the part is fixtured for each operation, and whether a formed feature can be checked after coating or has to be measured before it. We confirm the first article against the drawing and record the values, so the tolerance is demonstrated rather than assumed. If a dimension in your drawing is tighter than this part needs, it is usually worth relaxing it — over-toleranced features are one of the quietest cost drivers in a sheet metal quote.
Frequently asked questions
- What is the minimum order quantity for internal component bracket?
- The order range for this part is From 5,000 to 500,000+. Below the low end of that range the tooling and setup are spread over too few pieces to be economic, so if you are prototyping we would normally build the first units from the same process route and quote the production quantity separately.
- Can the material be changed to reduce cost or weight?
- Yes, and it is worth asking before the design is frozen. The current specification for this part is SUS304 stainless steel 0.5mm; depending on the service environment, a different grade or a lighter gauge with formed stiffening can meet the same requirement. What we would not do is change the material without re-checking the bend radii, the welding process and the coating system, because all three move with the substrate.
- What finishing options are available for this part?
- The current finish specification is Passivation. Because every finishing line runs in-house, the finish can be changed without changing supplier, and we match colour to a RAL or Pantone reference on the drawing.
- How long does production take, and what do you need from us to quote?
- Prototypes are typically 3–7 business days and production runs 7–15 days once the drawing is released and the finish is confirmed. To quote we need the drawing or CAD file (STEP, DXF, DWG, IGES or PDF), the material and finish, the quantity and the destination — and any tolerance or inspection requirement that is not already on the drawing. You get a DFM review with the quotation, not after it.
Sheet metal engineering guides
 Powder Coating vs Anodizing: How to ChoosePowder wins on colour and substrate range; anodizing wins on wear and thinness. Five rules that decide it, with the cost drivers behind each.Read More
 8 Proven Ways to Cut Sheet Metal Costs Without Sacrificing QualityFrom bend radius optimization to material nesting — eight actionable design and sourcing strategies that reduce cost while maintaining part performance.Read More