
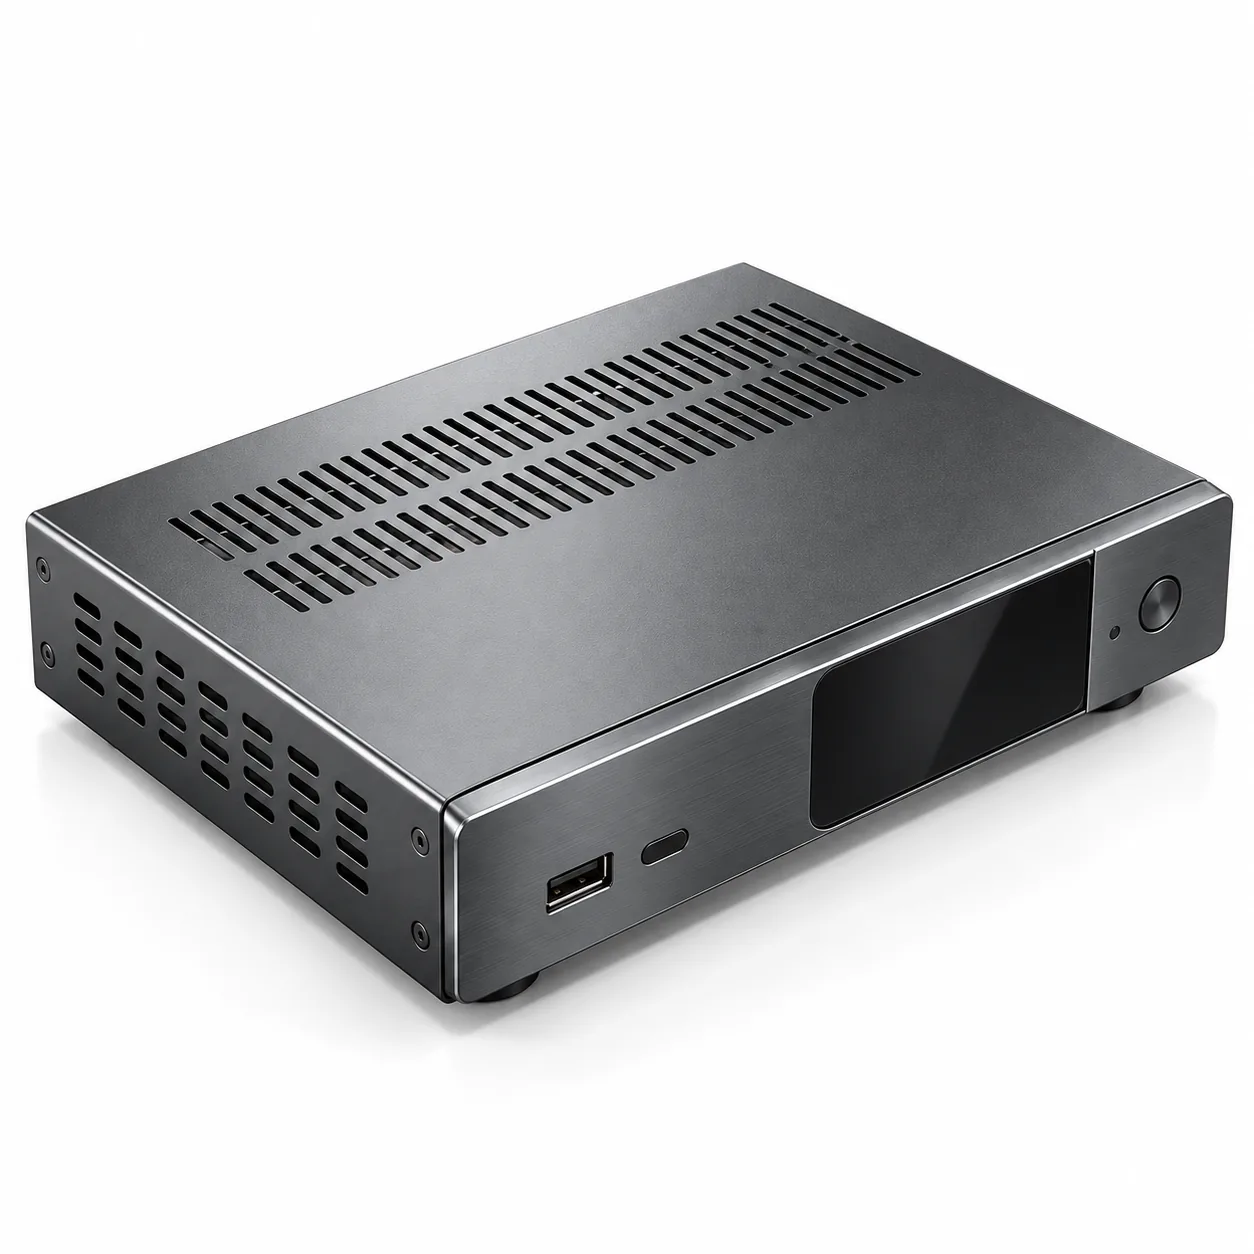
The part and its constraints
Material: SPCC cold-rolled steel at 0.8 mm, chosen for cost and for how well it takes a powder coat. Two formed halves plus a rear panel; the top face and front face are cosmetic class A, everything else is class B. Overall size roughly 220 × 180 × 45 mm.
The dimensional requirements were ordinary — ±0.2 mm on the mounting features, general tolerances elsewhere. The hard requirement was visual: no read-through of internal ribs on the cosmetic face, no twist across the diagonal, and a uniform gap where the two halves meet.
What the first sample got wrong
The first samples passed every measured dimension and still failed. Bending 0.8 mm steel over a 220 mm span produces a slight twist that no individual dimension catches, and once the two halves were fastened the cumulative twist showed as an uneven joint line.
The second issue was oil-canning. A large unsupported flat area flexes under handling pressure, and the deflection is permanent enough to be visible after coating. Adding thickness would have solved both problems and taken the part out of its cost bracket.
The DFM changes that fixed it
| Issue | Change | Effect |
|---|---|---|
| Twist across the long span | A field of short swages formed across the top face | Interrupts the bend line; twist falls inside the cosmetic tolerance |
| Oil-canning on the flat face | The same swage field, plus a small embossed logo used structurally | Removes the unsupported span without adding material |
| Uneven joint line | Register the two halves from a pierced hole pair rather than the edge | Edge condition no longer controls the gap |
| Visible tooling marks on class A face | Bend with a urethane-protected punch and specify the low-marking die | Finishing no longer has to sand out die witness marks |
Route and inspection
The route was laser cut, form, swage and emboss in a single press-brake and press sequence, then a light deburr before coating. No welding on the visible faces; the structure comes from geometry rather than joints, which is what keeps the cosmetic surface free of distortion.
Inspection focused on what actually fails: a flatness check across the cosmetic face with the part resting on a surface plate, a diagonal measurement to catch twist, and the joint gap checked with the two halves assembled rather than individually. The dimensional report measures features, but the cosmetic check is where this part is really approved.
What transfers to other parts
- On thin cosmetic panels, stiffness comes from geometry — swages, embossments, formed flanges — not from gauge.
- A part can pass every dimensional callout and still fail on twist; check the assembly, not just the part.
- Specify which faces are cosmetic and which are not. It changes the tooling and the amount of finishing work.
- Where a logo or label is required anyway, designing it as an embossment makes it carry structural work instead of being a cost.