
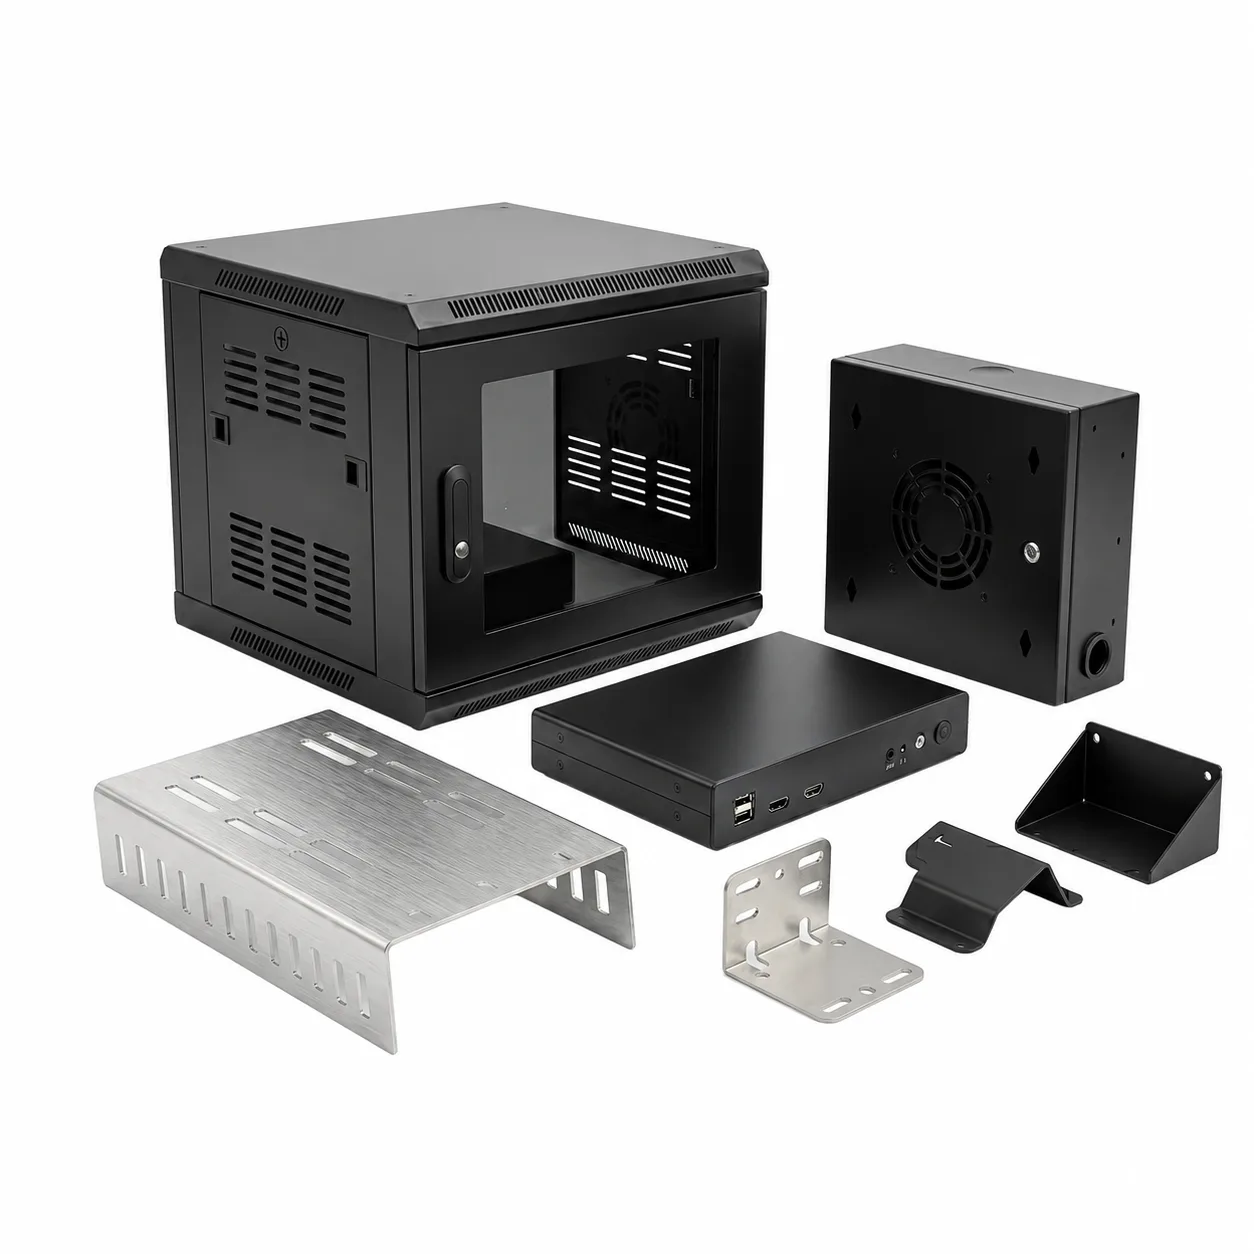
One supplier across the whole route
A custom sheet metal part passes through cutting, forming, welding, finishing, hardware and assembly before it is packed. Where those steps sit in different companies, each hand-off adds a freight move, a schedule, a tolerance conversation and a place for a defect to be discovered late.
Keeping the route in one shop does not make the work cheaper per operation. It makes the schedule shorter and the accountability single: one entity owns the part from blank to crate, including the finish and the packing.
| Step | What it needs from you | What it produces |
|---|---|---|
| DFM review | Model, drawing, quantity, function | Manufacturability notes and any suggested changes |
| Cutting | Outline, apertures, corner radii | Blank or finished profile at ±0.1 mm |
| Forming | Bend lines, radii, flange lengths, sequence | Formed part at ±0.5° on angle |
| Welding / joining | Joint type, whether structural or cosmetic, access | Welded assembly, dressed if specified |
| Finishing | Specification, colour reference, masking, which faces | Coated or plated part to the stated finish |
| Hardware / assembly | Insert part numbers, positions, press access | Assembled part, hardware seated and verified |
| Inspection | Which features matter, and what documentation | First article report and production checks |
What to send for a first enquiry
- The 3D model in STEP, plus a dimensioned 2D drawing. The model defines geometry; the drawing defines what is controlled.
- Material grade and thickness in millimetres, with any gauge reference as a cross-check only.
- Quantity now and the expected repeat rate. They change the recommended process, not just the price.
- General tolerance standard, and explicit callouts only on features that locate, seal or carry load.
- Finish, in enough detail to order it: process, thickness or film weight where applicable, and a colour reference.
- Inspection and documentation requirement — first article, material certificate, dimension report, or none.
- Any standard the part must meet, and how you verify it on receipt.
From prototype to production without changing supplier
A prototype is usually laser cut and bent, because that puts the geometry in a programme instead of a die. When volume arrives, the same part may move to stamping — and the honest question is where the break-even sits, which we will calculate with you rather than push a process.
Staying with the same supplier across the move means the flat pattern, the material, the finish and the inspection history carry across. It also means whoever validated the prototype is the same party accountable for the production part.
Where custom parts go wrong
Not usually in the making. The recurring failures are a drawing that contradicts its model, a material named in imperial and metric terms that disagree, a finish specified without masking, and a tolerance callout tighter than any process can repeat. All four are visible before a machine starts, which is why the DFM review on a new part is worth more than any amount of inspection afterwards.